bhp-ro-reverse-osmosis-system-industrial-pure-water-treatment-purification-equipment, bhp-ro-reverse-osmosis-system-industrial-pure-water-treatment-purification-equipment, /ro-system
EN
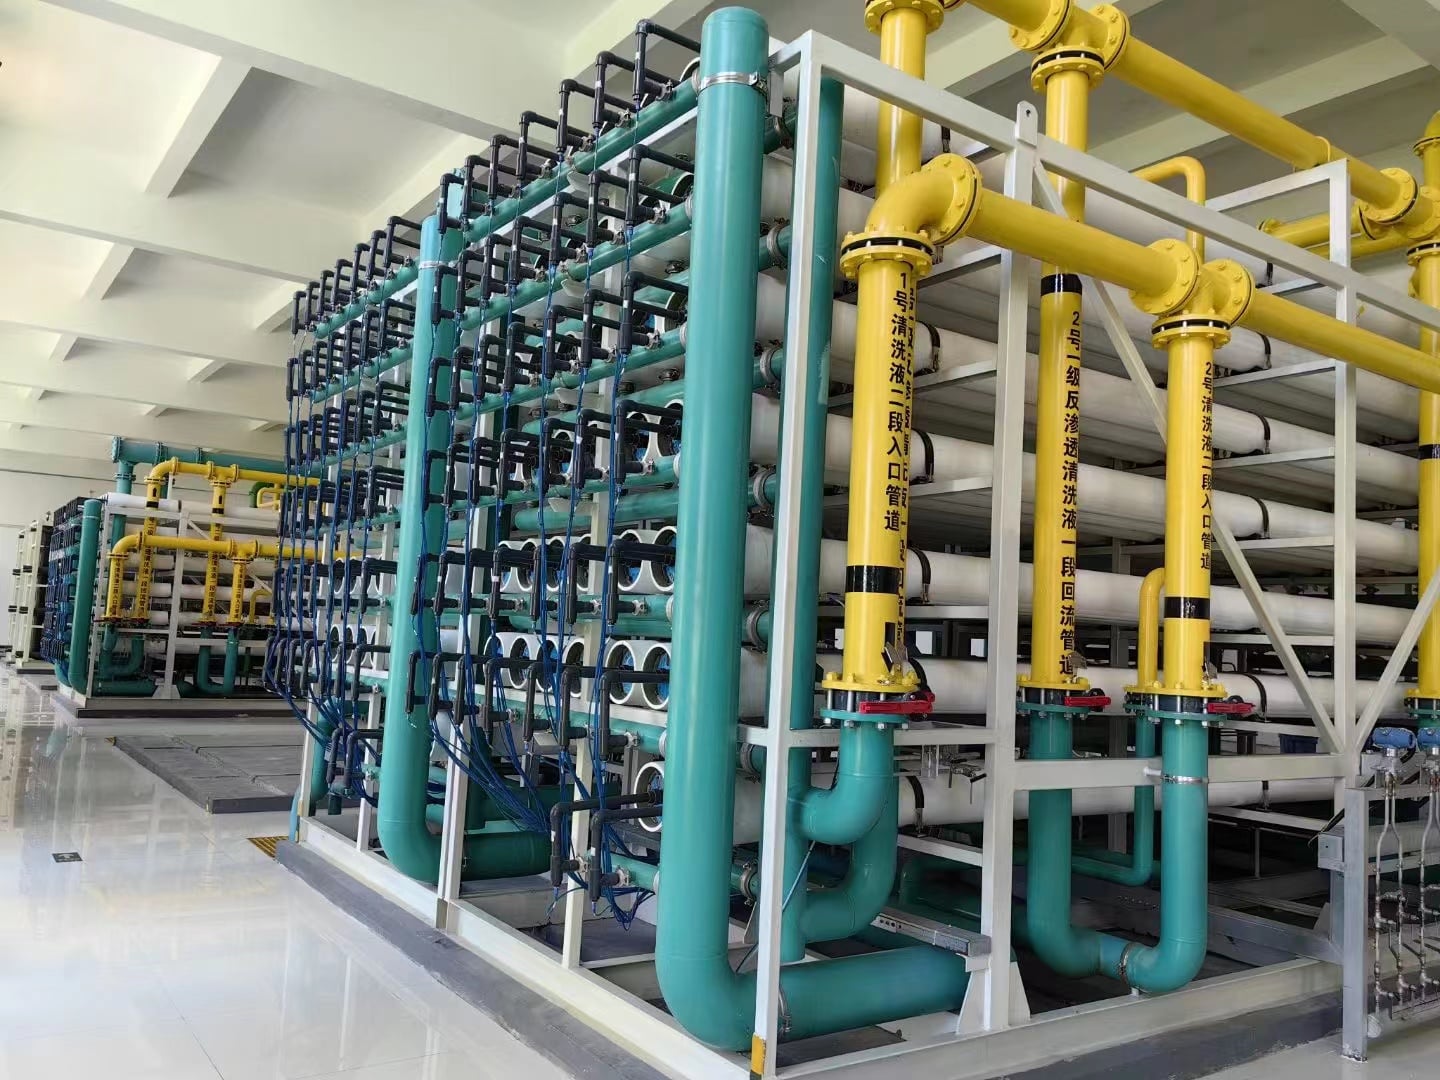
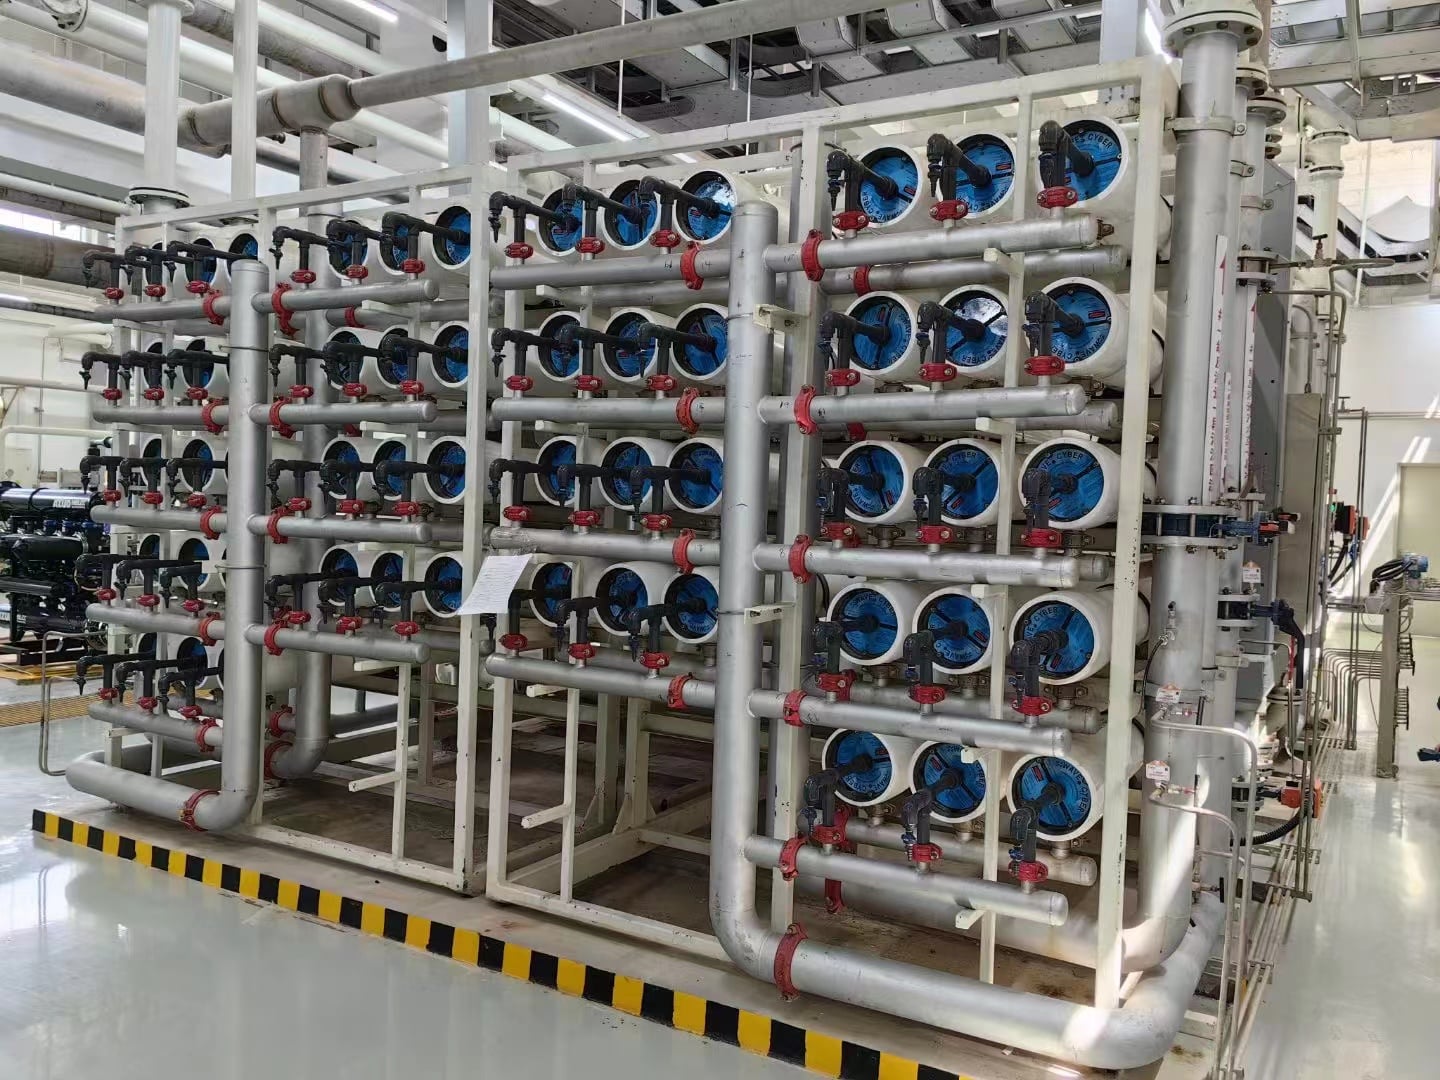
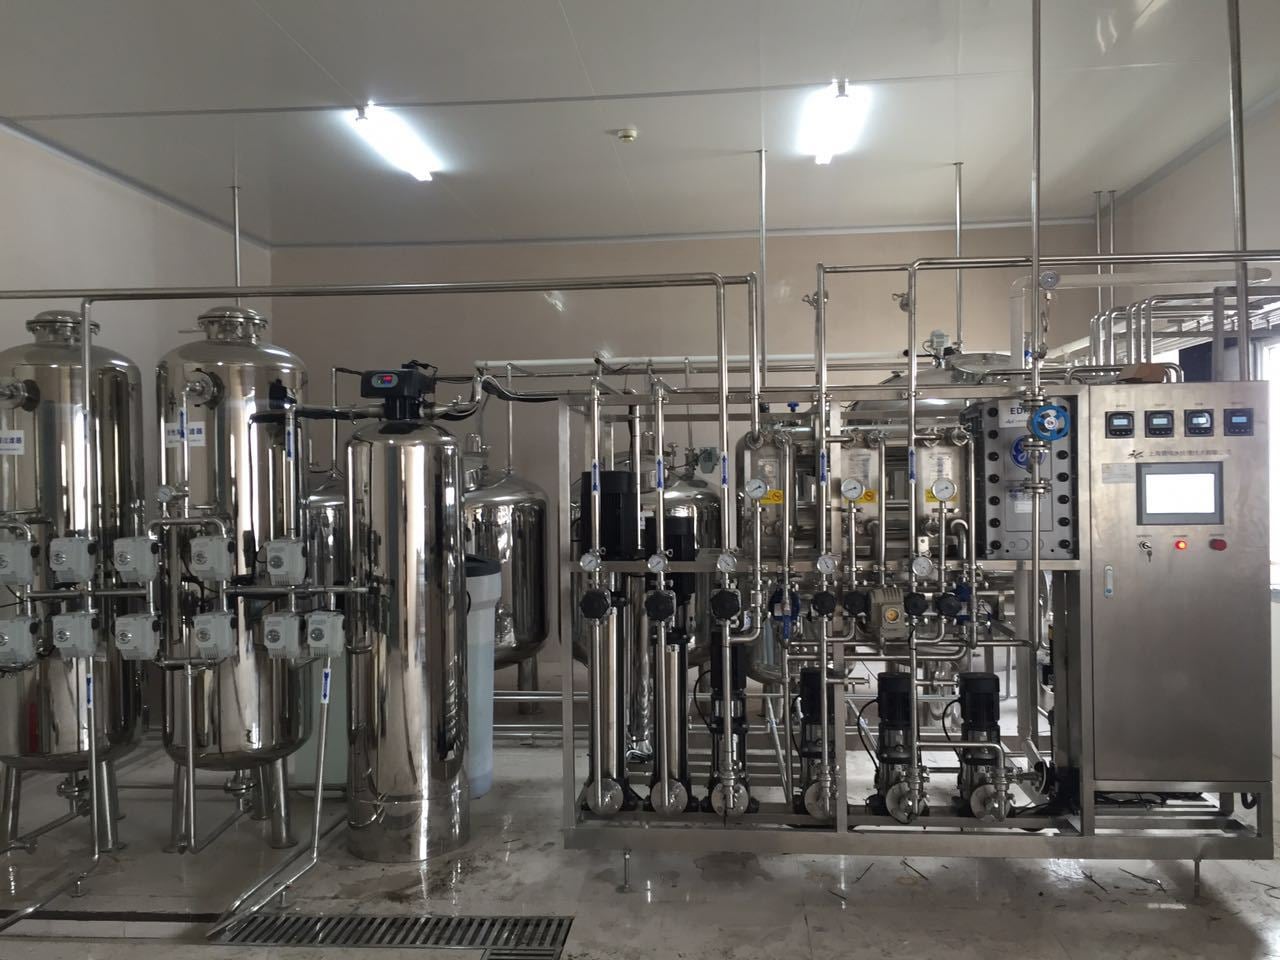
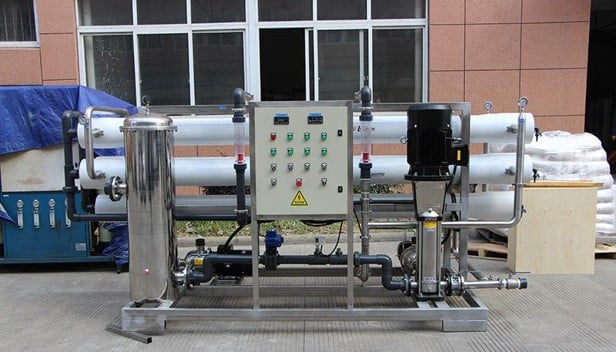
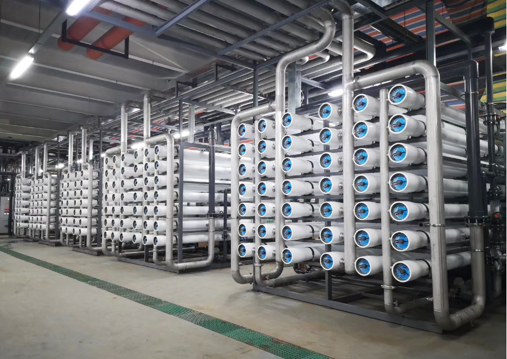
BHP industrial RO reverse osmosis system, 0.5-200T/H, ≥97% desalination, PLC-automated, corrosion-resistant, for electronics, pharma, food, and boiler feed.
| Brand | BHP |
| Model | BHP-RO Series, Custom Capacity 0.5–200T/H |
| Core Technology | Reverse Osmosis Membrane Filtration |
| Desalination Rate | ≥97% (Brand-new membrane elements) |
| Single-stage RO Water Quality | Conductivity ≤10 μS/cm |
| Double-stage RO Water Quality | Conductivity ≤2 μS/cm |
| System Water Recovery Rate | 70%–80% |
| Working Pressure | 1.0–1.6 MPa |
| Operation Mode | Full-automatic PLC intelligent control, auto flushing & fault alarm |
| Main Material | 304/316 stainless steel frame, UPVC / sanitary stainless steel pipeline |
| Inlet Water Requirement | Pretreated water, TDS ≤1000mg/L |
| Working Temperature | 5℃–45℃ |
| Certification | ISO9001, ISO14001, CE Export Certified |
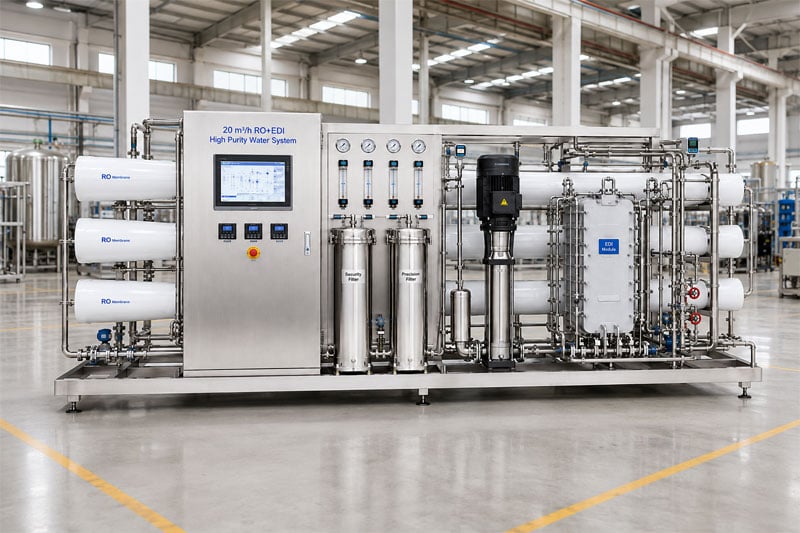
The BHP RO reverse osmosis system supports flexible configuration options including two-pass double-stage RO, EDI ultrapure modules, online TDS and conductivity monitoring, cloud-based remote monitoring systems, automatic CIP cleaning systems, and concentrated water recovery units to meet diverse industrial water-quality requirements. These options ensure that the pure water treatment system can be precisely tailored to specific industrial applications.
The BHP RO reverse osmosis system is a professional-grade industrial water purification equipment solution engineered to remove dissolved salts, heavy metals, colloids, bacteria, and organic impurities through high-precision RO membrane technology. Combining superior desalination efficiency, fully automated operation, and energy-conscious design, this pure water treatment system serves as the core unit for industrial pure water preparation and reclaimed water recycling across manufacturing, food processing, pharmaceutical, and utility sectors. As a comprehensive industrial RO filtration solution, the BHP-RO Series delivers consistent, high-quality product water for the most demanding industrial applications.
The BHP RO reverse osmosis system represents a mature, standardized industrial water purification equipment platform deployed globally in challenging water purification applications. At its core, the pure water treatment system employs premium RO membrane elements with a 0.0001 micron filtration rating that effectively rejects nearly all inorganic salts, heavy metal ions, suspended solids, microorganisms, and high-molecular-weight organic contaminants present in pretreated feed water, delivering consistent product-water quality suitable for demanding industrial processes. This industrial RO filtration technology ensures reliable performance across thousands of operating hours.
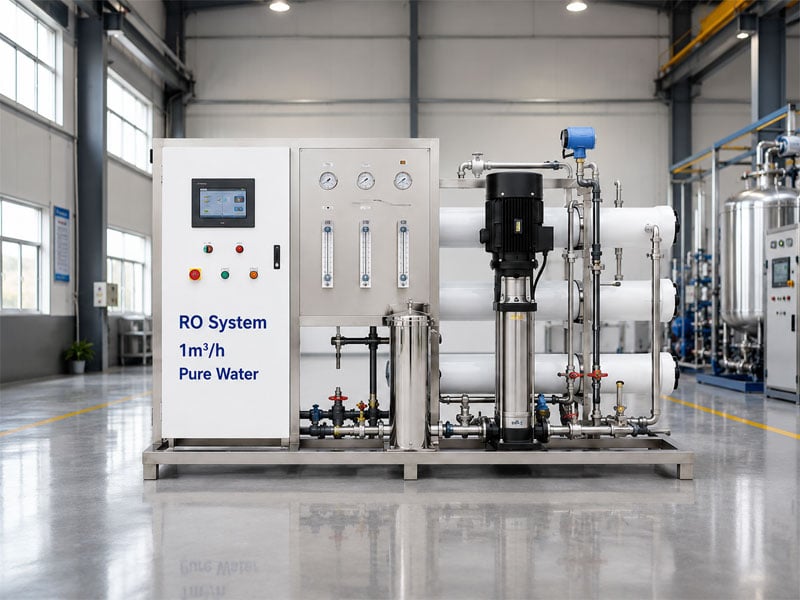
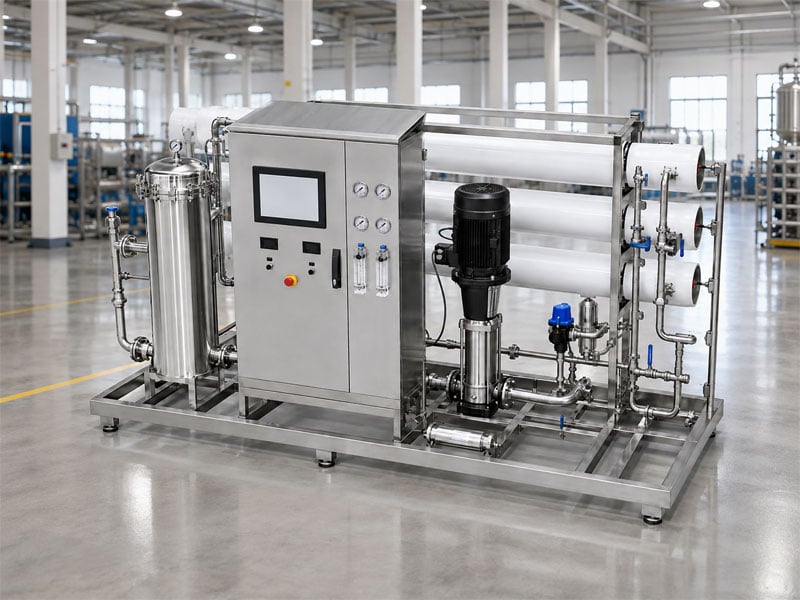
The complete RO reverse osmosis system features a compact, modular skid-mounted design with a minimal physical footprint ideal for space-constrained facilities. An integrated intelligent PLC control system automates the entire water production and membrane management workflow—including real-time water-quality monitoring, scheduled membrane flushing, and automatic fault protection—enabling reliable 24-hour unattended operation. Available in single-stage and two-pass (double-stage) RO configurations, the pure water treatment system flexibly addresses varying water-purity requirements from standard industrial pure water to high-purity process water. When paired with comprehensive pretreatment and advanced EDI modules, the industrial RO filtration system achieves laboratory-grade ultrapure water with resistivity up to 18.2 MΩ·cm for the most demanding pharmaceutical, electronics, and research applications.
1. High Salt-Rejection Performance
The industrial RO filtration system employs internationally recognized RO membrane elements to achieve a consistent salt-rejection rate exceeding 97%, delivering reliably low water conductivity and long-term product-water quality stability across thousands of operating hours. This performance makes the RO reverse osmosis system the preferred choice for industrial water purification equipment applications.
2. Intelligent Full-Automatic Operation
Integrated intelligent PLC control system performs automatic start/stop sequencing, scheduled membrane flushing, and abnormal-pressure protection, substantially reducing manual oversight and minimizing operational maintenance costs. The pure water treatment system is designed for continuous unattended operation, lowering labor requirements and human error.
3. Energy Efficiency and High Water Utilization
Optimized piping and hydraulic design achieve system water recovery rates reaching 80%, while energy-efficient high-pressure pump technology reduces power consumption and supports economical long-term continuous operation. The industrial RO filtration system delivers cost-effective water purification with optimized resource utilization.
4. Durable & Corrosion-Resistant Construction
Key system components utilize stainless steel and food-grade, corrosion-resistant materials engineered to withstand rust, chemical attack, and aggressive service environments, ensuring durability for demanding industrial applications and extended operational lifespan. The RO reverse osmosis system is built for long-term reliability in harsh industrial environments.
5. Flexible Customization
Available in customized flow rates ranging from small 0.5t/h commercial units to large 200t/h industrial systems, with single-stage or two-pass RO configurations tailored to different industrial and feedwater conditions. The pure water treatment system can be precisely scaled to match specific flow and quality requirements.
6. International Standards and Export Certification
The industrial water purification equipment complies with established international industrial manufacturing standards and carries ISO9001, ISO14001, and CE certifications. Complete professional technical documentation in English and dedicated worldwide after-sales support are provided for overseas projects and turnkey installations.
1. Electronic & Semiconductor Industry
Supplies ultrapure process water for silicon-chip fabrication, PCB production, and precision electronic-component cleaning, supporting stringent quality requirements of advanced manufacturing. The industrial RO filtration system delivers the water purity essential for high-tech electronics production.
2. Food & Beverage Processing
Produces purified water meeting food-grade hygiene standards for bottled water production, dairy processing, beverage formulation, wine brewing, and food ingredient preparation. The RO reverse osmosis system ensures consistent product water quality for sensitive food and beverage applications.
3. Pharmaceutical & Cosmetic Industry
Delivers purified water compliant with pharmaceutical preparation standards, cosmetic batching requirements, and medical-equipment sterilization and cleaning applications. The pure water treatment system meets the stringent water quality standards of regulated industries.
4. New Energy & Electroplating Industry
Provides ultrapure water for lithium-battery production, photovoltaic cell processing, and electroplating pretreatment, preventing product defects and yield loss from waterborne contamination. The industrial water purification equipment supports precision manufacturing with consistent, high-purity water.
5. Boiler & Thermal Power Industry
Generates high-quality boiler make-up water with reduced salinity, preventing internal piping scale formation and corrosion while extending boiler service life and operational efficiency. The industrial RO filtration system delivers the low-conductivity water essential for power generation applications.
6. Industrial Water Reuse Project
Enables advanced treatment and reuse of reclaimed water, reducing total plant water consumption and supporting corporate energy conservation and environmental discharge-reduction objectives. The RO reverse osmosis system is a key component of comprehensive water recycling strategies.
7. Park Centralized Water Supply
Delivers reliable standardized and process water supply for industrial zones, manufacturing facilities, and public utility infrastructure requiring consistent water-quality performance. The pure water treatment system provides centralized water purification for multi-user industrial parks.
The BHP RO reverse osmosis system integrates seamlessly with a comprehensive ecosystem of complementary treatment technologies—including multimedia sand filters, activated-carbon cartridge filters, ultrafiltration (UF) systems, and EDI ultrapure-water modules—enabling complete, integrated pretreatment and high-purity water production solutions from a single trusted source. From industrial water purification equipment to advanced industrial RO filtration, BHP delivers complete pure water treatment system solutions for diverse industrial applications and water quality requirements.
BHP industrial RO reverse osmosis system, 0.5-200T/H, ≥97% desalination, PLC-automated, corrosion-resistant, for electronics, pharma, food, and boiler feed.

 EN