bhp-industrial-ro-pure-water-system--centralized-purified-water-equipment-for-factory, bhp-industrial-ro-pure-water-system--centralized-purified-water-equipment-for-factory, /centralized-water-supply-system
EN
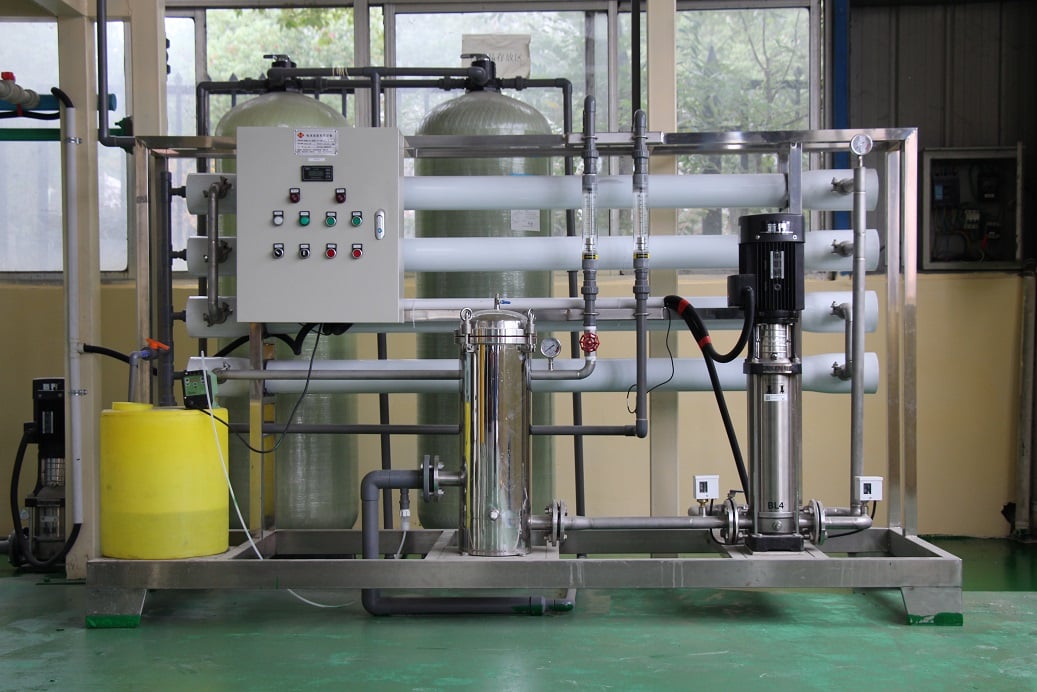
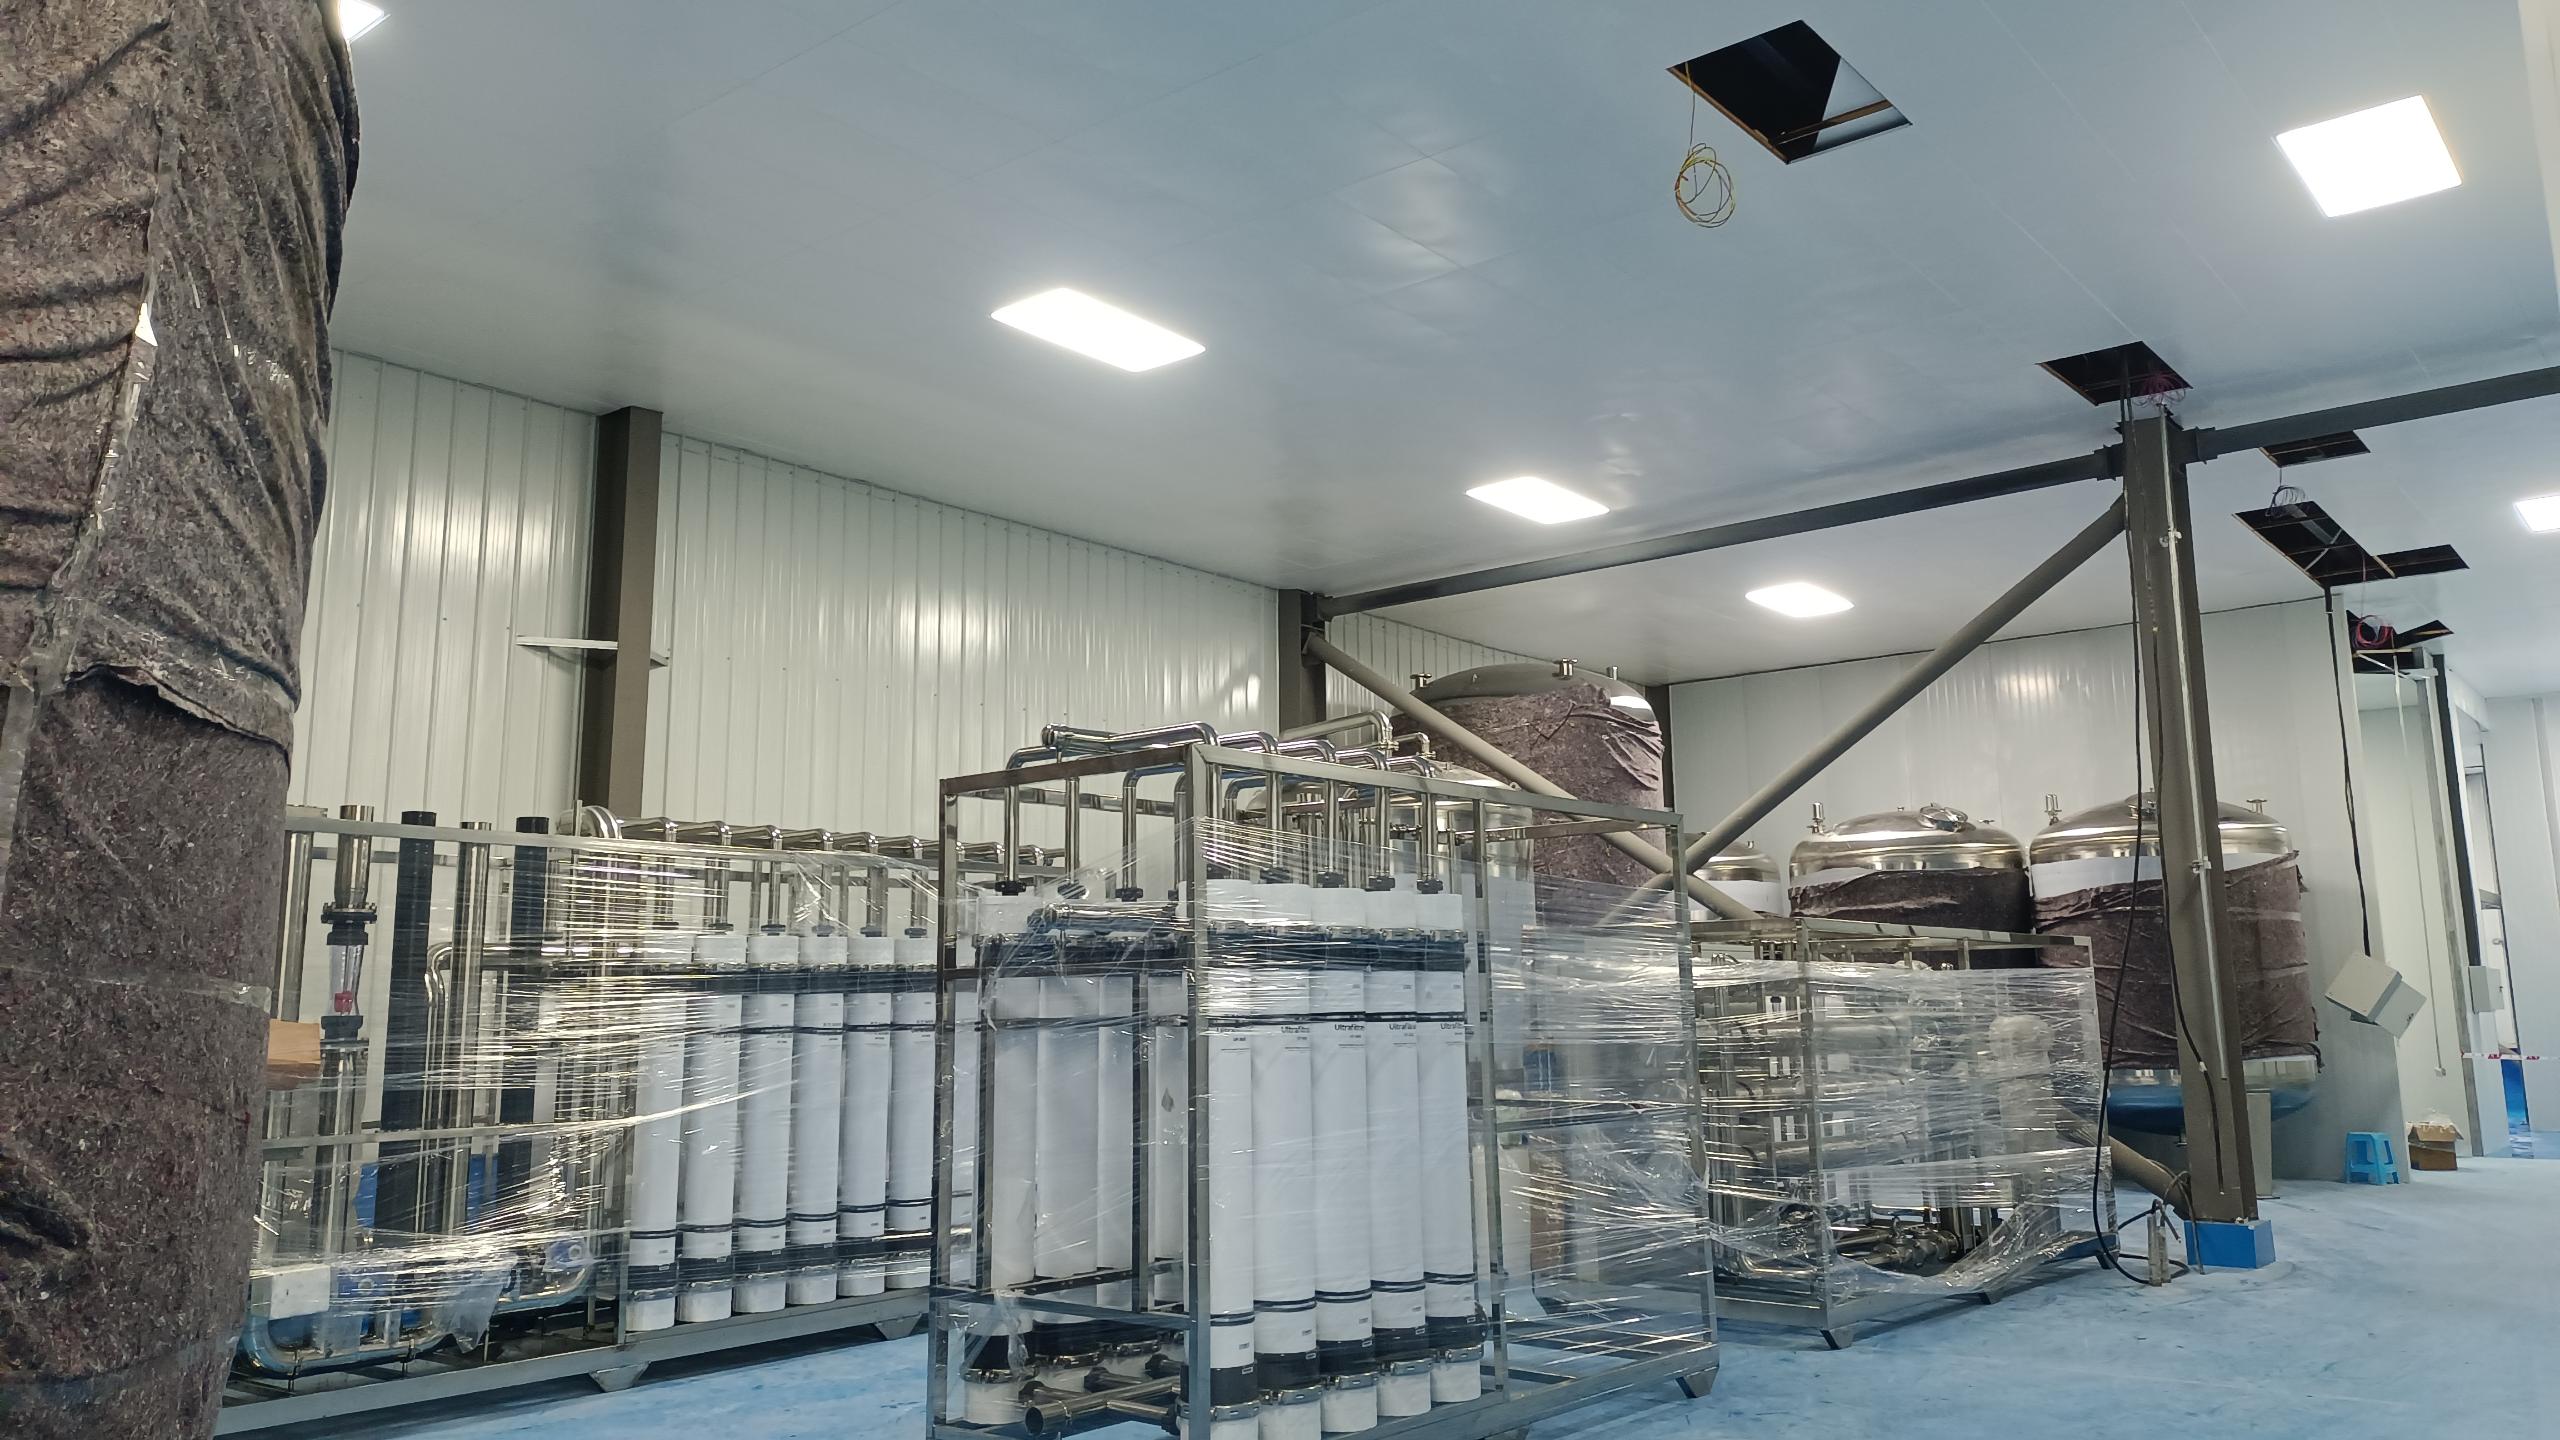
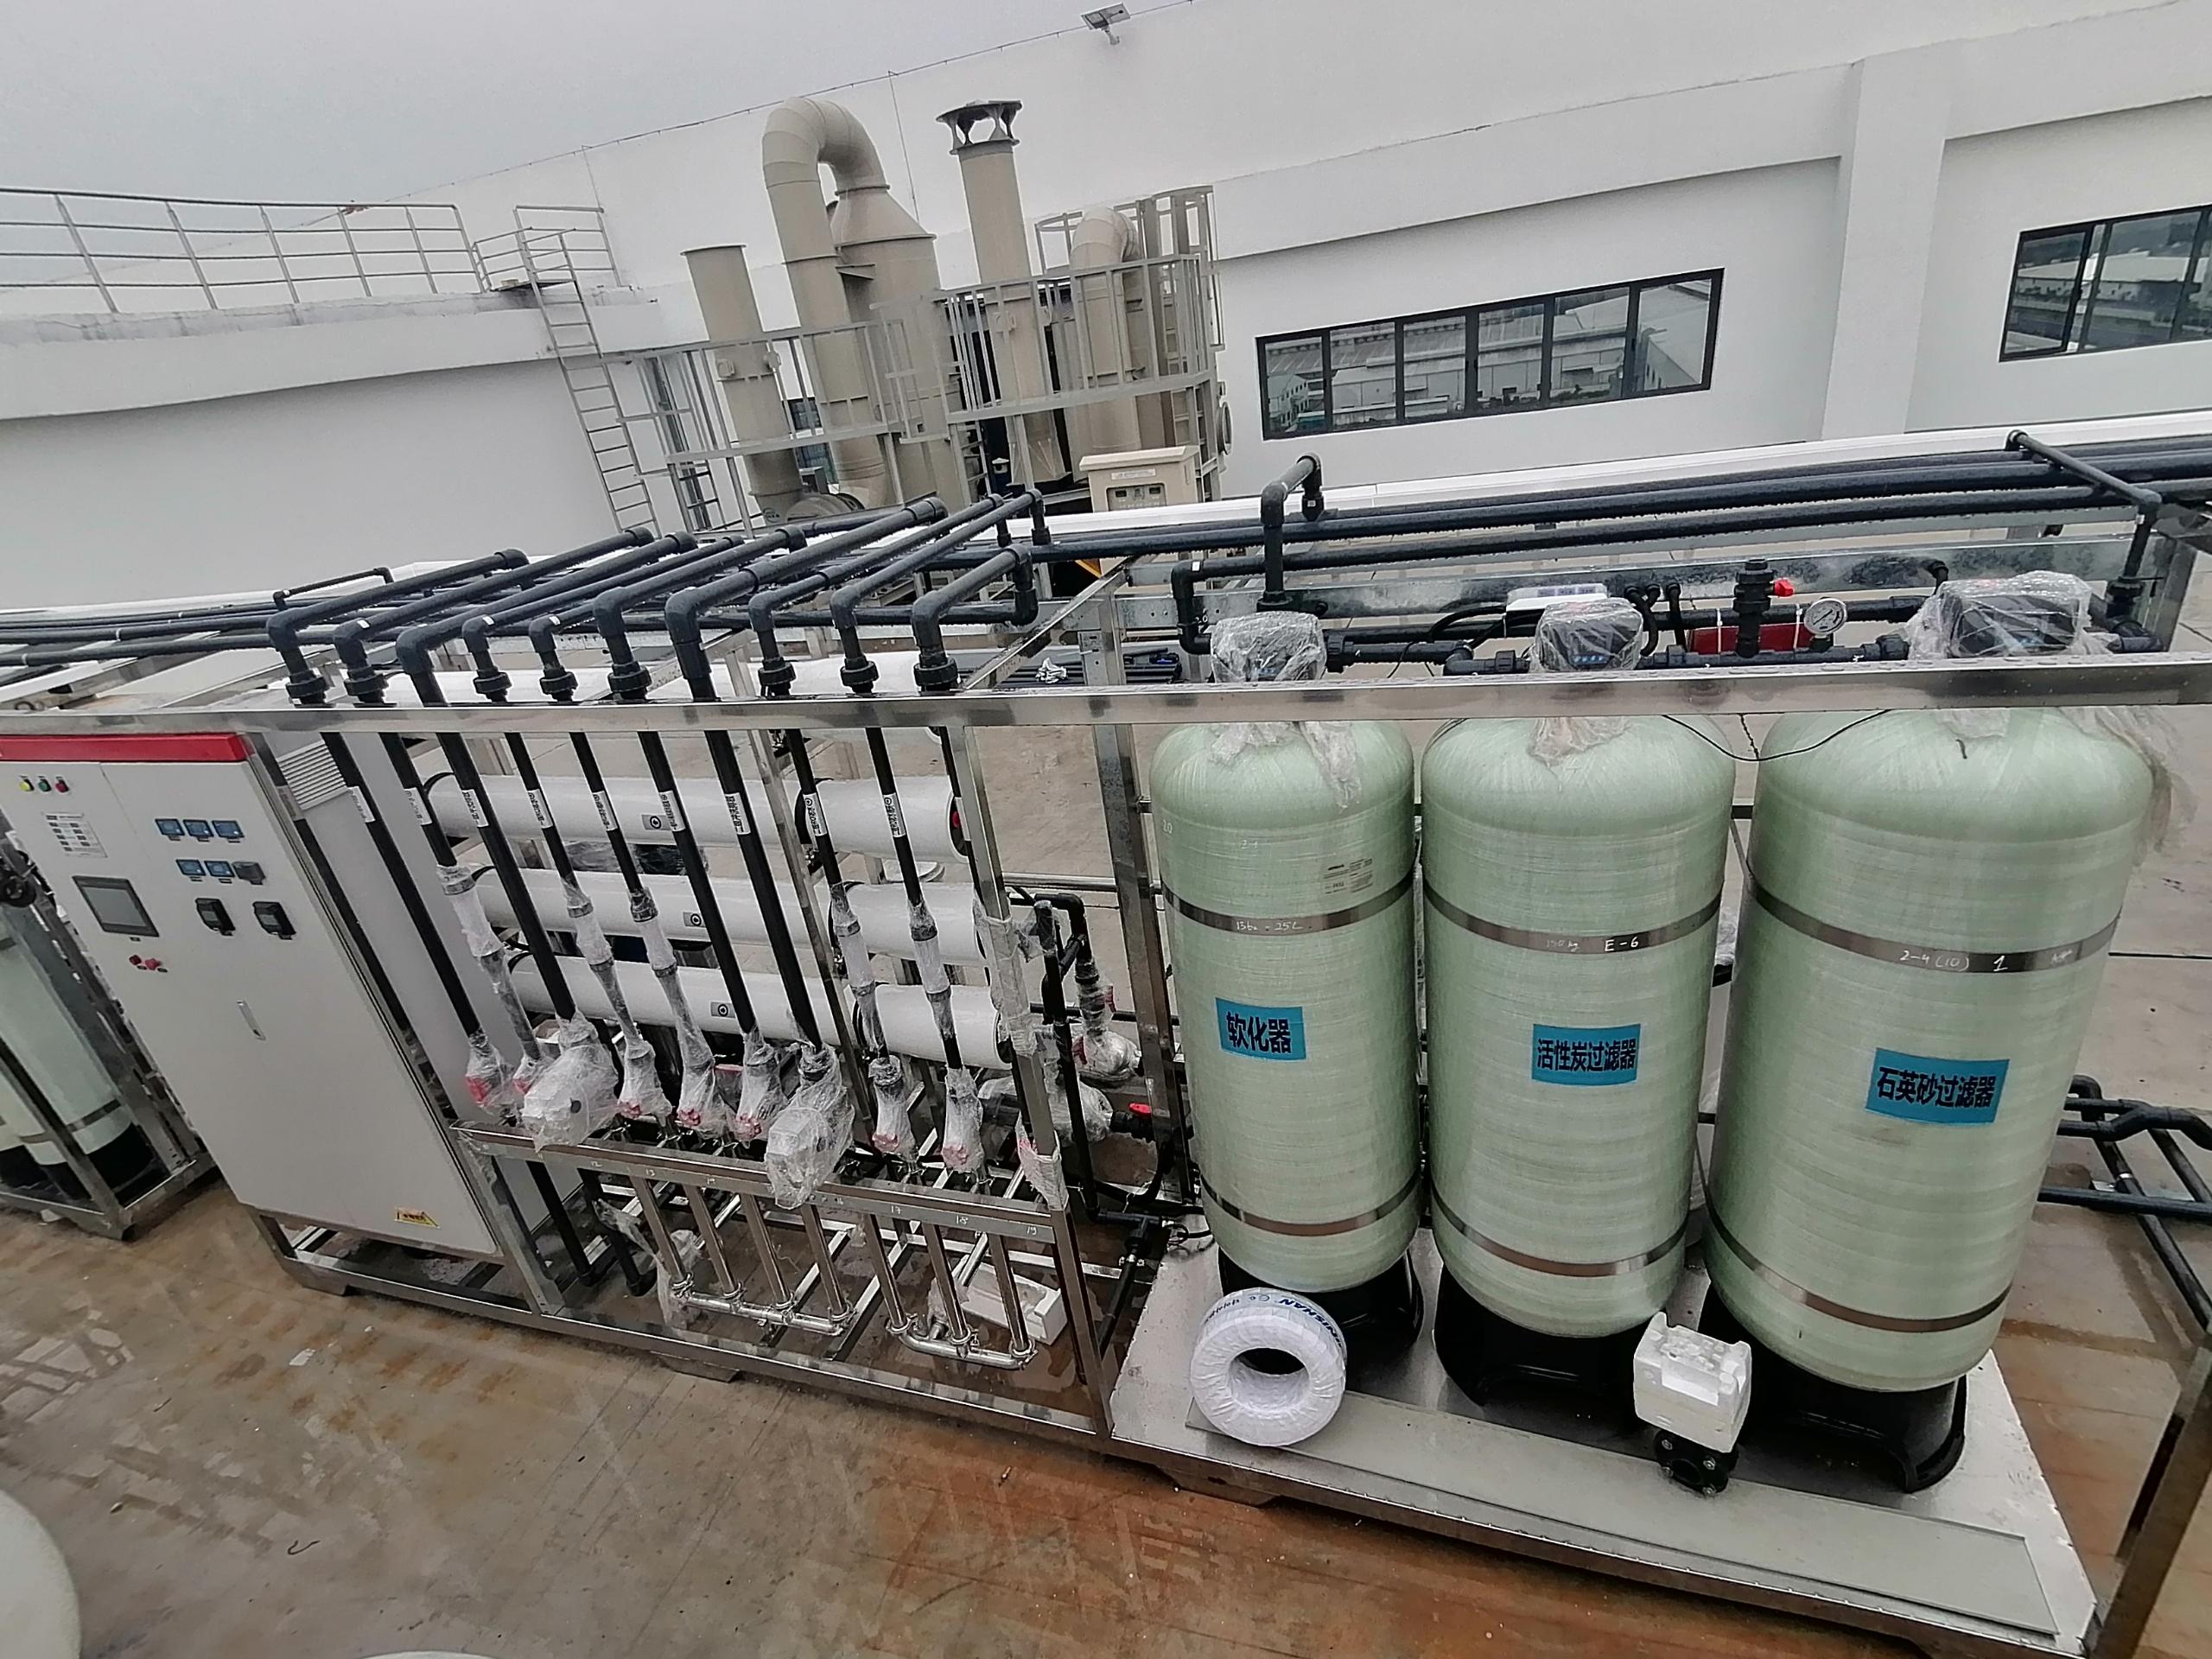
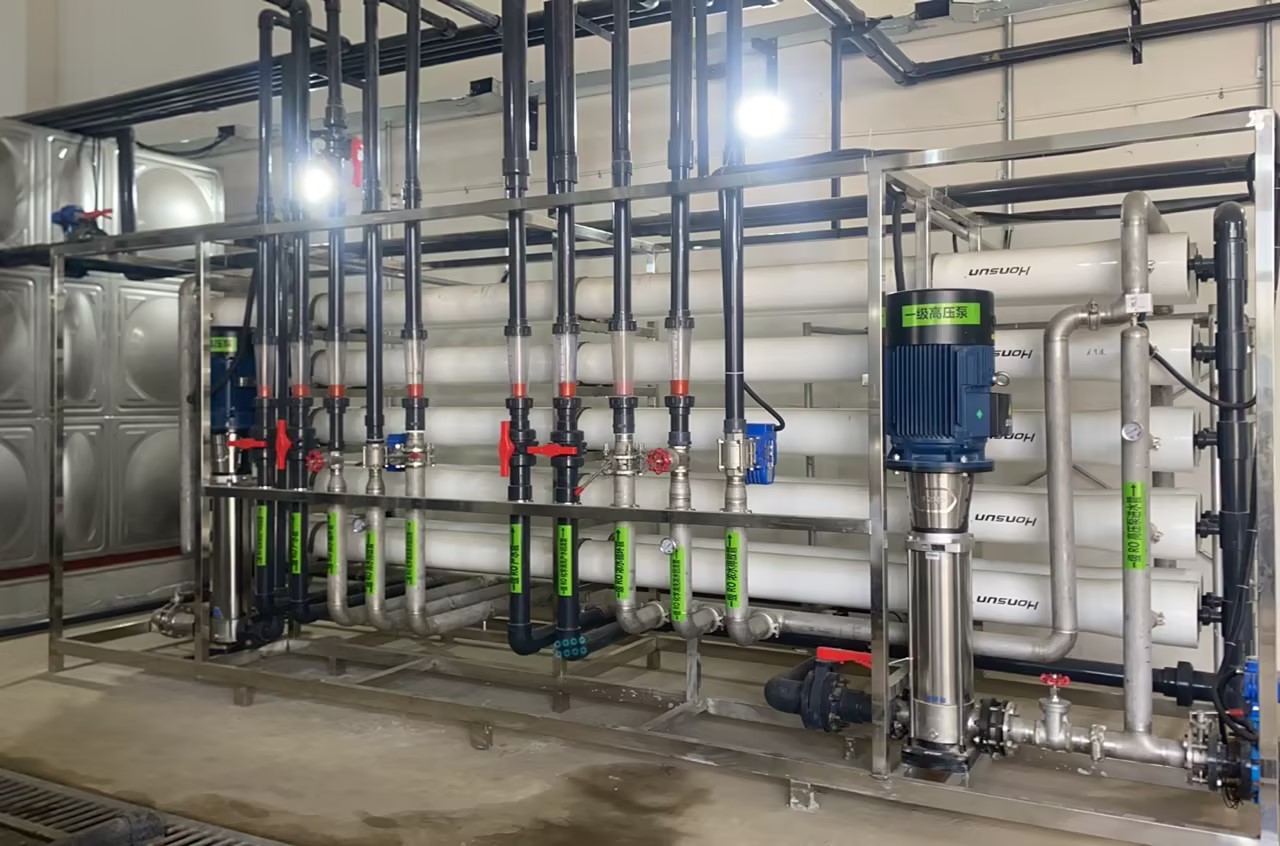
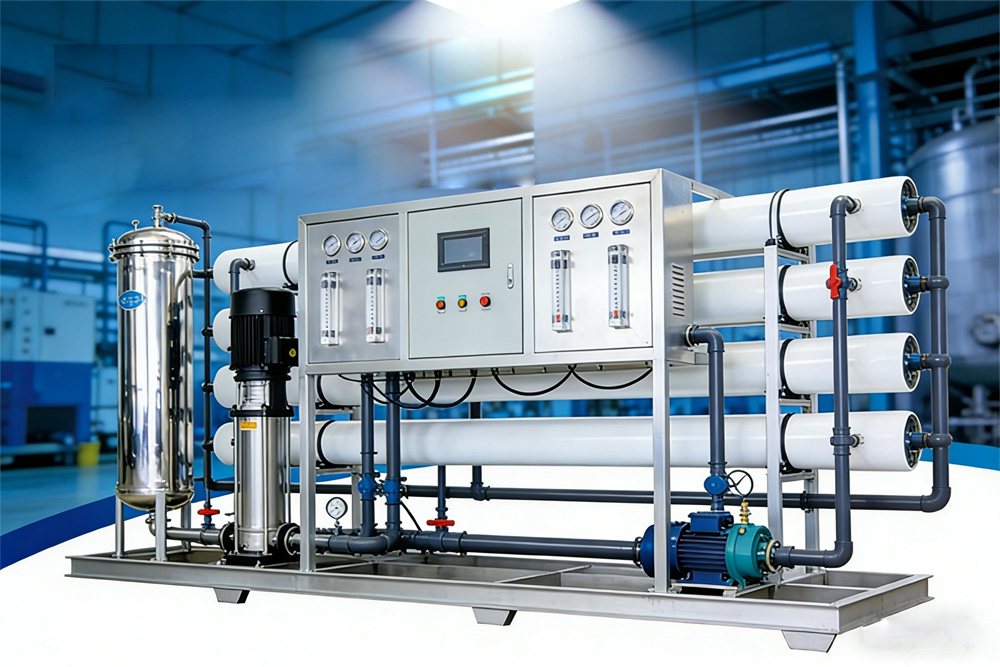
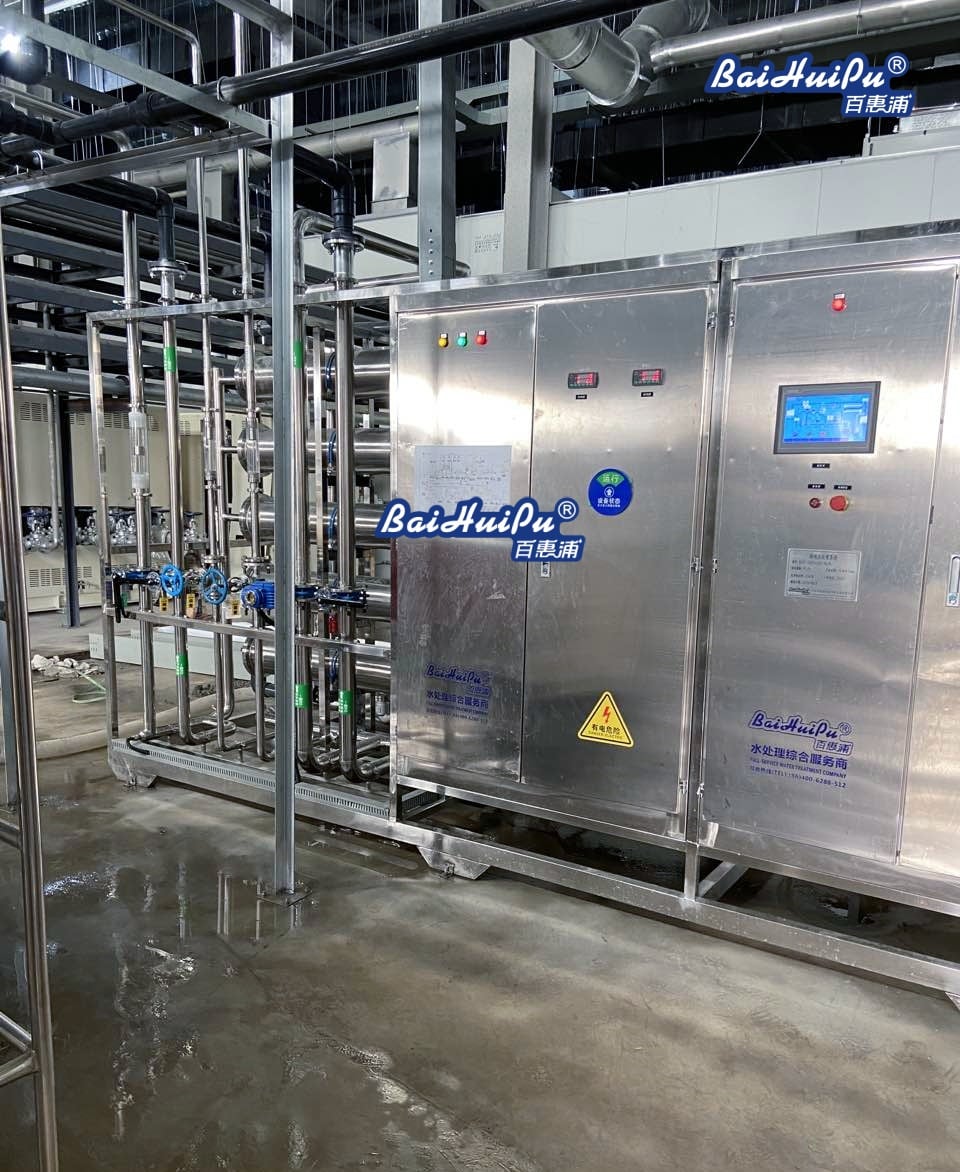
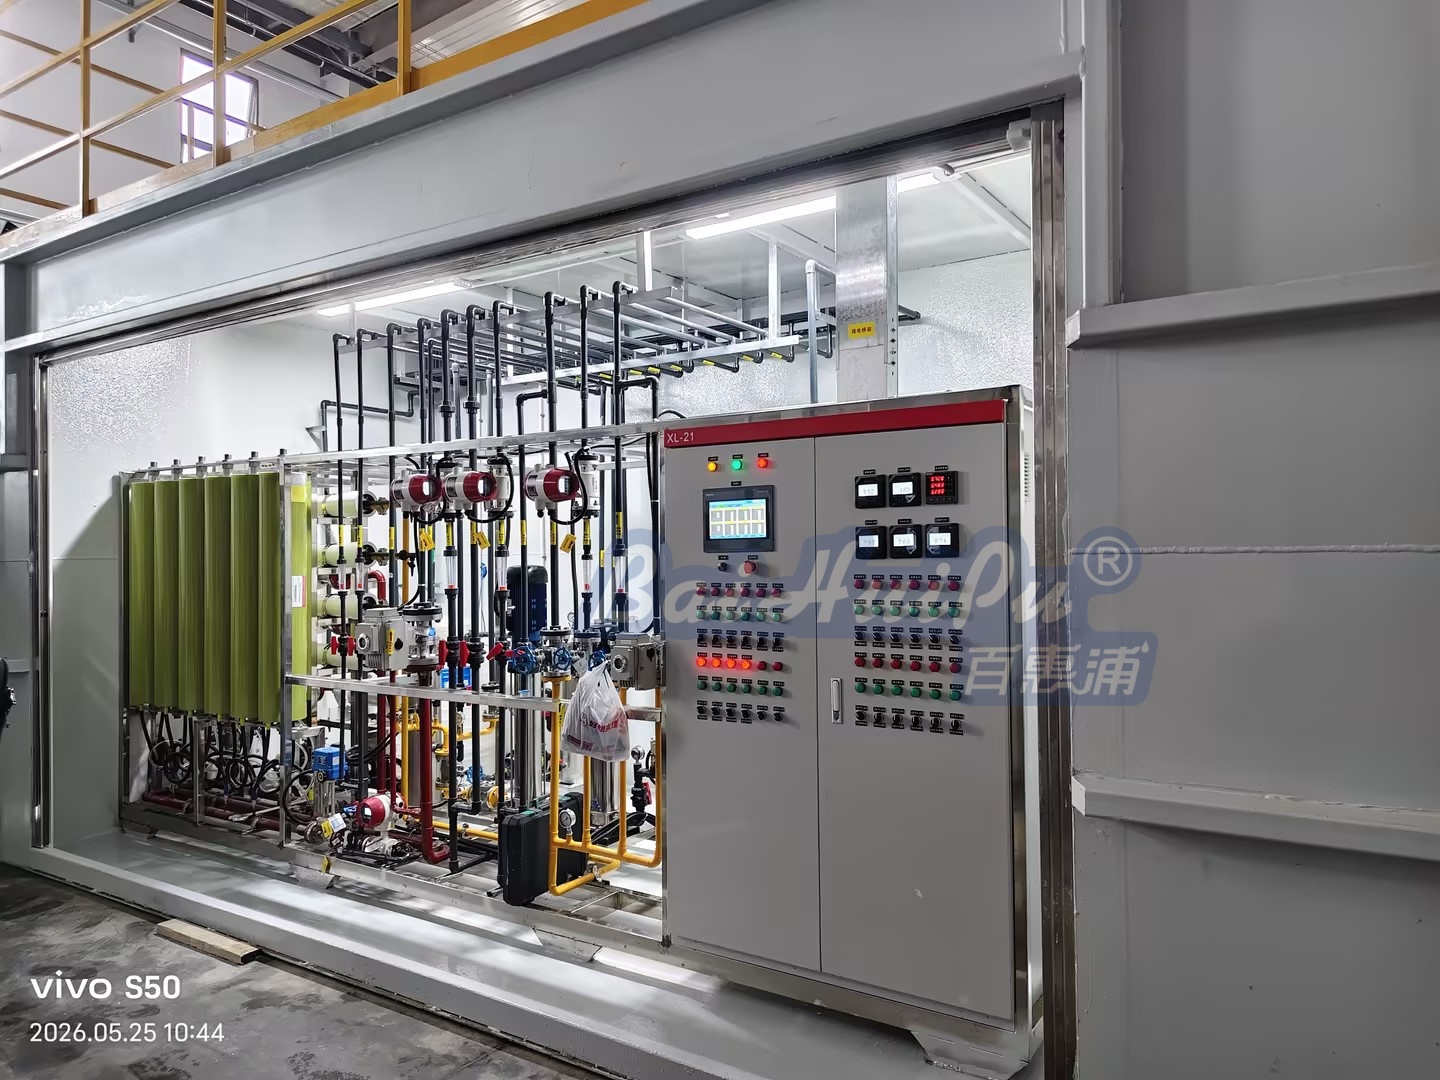
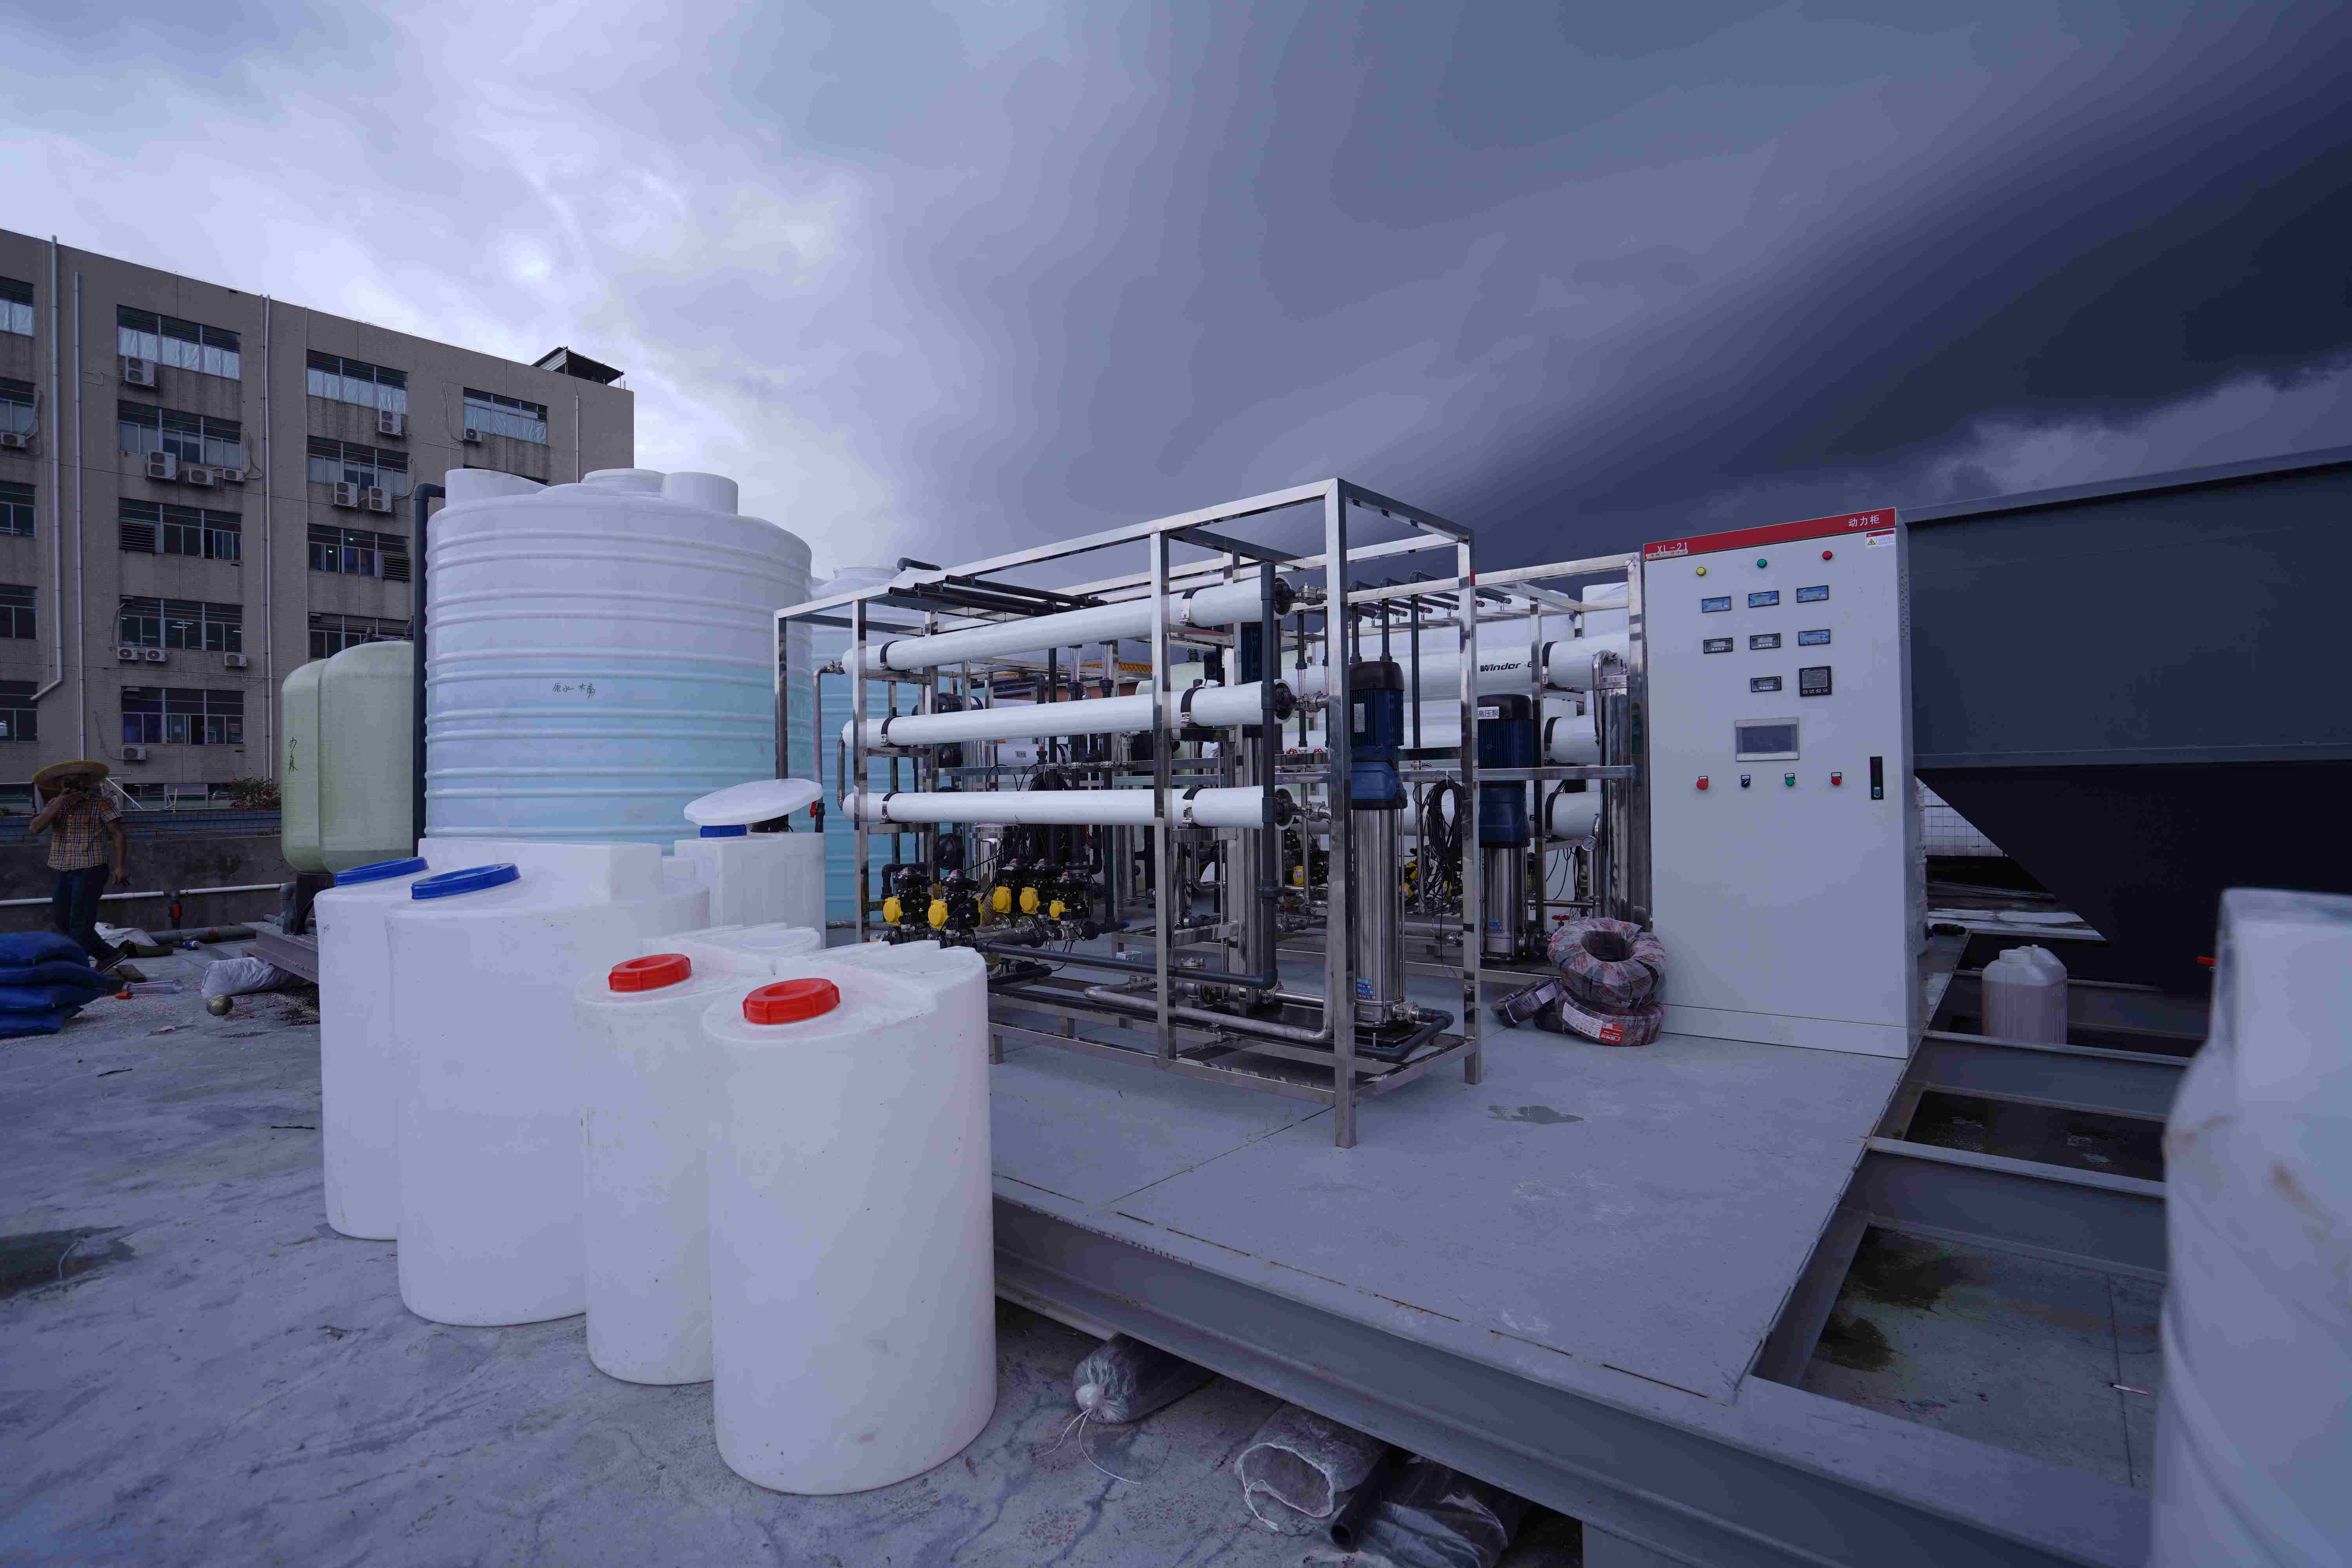
BHP industrial RO pure water system, 0.5-100T/H, 18.2 MΩ·cm resistivity with EDI, PLC-controlled, for electronics, pharma, and food industries.
| Brand | BHP |
| Model | BHP-RO Series, Custom capacity from 0.5T/H to 100T/H |
| Single-Stage RO Effluent | Conductivity ≤ 10 μS/cm |
| Double-Stage RO + EDI Effluent | Maximum Resistivity 18.2 MΩ·cm at 25℃ |
| Membrane Desalination Rate | ≥97% for Brand-New RO Membrane Elements |
| System Water Recovery Rate | 70%–80%, Concentrated Water Compatible with Reclaimed Water Reuse Circulation |
| Main Materials | Frame & Water Tank 304/316 Stainless Steel; Pipeline UPVC / Sanitary Stainless Steel |
| Control Mode | Full-Automatic PLC System with Real-Time Online Monitoring of TDS, Conductivity and Resistivity, Automatic Fault Alarm |
| Power Supply | 380V 3-phase industrial power, 50/60Hz, compatible with global power grids |
| Raw Water Inlet Condition | Tap Water / Underground Water, Inlet TDS ≤ 1000 mg/L |
| Certifications | ISO9001, ISO14001, Full CE Export Certification |
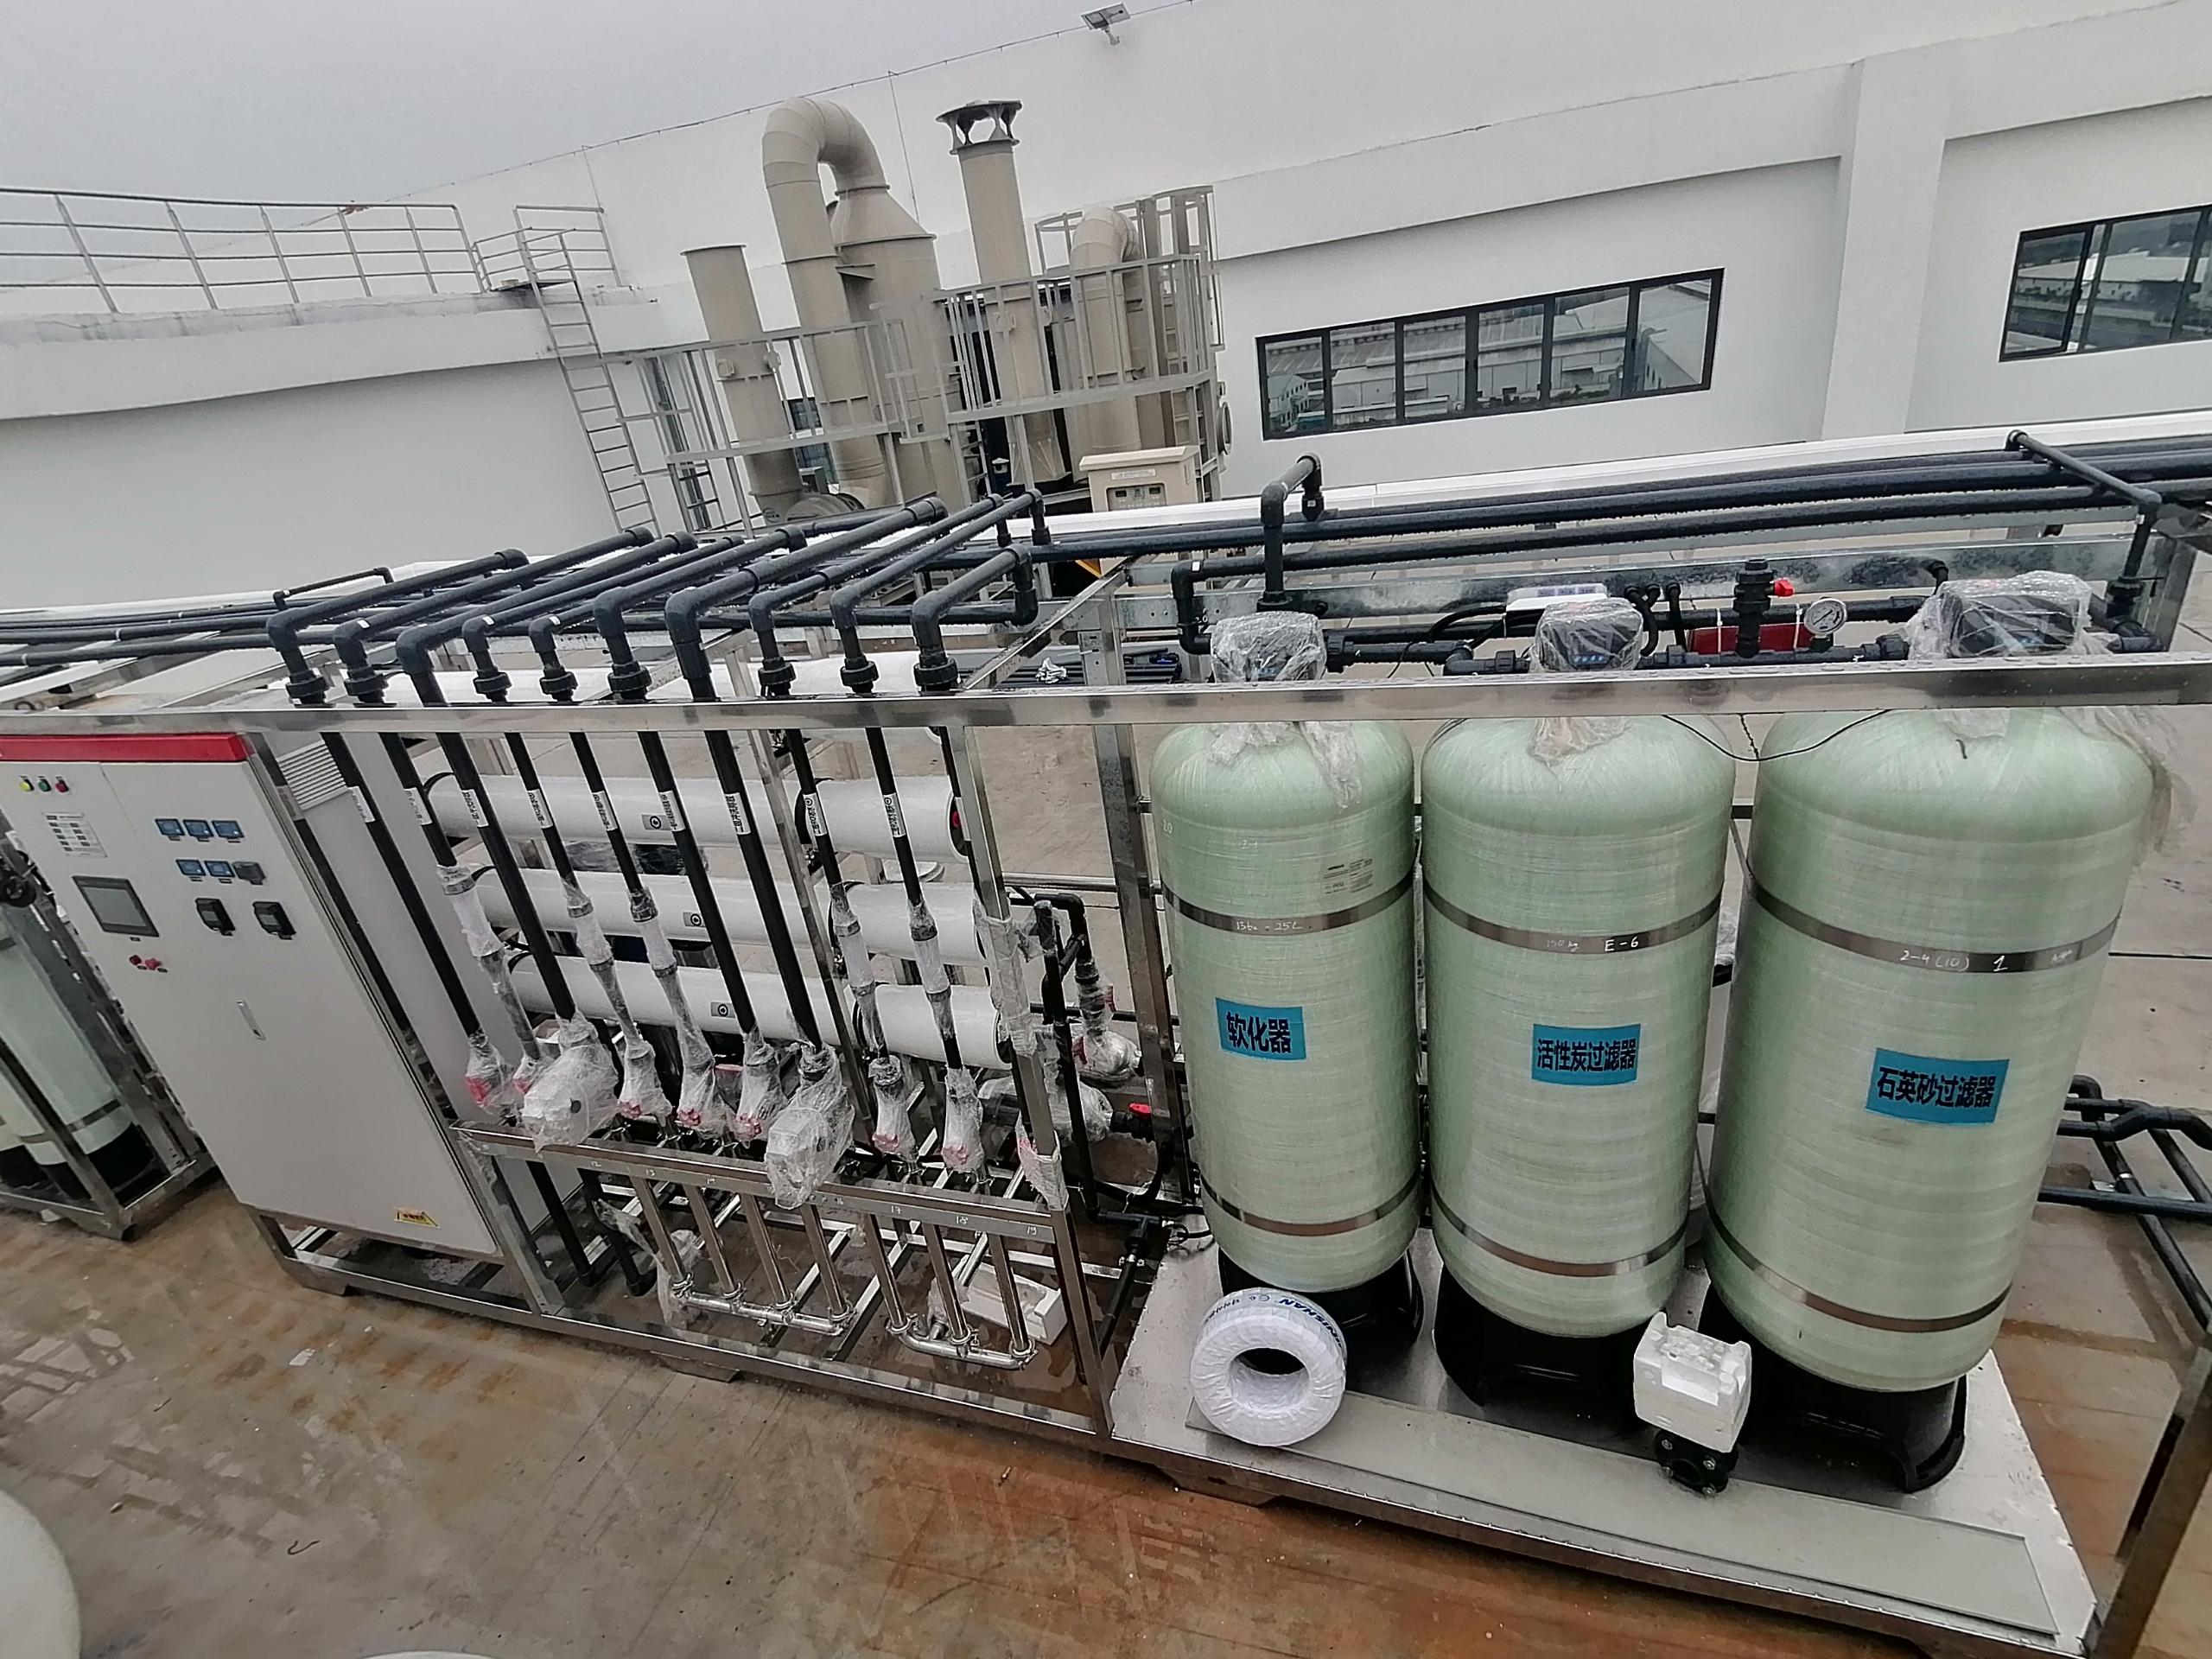
Pre-Treatment: Multimedia Filter, Activated Carbon Filter, Security Filter
Post-Treatment: EDI Ultrapure Module, UV Sterilizer, Constant Pressure Water Supply Tank
Additional Options: Cloud-Based Remote Monitoring, Automatic CIP System, Concentrate Recovery Unit
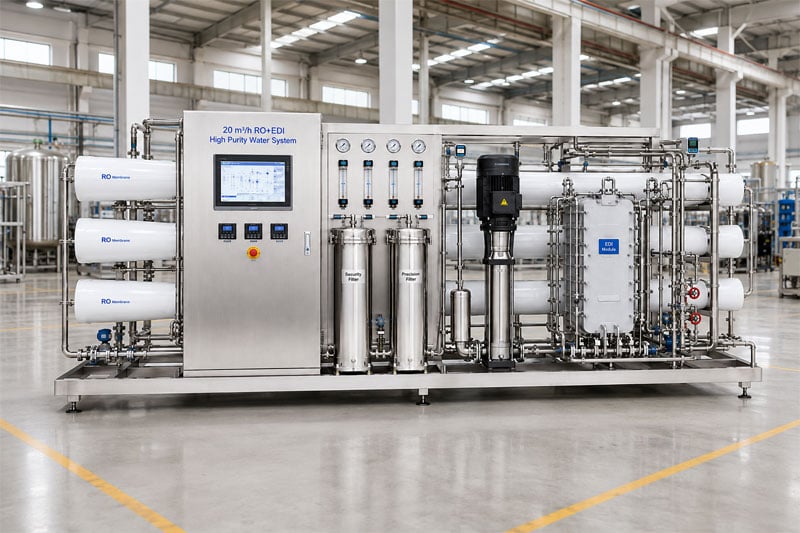
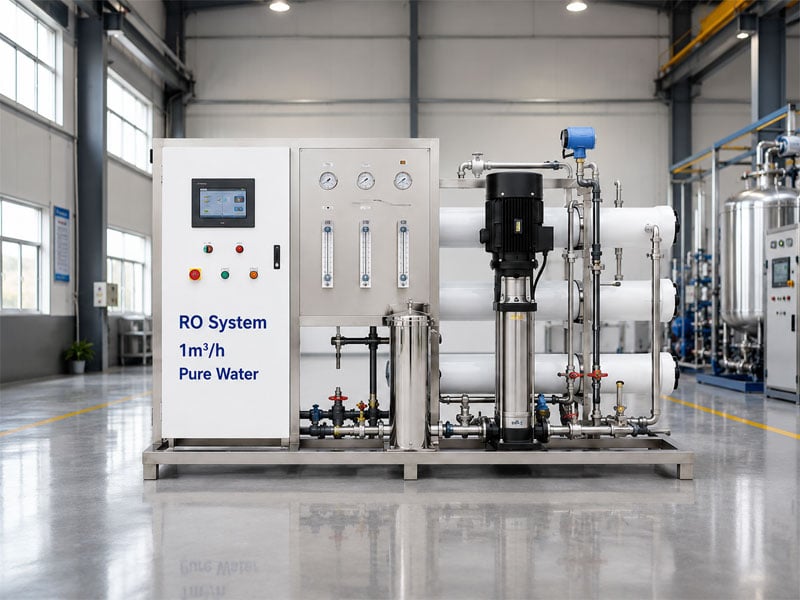
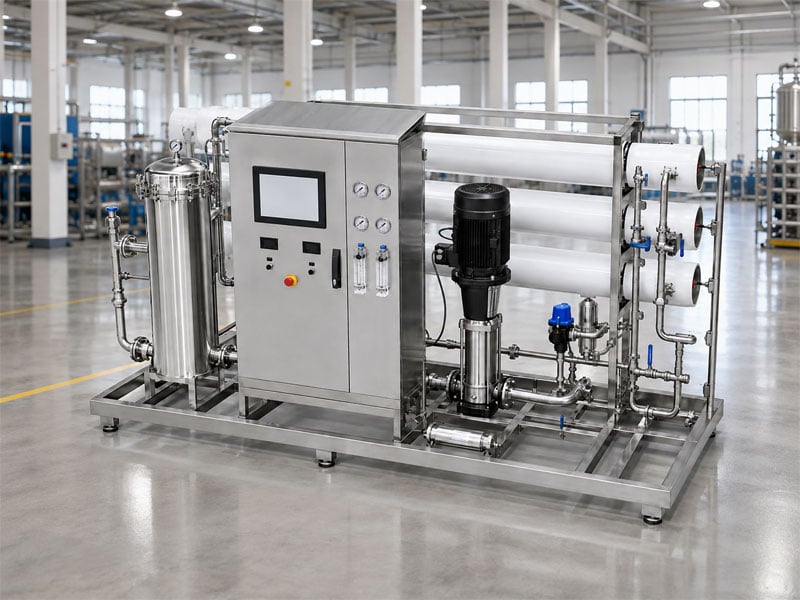
The BHP industrial RO pure water system uses reverse osmosis technology to efficiently remove salt, heavy metals, suspended solids, and microorganisms from raw water, producing qualified industrial purified water for factory operations. When equipped with an EDI module, it generates high-standard ultrapure water reaching 18.2 MΩ·cm resistivity. Designed as a centralized purified-water equipment solution, it supports factory water supply systems and integrates seamlessly with water reuse circuits for circular water utilization. The modular skid-mounted design enables full customization to match specific customer requirements.
The BHP industrial RO pure water system is a proven, standardized, fully integrated factory water treatment solution. Built on proprietary patented water-treatment technology, it combines multistage pretreatment with single-stage or two-pass reverse osmosis to deliver advanced feedwater purification and consistent industrial purified-water quality. The system operates independently as the primary water-supply unit for industrial parks or integrates with reclaimed-water equipment to reduce plant operating costs. Equipped with an EDI ultrapure-water module, product-water resistivity reaches 18.2 MΩ·cm, meeting stringent purity requirements for laboratories, semiconductor manufacturing, electronic-chip production, and precision industries. The modular skid-mounted construction minimizes facility footprint and accelerates delivery timelines. Complete turnkey industrial water purification systems are available for domestic and international projects.
1. Consistent Quality: Ultrapure Water Up to 18.2 MΩ·cm
Utilizing internationally recognized RO membranes and an intelligent PLC control system, the unit continuously monitors conductivity and resistivity online 24 hours daily, preventing water-quality fluctuations that could compromise production yield. Optimized pretreatment configurations for hard water and high-TDS feedwater extend membrane service life by over 30%. Models with integrated EDI consistently deliver ultrapure water with resistivity up to 18.2 MΩ·cm.
2. Energy & Water Efficiency: Cost Reduction Through Recycling
The optimized concentrate-recovery pipeline design achieves system recovery rates up to 80%. Filtered concentrate routes to the reclaimed-water treatment section for further reuse, reducing long-term factory water and electricity costs through energy-efficient operation.
3. Customized Solutions for Diverse Industrial Applications
Complete centralized purified-water equipment systems are tailored to water demand, feedwater quality, and industry-specific hygiene standards for industrial parks and manufacturing facilities. Sanitary-grade 304/316 stainless steel construction meets stringent requirements for food, pharmaceutical, and cosmetics processing.
4.Comprehensive Global After-Sales Support
The complete RO water treatment system carries CE and ISO export certifications for worldwide industrial deployment. The engineering team provides site surveys, customized system design, field installation, and operator training. Global 24/7 online technical support is available, and all overseas orders include English operating manuals and engineering drawings.
1. Centralized Water Supply for Industrial Parks
2. Electronics and New Energy Manufacturing
3. Food and Beverage Processing
4. Pharmaceutical and Cosmetics Industries
5. Industrial Boiler Applications
6. Boiler Feed Water Treatment
Integrates with reclaimed-water systems to provide advanced treatment of recycled wastewater for production reuse, helping factories achieve zero liquid discharge (ZLD) targets and reduce water consumption costs through circular water management.
BHP industrial RO pure water system, 0.5-100T/H, 18.2 MΩ·cm resistivity with EDI, PLC-controlled, for electronics, pharma, and food industries.

 EN