An industrial reverse osmosis plant depends fundamentally on the quality of water entering its system. Feed water characteristics directly determine pretreatment requirements, membrane lifespan, and overall operational efficiency. When an industrial reverse osmosis plant receives poor-quality feed water, the pretreatment stage becomes more complex and costly, yet it remains the most critical defense against membrane damage and system failure.
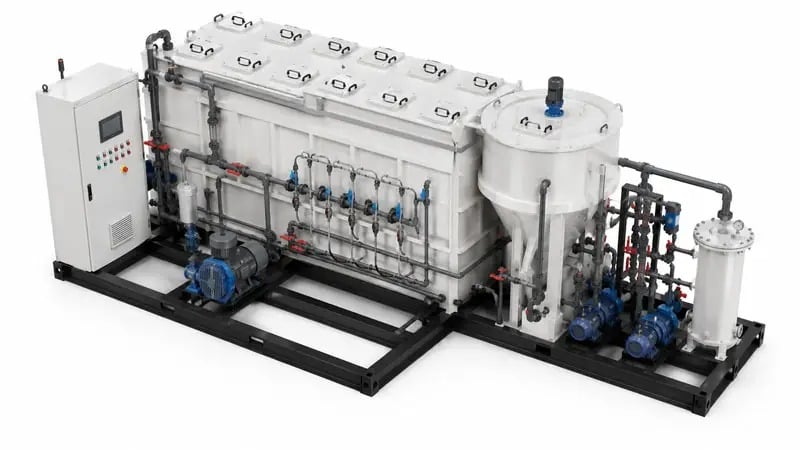
Understanding the relationship between feed water quality and pretreatment strategy is essential for operators, engineers, and plant managers. Industrial RO systems process thousands of gallons daily, making water composition analysis a cornerstone of reliable operation. Feed water turbidity, dissolved minerals, organic matter, and biological contaminants all influence which pretreatment technologies must be deployed. This article explores how feed water quality shapes pretreatment design and why proactive water analysis prevents costly fouling and membrane replacement.
Understanding Feed Water Quality Parameters
Suspended Solids and Turbidity
Feed water turbidity reveals the presence of suspended particles that threaten membrane integrity in an industrial reverse osmosis plant. Particles ranging from sand and silt to rust and scale can rapidly foul RO membranes if not removed during pretreatment. Turbidity levels above 1 NTU (Nephelometric Turbidity Unit) typically trigger multi-stage filtration requirements, including multimedia filters and cartridge stages. When feed water originates from groundwater, surface water, or recycled sources, suspended solids assessment becomes the first pretreatment decision point.
Hardness and Mineral Content
Calcium, magnesium, and other dissolved minerals in feed water create scaling risk on RO membranes unless pretreatment removes or controls them. An industrial reverse osmosis plant processing hard water must employ softening, antiscalant dosing, or both to prevent mineral precipitation. RO systems designed for soft feed water require minimal pretreatment, whereas those handling water with 200+ mg/L hardness demand comprehensive softening stages. Feed water analysis determines whether pretreatment includes ion exchange, scale inhibitor injection, or pH adjustment strategies.
Pretreatment Technologies Driven by Feed Water Characteristics
Multi-Stage Filtration Systems
Pretreatment design for an industrial reverse osmosis plant begins with filtration stages matched to feed water particle content and size distribution. Coarse multimedia filters remove sand and large debris, while cartridge filters target micron-level contaminants. Feed water containing high turbidity or algae requires multiple filtration passes to achieve the 5–10 micron particle sizes acceptable before RO. Without adequate pretreatment, fouling accelerates exponentially, reducing membrane flux and increasing pressure requirements. Industrial RO operators regularly measure feed water clarity to confirm that pretreatment filtration meets specification.
Chemical Softening and Antiscalant Application
When feed water contains elevated hardness, an industrial reverse osmosis plant requires pretreatment that removes calcium and magnesium ions or prevents their precipitation on membrane surfaces. Lime softening or ion exchange reduces hardness before the feed enters the RO vessel, while antiscalant additives protect against scaling of sparingly soluble salts. Pretreatment chemistry depends on both feed water mineral profile and the desired RO recovery rate. Industrial applications often combine mechanical softening with chemical inhibitor dosing for maximum fouling resistance. This dual approach extends RO membrane life by years and reduces maintenance intervals.
Feed Water Analysis and Pretreatment Design
Seasonal and Source Variability
Feed water quality fluctuates with weather, season, and source location, requiring adaptive pretreatment in an industrial reverse osmosis plant. Groundwater may show consistent mineral content but variable iron and manganese levels. Surface water exhibits dramatic turbidity swings during rainfall and seasonal algal growth periods. Industrial RO systems designed for single-season feed water often fail when processing water from different sources or during extreme weather. Comprehensive feed water testing establishes baseline parameters, identifies contaminant ranges, and drives pretreatment flexibility. Operators who adjust pretreatment settings based on feed water changes maintain consistent RO performance year-round.
Biological and Organic Contaminants
Feed water carrying dissolved organic matter, biofouling bacteria, and biofilm-forming compounds demands additional pretreatment steps within an industrial reverse osmosis plant. Microbial activity causes membrane biofouling, a fouling mechanism that reduces permeate flux and water quality. Pretreatment for biological contamination includes carbon filtration, UV disinfection, or chlorination followed by dechlorination with activated carbon. Feed water biological oxygen demand (BOD) and total organic carbon (TOC) testing guide the selection of pretreatment oxidation and absorption technologies. Industrial RO plants operating on surface water or recycled feed water must incorporate robust biological pretreatment to prevent biofilm accumulation inside the system.
Optimizing Pretreatment to Prevent Fouling
Real-Time Feed Water Monitoring
Advanced industrial reverse osmosis plant systems employ continuous feed water monitoring to detect quality changes and trigger pretreatment adjustments before fouling begins. Online turbidity sensors, differential pressure gauges, and conductivity probes provide real-time feedback on filtration effectiveness and pretreatment performance. When feed water turbidity spikes unexpectedly, operators can increase filter backwash frequency or tighten cartridge filter schedules before RO fouling occurs. Automated pretreatment systems linked to feed water sensors dynamically adjust antiscalant dosing, softening intensity, and filtration stages. This proactive approach reduces unscheduled downtime and extends RO membrane operating life significantly.
Pretreatment Maintenance and Replacement
Feed water quality directly determines pretreatment maintenance costs and replacement intervals for an industrial reverse osmosis plant. High-turbidity feed water clogs multimedia filters and cartridge stages rapidly, increasing backwash frequency and labor demands. Industrial RO plants processing contaminated feed water often replace filters every 3–6 months, whereas systems with clean feed water may extend intervals to 12–24 months. Predictive maintenance based on feed water analysis optimizes equipment life and operational budgeting. Plant managers who understand feed water characteristics can forecast pretreatment expenses accurately and align capital spending with seasonal demand variations.
FAQ
What feed water turbidity level requires pretreatment in an industrial RO system?
Feed water turbidity above 1 NTU typically demands multimedia or cartridge filtration before RO processing. Turbidity above 5 NTU requires aggressive multi-stage pretreatment with frequent backwashing. Most industrial reverse osmosis plant operators target feed water turbidity below 0.1 NTU after pretreatment to ensure membrane longevity and minimize fouling.
How does feed water hardness influence RO pretreatment design?
Feed water hardness above 150 mg/L typically triggers softening or antiscalant dosing within pretreatment stages. Industrial reverse osmosis plant systems handling extremely hard water often employ lime softening combined with antiscalant injection. Pretreatment softening reduces mineral scaling risk and allows higher RO recovery rates, improving system efficiency and water yield.
Can poor feed water quality damage an industrial RO system despite pretreatment?
Yes, inadequate or failed pretreatment allows fouling even in an industrial reverse osmosis plant with robust design. Unexpected feed water contamination, pretreatment equipment malfunction, or extreme turbidity spikes can overwhelm existing pretreatment stages. Continuous feed water monitoring and adaptive pretreatment adjustment are essential safeguards against membrane fouling and operational failure in industrial RO applications.

 EN






