
oilfield-produced-water-treatment-and-reuse-industry-solution, oilfield-produced-water-treatment-and-reuse-industry-solution, /solutions
EN
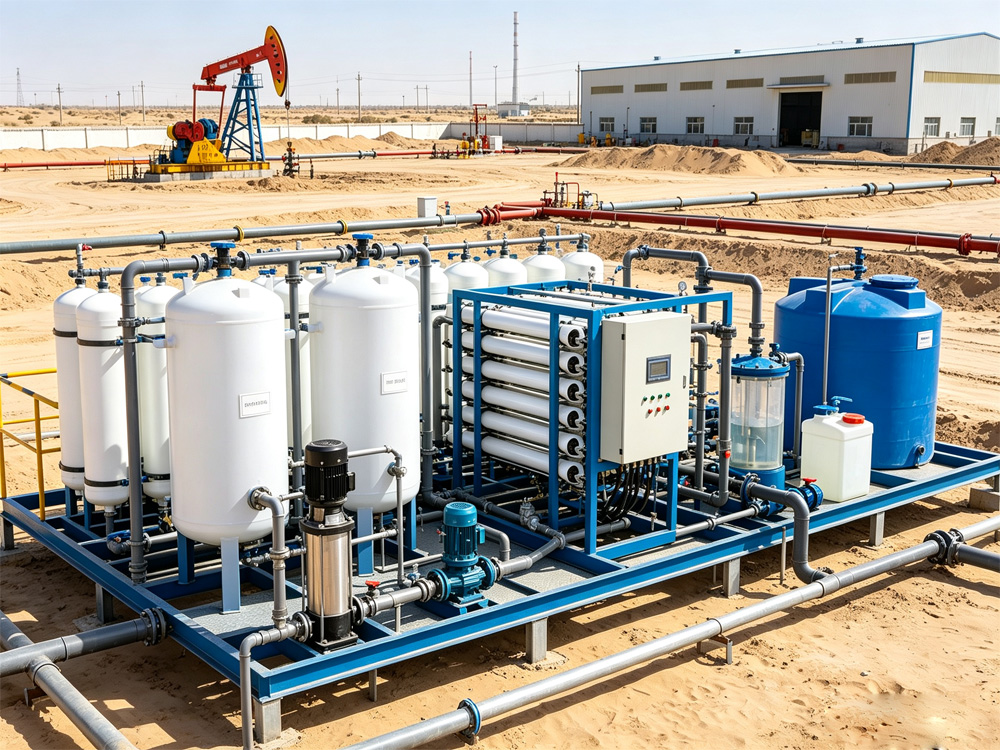
Oilfield produced water is formation water that is brought to the surface together with crude oil during oil production. It also includes wellhead operation wastewater, gathering pipeline flushing water, and wastewater generated from oilfield production stations. Produced water represents the largest volume of industrial wastewater generated in upstream oil and gas operations.
Produced water is characterized by high salinity, high oil content, and severe scaling potential. Typical contaminants include suspended crude oil, emulsified oil, paraffin wax, asphaltenes, sulfides, bacteria, colloidal suspended solids, high concentrations of chlorides, sulfates, calcium and magnesium hardness ions, and trace heavy metals in certain oilfields.
Overall, the wastewater exhibits extremely high Total Dissolved Solids (TDS), strong corrosiveness, complex chemical composition, and significant fluctuations in water quality and flow rate. Stable emulsified oil systems are difficult to separate naturally, often resulting in equipment scaling, corrosion, and pipeline blockage. Conventional treatment technologies typically struggle to provide consistent treatment performance. Treated water must comply with stringent standards for water injection, enhanced oil recovery (EOR), irrigation reuse, or environmental discharge, depending on the application.
Produced water treatment presents several critical operational challenges.
High concentrations of emulsified oil and organic colloids cannot be effectively removed through conventional sedimentation and filtration alone. If inadequately treated water is reinjected into the reservoir, it can cause formation plugging, reduce reservoir permeability, and negatively impact oil recovery efficiency.
Highly mineralized water with elevated hardness rapidly causes scaling and corrosion in pipelines, pumps, heat exchangers, and treatment equipment, resulting in frequent failures, increased maintenance, and high operating costs.
Sulfate-rich water combined with bacterial growth promotes hydrogen sulfide (H₂S) formation, leading to unpleasant odors, secondary contamination, microbiologically influenced corrosion (MIC), and equipment degradation.
Conventional standardized treatment equipment generally lacks sufficient resistance to high salinity, oil contamination, and corrosion, making it unsuitable for harsh oilfield environments. Furthermore, oilfield facilities are typically geographically dispersed with limited installation space and varying operating conditions, creating strong demand for customized, highly reliable, modular treatment systems.
To address the challenges of high oil content, high salinity, and severe scaling, our solution adopts the following integrated treatment process:
Multi-stage Oil-Water Separation → Water Conditioning & Sedimentation → Fine Filtration → Water Softening → Advanced Purification → Produced Water Reuse & Reinjection
Produced water first enters the pretreatment section, where high-efficiency oil separation equipment removes free oil, dispersed oil, and coarse suspended solids.
The conditioned water then passes through sedimentation units to further remove emulsified oil and colloidal contaminants.
An automatic water softening system effectively removes calcium and magnesium hardness ions, significantly reducing scaling risks throughout downstream equipment.
Finally, precision filtration combined with anti-fouling membrane treatment removes residual oil, dissolved salts, suspended solids, and other impurities, producing high-quality water suitable for oilfield water injection, reservoir reinjection, hydraulic operations, and other production reuse applications.
This solution is specifically engineered for the demanding operating conditions of oilfield produced water treatment. It effectively addresses the industry's three primary challenges: oil removal, high-salinity scaling, and unstable water quality, consistently producing treated water that meets oilfield reinjection and water reuse requirements while protecting reservoir permeability and improving oil recovery efficiency.
Customized equipment configurations are available based on produced water salinity, oil concentration, field conditions, installation space, and environmental requirements. Heavy-duty anti-corrosion housings, anti-fouling hydraulic designs, and high-pressure modular equipment are specifically designed to withstand harsh oilfield operating environments.
All core mechanical equipment, electrical control systems, and water treatment components are certified to CE, UL, and ISO international standards, ensuring outstanding operational reliability and compliance with international oilfield project specifications.
The treatment system provides excellent resistance to hydraulic and contaminant shock loading, significantly reducing scaling, corrosion, maintenance frequency, and equipment downtime. Water reuse rates of over 90% can be achieved, reducing freshwater consumption, lowering water sourcing costs, and minimizing environmental discharge requirements.
Its modular design features a compact footprint, rapid deployment, and fully automated operation, making it ideal for unmanned, remote, and decentralized oilfield production facilities.
We have successfully completed numerous produced water treatment and reinjection projects for onshore oilfields and petroleum production blocks.
A representative project involved a large-scale produced water treatment and reuse system with a treatment capacity of 2,500 m³/day. The system has operated reliably over the long term, successfully resolving issues related to excessive emulsified oil, pipeline scaling, and substandard injection water quality. Treated water consistently meets reservoir water injection specifications, helping improve production efficiency while successfully passing both owner acceptance inspections and environmental compliance audits.
We provide comprehensive EPC (Engineering, Procurement & Construction) turnkey solutions for oilfield produced water treatment and reuse, including:

 EN