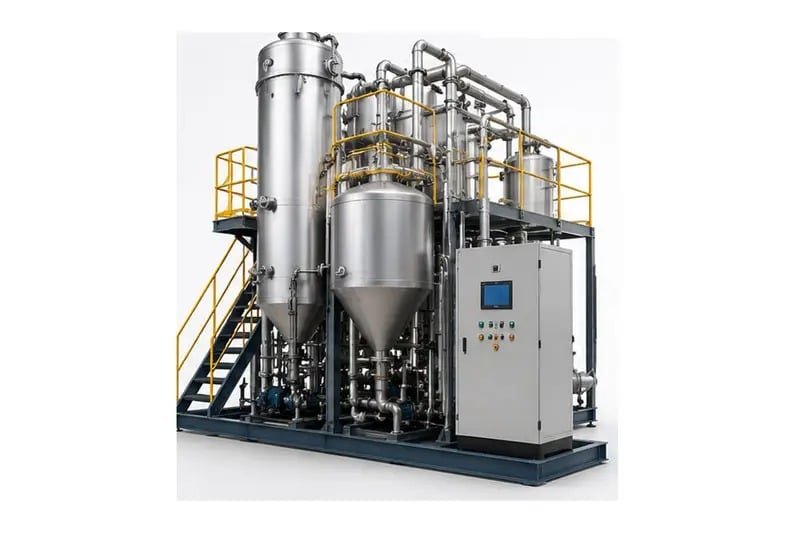
A brine evaporation system represents a critical infrastructure investment for industries managing high-salinity wastewater streams. Whether your operation produces concentrated brines from desalination, food processing, chemical manufacturing, or mining, the planning phase determines operational success, cost efficiency, and regulatory compliance. This guide addresses the essential components you must evaluate before implementing a brine evaporation system: utilities infrastructure, pretreatment requirements, and residue handling strategies that align with zero liquid discharge (ZLD) goals.
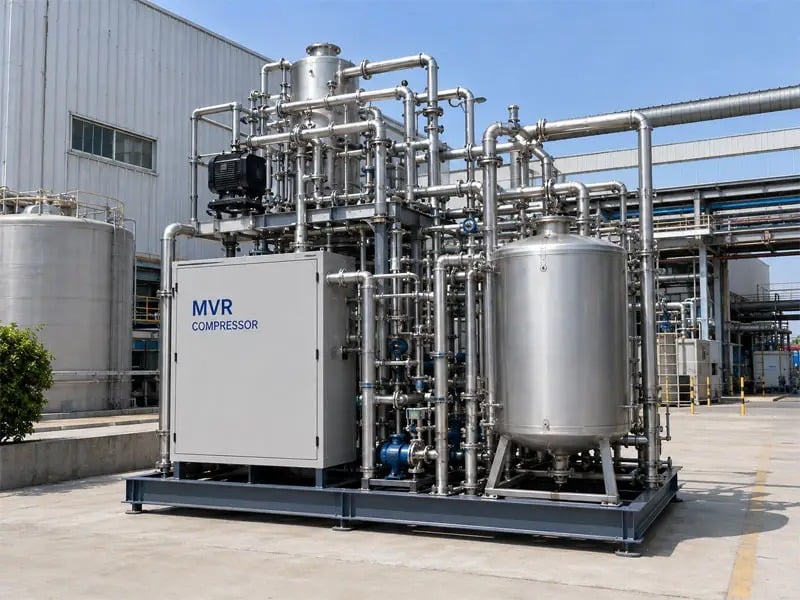
Planning a brine evaporation system without evaluating these three pillars leads to operational bottlenecks, unexpected capital expenses, and regulatory violations. Industrial facilities that integrate utilities assessment, comprehensive pretreatment, and residue management upfront experience 40% faster commissioning timelines and substantially reduced maintenance costs. The following sections break down each planning element so your team can make informed decisions aligned with your facility's production capacity, environmental constraints, and long-term sustainability objectives.
Utilities Infrastructure and Energy Requirements
Power Supply Demands for Brine Evaporation System Operation
Every brine evaporation system consumes substantial electrical power for mechanical vapor recompression (MVR), thermal systems, or hybrid configurations. A typical evaporator handling 10 to 50 cubic meters per hour of brine requires 150 to 500 kilowatts of continuous electrical input, depending on brine concentration, feed temperature, and desired evaporation rate. Before purchasing equipment, conduct a detailed electrical audit: verify your facility's available switchgear capacity, confirm three-phase power stability, and assess whether peak demand coincides with other operational loads that could trigger demand charges.
Many facilities discover during implementation that their electrical infrastructure cannot sustain the brine evaporation system's simultaneous startup with other equipment. This constraint necessitates either upgrading your substation, installing power factor correction systems, or implementing staged startup protocols. Utilities companies often require 90 to 180 days for grid connection upgrades, so advance notification and capacity planning prevent costly project delays.
Thermal Energy and Heat Recovery Considerations
Thermal-based evaporators and hybrid systems require steam supply, waste heat integration, or direct fuel combustion. If your facility operates a cogeneration plant or has excess thermal energy from manufacturing processes, a brine evaporation system can leverage that waste heat, reducing operational expenses significantly. However, integrating utilities this way demands precise thermal modeling: heat recovery exchangers must match your waste stream temperature profile, and condensate return lines must be sized correctly to avoid backpressure that reduces evaporator performance.
ZLD-focused operations often employ mechanical vapor recompression (MVR) to minimize external thermal energy demand, though MVR systems require robust electrical infrastructure. Hybrid approaches combining MVR with partial steam injection offer a middle path: they reduce electrical loads while maintaining flexibility during peak brine volumes. Your utilities assessment must quantify the cost differential between pure MVR, pure thermal, and hybrid configurations specific to your region's energy pricing and availability constraints.
Pretreatment Design and Feed Quality Control
Scaling and Fouling Prevention in Pretreatment Systems
Untreated brine entering an evaporator deposits mineral scales, biological films, and suspended solids that reduce heat transfer efficiency and force costly downtime for cleaning. Pretreatment removes these contaminants before the brine enters the evaporation chamber, extending equipment life and maintaining consistent performance. A comprehensive pretreatment strategy typically includes multimedia filtration (sand, anthracite, or GAC), antiscalant chemical injection, pH adjustment, and sometimes microfiltration or ultrafiltration for high-contamination streams.
The choice of pretreatment depends on your brine's specific composition. Oily wastewaters require coalescers or DAF (dissolved air flotation) ahead of filtration. Brines with high hardness need chemical softening or ion exchange. Brines containing silica near saturation require silica removal before the brine evaporation system to prevent irreversible deposits. Testing your actual feedstock through a pretreatment pilot plant reveals which modules are truly necessary, preventing overdesign that inflates capital cost and operational footprint.
Chemical Additives and Antiscalant Optimization
Antiscalant chemicals condition the brine to suppress mineral precipitation, allowing higher concentration factors and reducing residue production per unit of treated water. However, excessive antiscalant dosing increases operating costs and complicates downstream residue disposal or crystallization. Pretreatment optimization involves bench-scale testing to determine the minimum effective antiscalant dose, then validating that dose in continuous pilot trials using your facility's actual brine composition and temperature conditions.
Many industries overlook the interaction between pretreatment chemicals and residue handling. Antiscalants that prevent precipitation during evaporation may interfere with subsequent crystallization or brine concentration processes. Selecting pretreatment additives requires collaboration between your water treatment engineer, the brine evaporation system vendor, and your residue disposal partner to ensure the complete treatment train achieves ZLD or near-ZLD status without creating secondary waste streams.
Residue Management and ZLD Integration
Solid and Semi-Solid Residue Characterization
When a brine evaporation system operates, it concentrates dissolved salts and minerals until they precipitate or reach saturation. The resulting residue may be wet filter cake, dry crystalline solids, or semi-liquid slurries, each requiring different disposal or recovery pathways. Before committing to an evaporator, characterize the expected residue composition through evaporation trials: identify crystalline phases (halite, sulfates, silicates), measure moisture content, assess leachability for hazardous constituents, and determine storage volume or weight per thousand cubic meters of brine processed.
Residue disposal or beneficial reuse options range from landfill (often costly and increasingly restricted), to industrial salt recovery, mineral extraction, or road deicing applications. A brine evaporation system producing high-purity residue enables revenue-generating recovery contracts. Conversely, residue contaminated with heavy metals, organic compounds, or silicates may require secure disposal at hazardous waste facilities, significantly impacting the system's total cost of ownership.
ZLD Strategy and Closed-Loop Implementation
Zero liquid discharge (ZLD) means converting all brine into usable products or solid waste, eliminating liquid discharge entirely. Achieving ZLD with a brine evaporation system requires combining evaporation with crystallization, drying, or additional processing steps to transform even the most concentrated residual liquid into saleable or disposable solids. ZLD-focused utilities planning includes not only the brine evaporation system itself but also ancillary drying equipment, product storage, and logistics for residue transport or reuse.
The ZLD pathway increases capital expenditure and complexity compared to conventional evaporation-only systems, but regulatory pressures in many regions now mandate ZLD or near-ZLD performance. Planning a brine evaporation system with ZLD intent from the start simplifies permitting, reduces future retrofit costs, and positions your facility for stricter environmental standards anticipated over the next decade. Your planning must quantify the incremental cost of ZLD-ready infrastructure against your facility's discharge permits, environmental liability, and market reputation factors.
FAQ
What electrical infrastructure changes does a brine evaporation system require?
Most facilities need to upgrade switchgear, add dedicated transformer capacity, or install harmonic filters to accommodate the continuous high-power draw of a brine evaporation system. Mechanical vapor recompression systems typically require 150 to 500 kilowatts depending on capacity. Electrical audits should occur at least 6 months before installation to allow time for utility coordination, permitting, and construction of new infrastructure.
How does pretreatment reduce residue volume from a brine evaporation system?
Effective pretreatment removes suspended solids, biological matter, and unstable minerals before concentration, allowing the evaporator to operate at higher concentration factors without fouling. This means more water evaporates per unit of brine processed, and the residue contains fewer impurities, often enabling reuse or recovery. ZLD strategies benefit significantly because purer residue is more marketable and requires less specialized disposal.
Is a brine evaporation system necessary for ZLD compliance?
For most high-salinity brines, yes. Membrane technologies alone cannot achieve zero liquid discharge because reject streams remain. A brine evaporation system paired with crystallization or drying achieves true ZLD by converting the final concentrated brine into solid products. Some lighter brines may achieve near-ZLD through reverse osmosis alone, but regulatory definitions and site-specific permits typically mandate brine evaporation system integration for full ZLD certification.

 EN