
baihuipu-720m/d-mining-wastewater-treatment--reuse-system-for-sand-washing, baihuipu-720m/d-mining-wastewater-treatment--reuse-system-for-sand-washing, /case-studies
EN
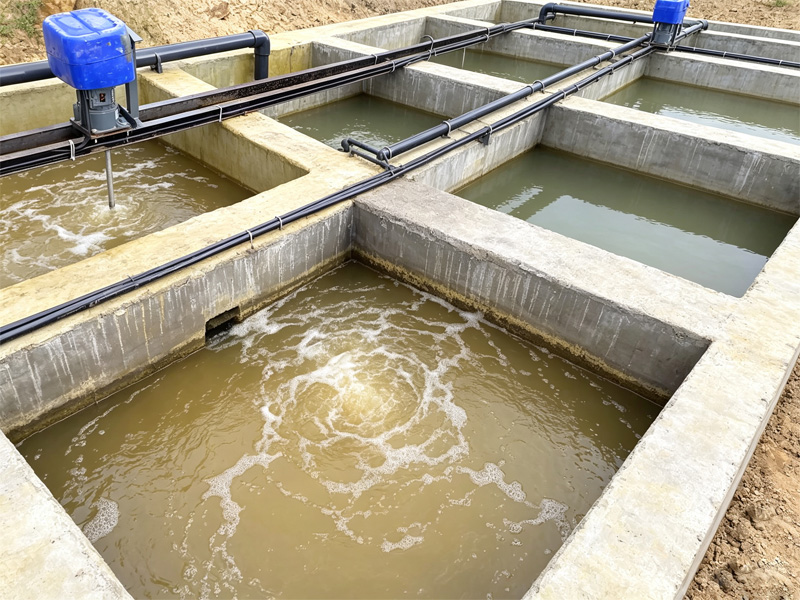
Designed for mining wash water conditions in Guangxi, the system integrates sedimentation, coagulation-flocculation, clarification and sand filtration to support wastewater recycling and continuous high-volume operation.
This project was developed for a mining enterprise in Guangxi, with a designed treatment capacity of 720m³/d. The system is designed for continuous mining washing operations with high volumes of wastewater generated from ore cleaning and aggregate washing processes.
The complete treatment process includes:
Mining wastewater collection → Equalization → Coagulation dosing → Flocculation reaction → High-efficiency inclined tube sedimentation → Sludge thickening and filter pressing → Multi-stage sand filtration → Recycled water storage
The system is designed to treat high-turbidity mining wastewater containing large amounts of suspended solids, fine mineral particles, sand, and slurry materials generated during ore washing activities. Through chemical coagulation, sedimentation separation, and filtration processes, the system reduces turbidity and suspended solids, improving water quality for production reuse.
Equipped with an automatic PLC control system, the equipment supports chemical dosing control, integrated operation management, and automatic sludge discharge functions. The system is designed to handle fluctuations in wastewater flow rate and turbidity during mining production, providing stable treatment performance with manageable operation requirements.
The equipment structure is suitable for complex outdoor mining environments, offering practical installation flexibility, corrosion resistance, and continuous operation capability for large-scale mining wastewater recycling applications.
 |
|
This mining wastewater treatment and recycling system is suitable for:
Mining wash wastewater typically contains high concentrations of fine sand, mineral powder, and suspended particles, resulting in high turbidity and limited direct reuse potential.
The system is designed for new mining wastewater recycling stations, upgrading of existing washing water treatment facilities, water-saving improvement projects, and tailings wastewater pretreatment applications.
It supports mining enterprises in improving water reuse efficiency, reducing freshwater consumption, and meeting environmental management requirements for sustainable production.
 |
 |
 |
Guangxi has abundant mineral resources, supporting large-scale mining, ore washing, and aggregate processing industries. During mining operations, continuous wastewater is generated from ore cleaning and sand washing processes.
Unlike industrial wastewater containing complex chemical pollutants, mining wash wastewater mainly contains fine mineral particles, suspended solids, and sediment. Due to the small particle size and slow natural settling characteristics, conventional settling ponds often have limited performance in reducing turbidity. Insufficient treatment may affect water reuse efficiency, increase freshwater consumption costs, and create environmental management challenges for mining operations.
To address the requirements of 720m³/d high-volume mining wastewater treatment, Baihuipu developed a customized recycling solution combining equalization, coagulation-flocculation, high-efficiency clarification, and filtration technologies.
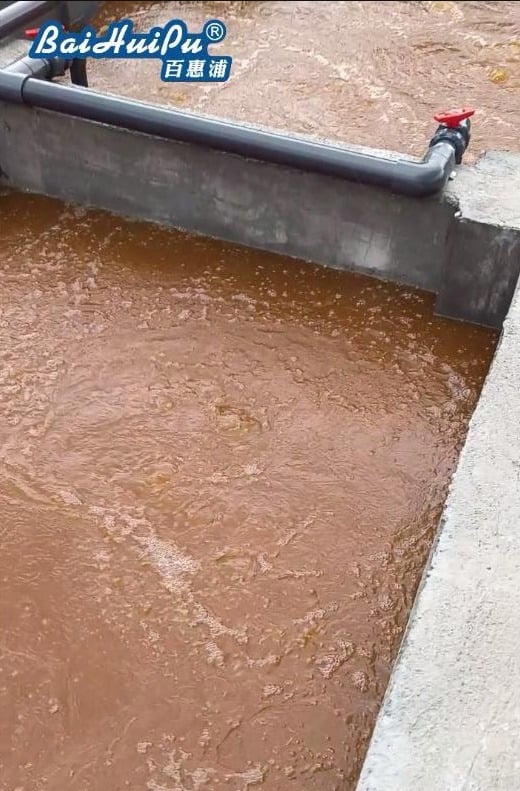
The wastewater first enters the large-capacity equalization tank, where fluctuations in flow rate and turbidity caused by continuous mining operations are balanced. This process helps stabilize the influent conditions and provides more consistent loading for downstream treatment units.
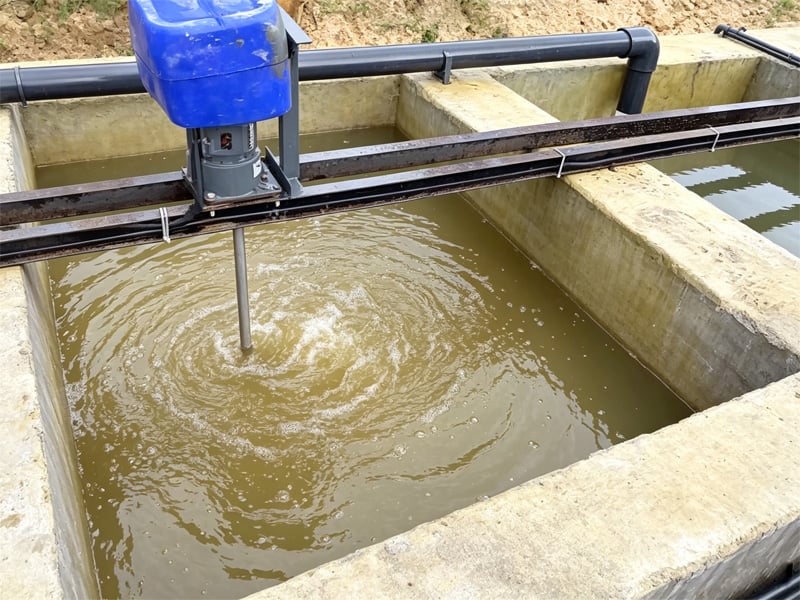
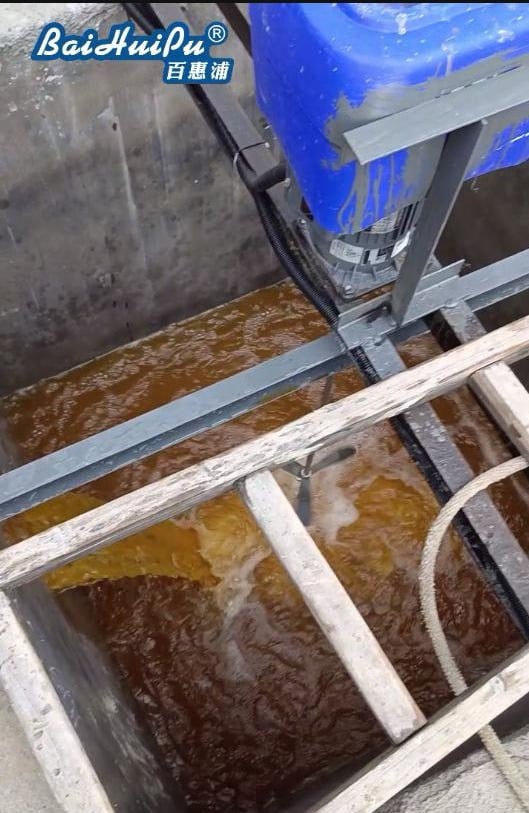
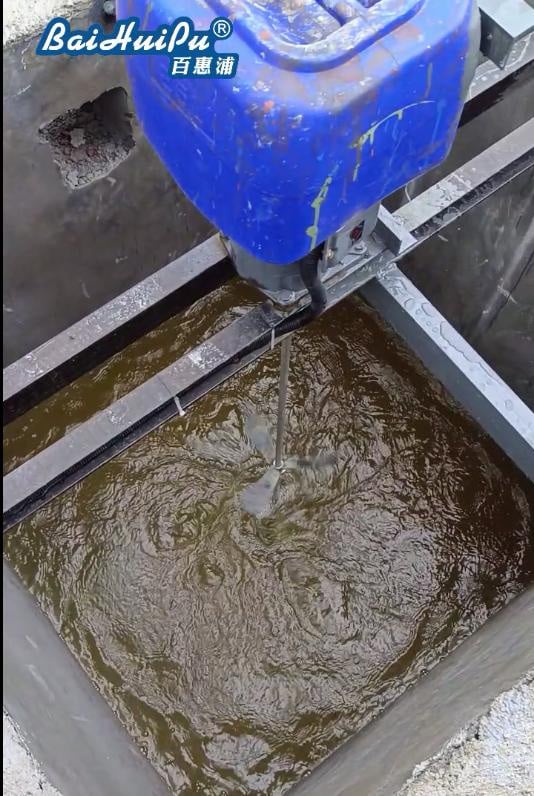
The wastewater then enters the coagulation and flocculation stage. Through controlled chemical dosing, fine mineral powders, suspended particles, and colloidal substances gradually aggregate into larger flocs, improving separation efficiency.
The flocculated wastewater flows into the inclined tube sedimentation tank, where enhanced surface settling technology promotes solid-liquid separation. Most mineral solids and sediment settle at the bottom and are transferred to the sludge treatment system. After thickening and filter pressing, the dewatered sludge can be collected for centralized disposal or resource utilization according to site requirements.
The clarified water passes through multi-stage quartz sand filtration units to further remove remaining fine particles and improve water clarity. The treated water can be returned to mining washing and aggregate cleaning processes, supporting internal water circulation.
After project commissioning, the system provides stable treatment for approximately 720m³/d mining wastewater, supporting continuous production with reduced freshwater demand. With automated operation, adaptable treatment capacity, and practical maintenance features, the project provides a reliable wastewater recycling solution for mining enterprises in Guangxi and surrounding regions.

 EN