
8-m3/h-industrial-ro-pure-water-system-for-advanced-materials, 8-m3/h-industrial-ro-pure-water-system-for-advanced-materials, /case-studies
EN
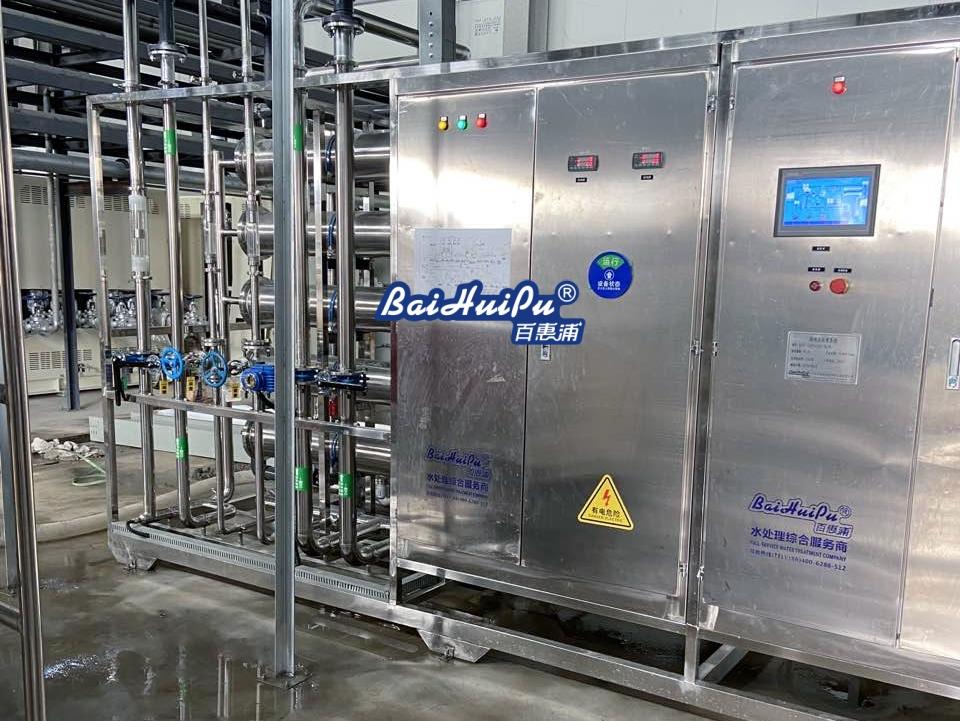
Designed for advanced materials manufacturing, this system combines multi-stage pretreatment with double-pass RO purification to deliver 8 m3/h of stable high-purity water for production, cleaning, and cooling applications with fully automated operation.
This project was implemented for an advanced materials manufacturer in Hubei, China, providing a customized industrial pure water production system with a design capacity of 8 m3/h. The system supports both continuous 24/7 production and intermittent water demand while consistently meeting industrial pure water standards required by the advanced materials and specialty chemicals industries.
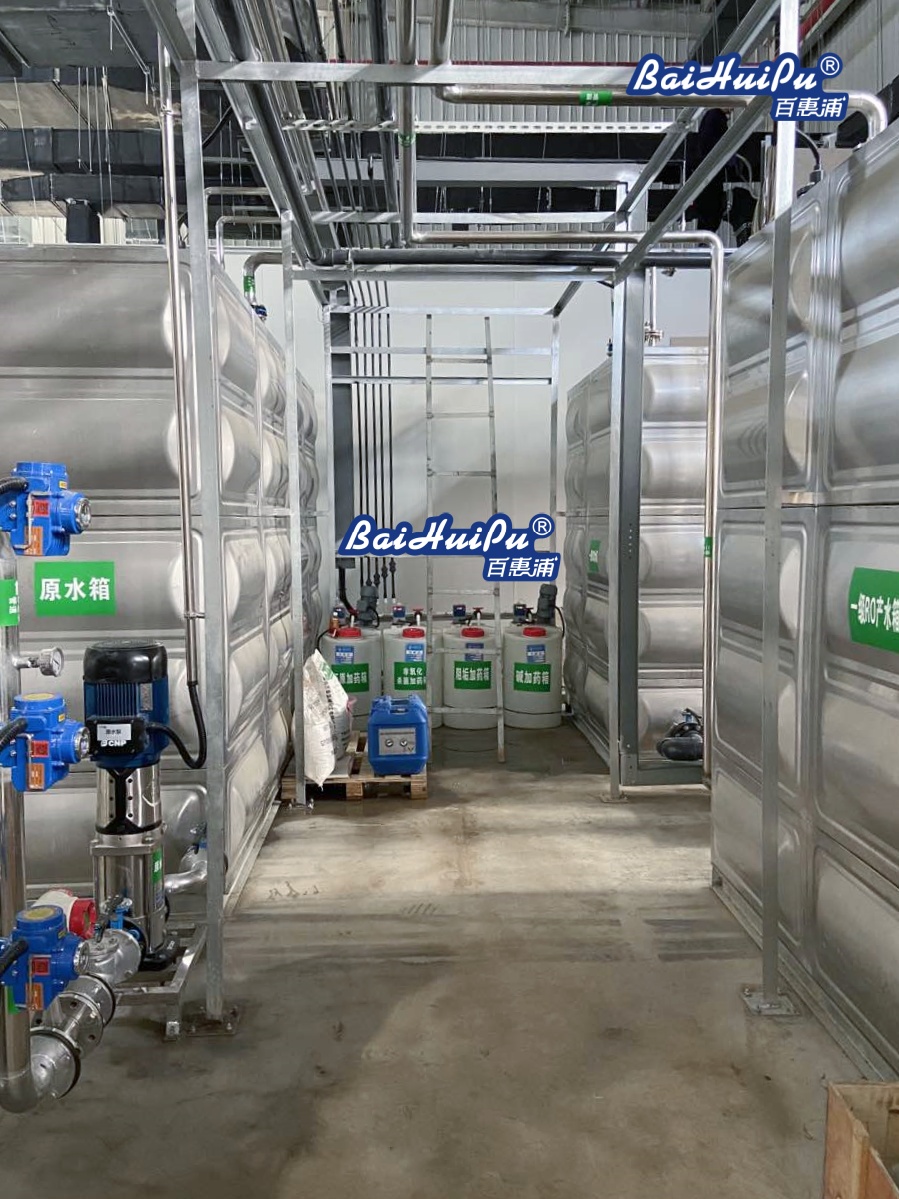
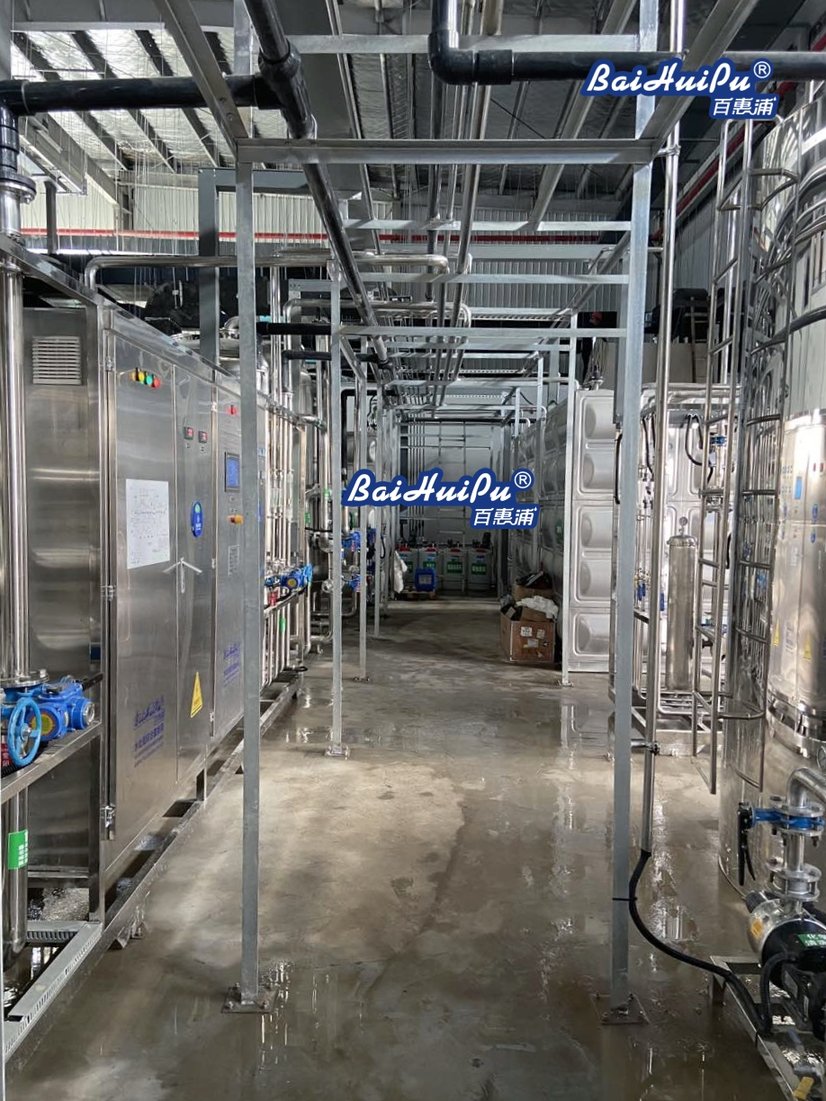
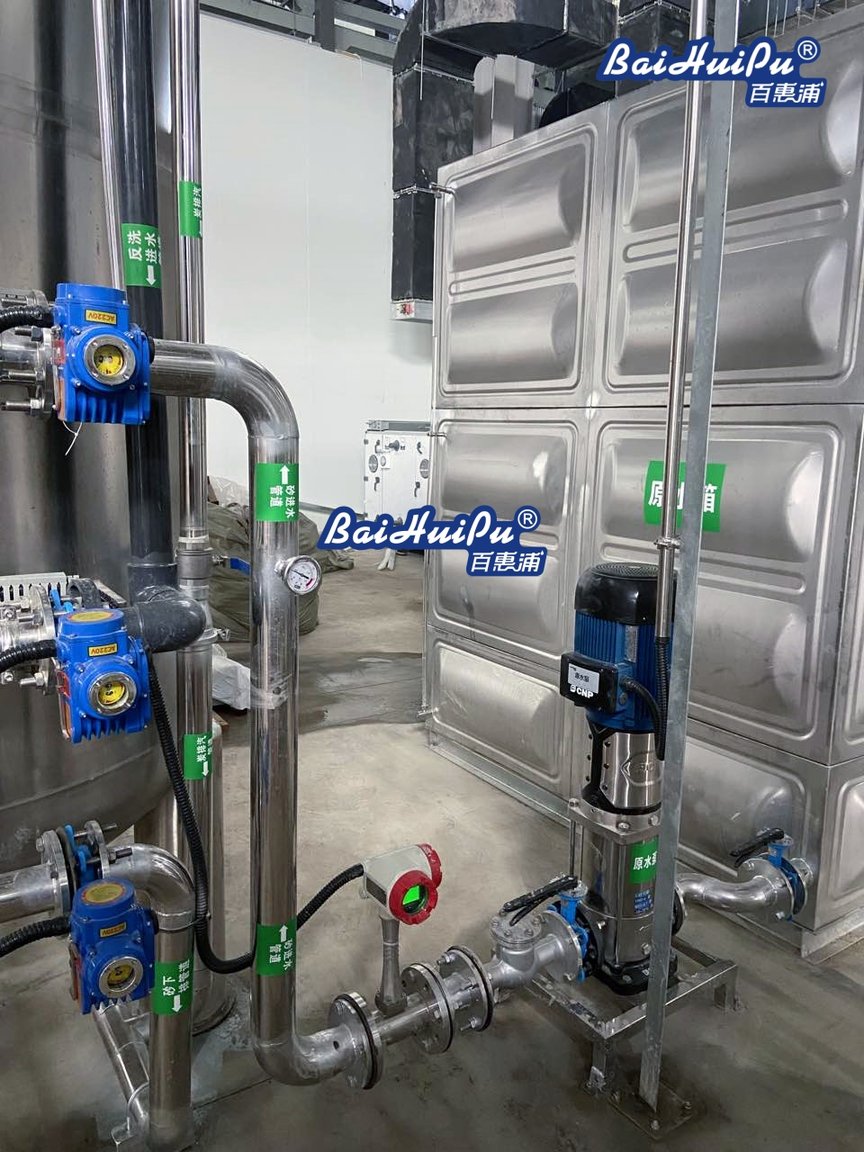
Raw Water Booster Pump → Multi-Media Filter → Activated Carbon Filter → Precision Cartridge Filter → Double-Pass Reverse Osmosis (RO) → Pure Water Storage Tank → Constant-Pressure Water Supply
The pretreatment section effectively removes suspended solids, sand, rust, colloids, residual chlorine, organic contaminants, and odor, protecting downstream RO membranes from scaling, fouling, and premature wear.
The double-pass RO system efficiently removes dissolved salts, heavy metals, and dissolved impurities, delivering stable, high-quality purified water suitable for precision manufacturing.
The equipment is well suited to Hubei's local water quality and continuous industrial production environments.
Hubei is one of Central China's major manufacturing hubs for advanced materials, specialty chemicals, and high-performance industrial products. These industries require highly stable, ultra-clean process water throughout manufacturing operations.
Although municipal water meets drinking water standards, it still contains dissolved minerals, metal ions, colloidal particles, residual chlorine, and other impurities that can negatively affect precision manufacturing processes. Using untreated water may result in inconsistent formulations, lower material purity, surface defects, unstable production processes, and reduced product yield.
To satisfy the customer's stringent production requirements, BHP designed and supplied a customized 8 m³/h industrial pure water system based on multi-stage pretreatment and double-pass reverse osmosis technology. The system provides continuous, reliable production of high-quality purified water while accommodating both continuous and variable water consumption throughout the facility.
Raw water first passes through a booster system before entering the pretreatment section. Multi-media filtration removes suspended solids and coarse particles, while activated carbon filtration eliminates residual chlorine, organic compounds, taste, and odor. This pretreatment significantly improves feed water quality and extends the service life of downstream membrane components.
The pretreated water then passes through a precision cartridge filter that removes fine particles before entering the double-pass RO system. High-pressure membrane separation efficiently removes dissolved salts, heavy metals, colloids, and trace contaminants, producing industrial-grade pure water that fully complies with advanced materials manufacturing requirements.
The entire system operates automatically through an intelligent PLC control platform. Functions such as automatic load adjustment, scheduled membrane flushing, pressure regulation, and continuous monitoring minimize manual intervention while preventing membrane fouling and reducing operating costs.
Following commissioning, the system has consistently delivered stable water quality and reliable production capacity. The purified water now supports material formulation, synthesis, cleaning, laboratory analysis, and other critical manufacturing processes throughout the facility.
The project has successfully eliminated production risks associated with poor source water quality, improved finished product consistency and manufacturing yield, and provided an energy-efficient, low-maintenance water treatment solution. Today, it serves as a benchmark industrial pure water project for the advanced materials industry in Central China.

 EN