
50-m/h-industrial-water-reuse-system--advanced-wastewater-recycling-solution-for-energy-facilities, 50-m/h-industrial-water-reuse-system--advanced-wastewater-recycling-solution-for-energy-facilities, /case-studies
EN
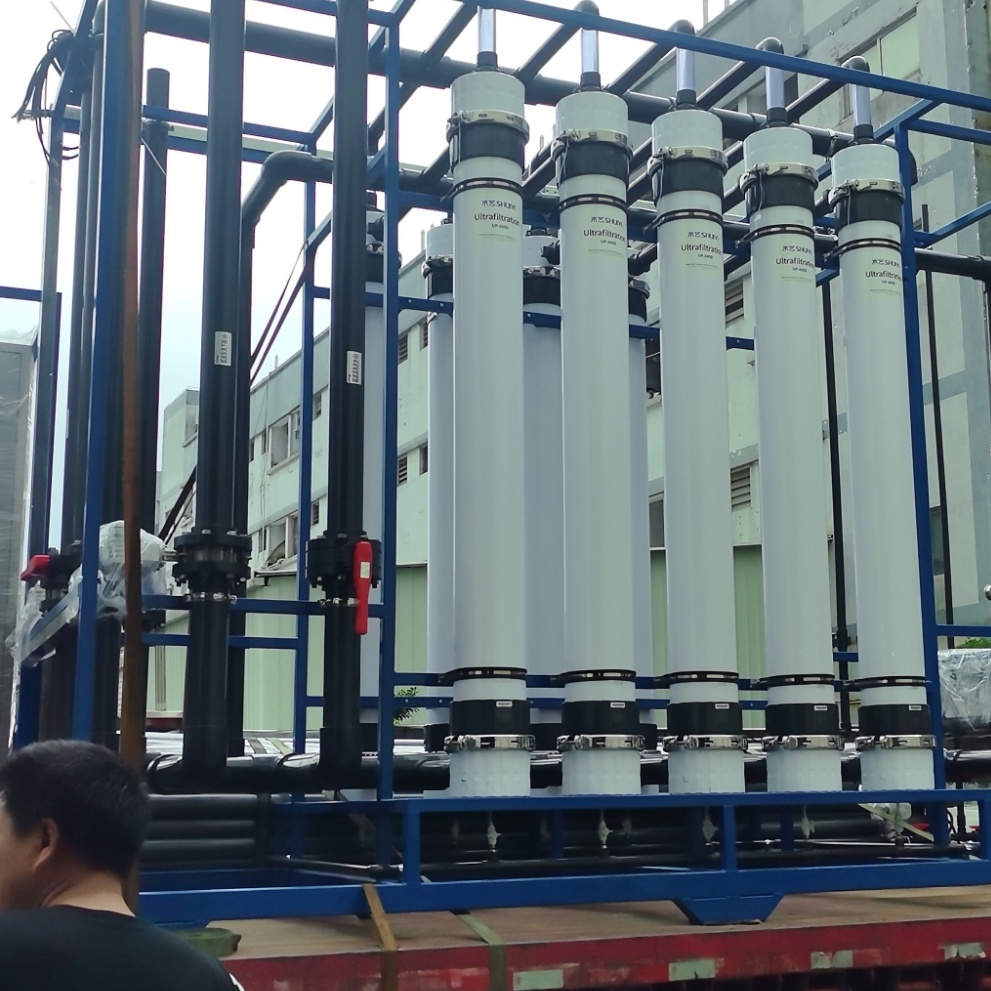
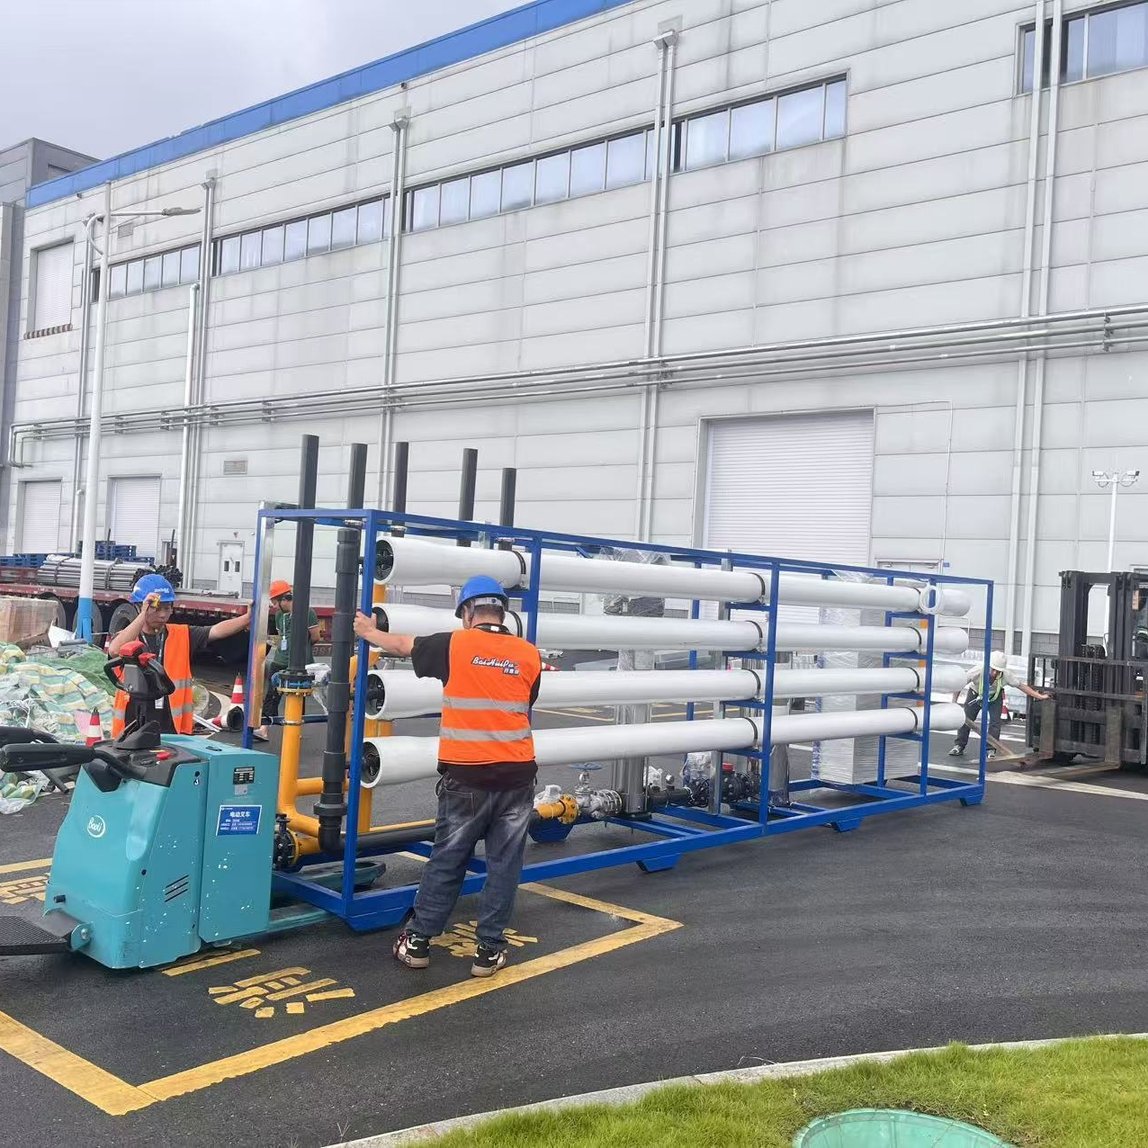
Designed for energy industry wastewater reclamation, this 50 m³/h industrial water reuse system utilizes pretreatment, ultrafiltration (UF), and reverse osmosis (RO) double-membrane technology to remove suspended solids, dissolved salts, and organic contaminants, delivering stable reclaimed water for cooling systems, process make-up water, and industrial reuse.
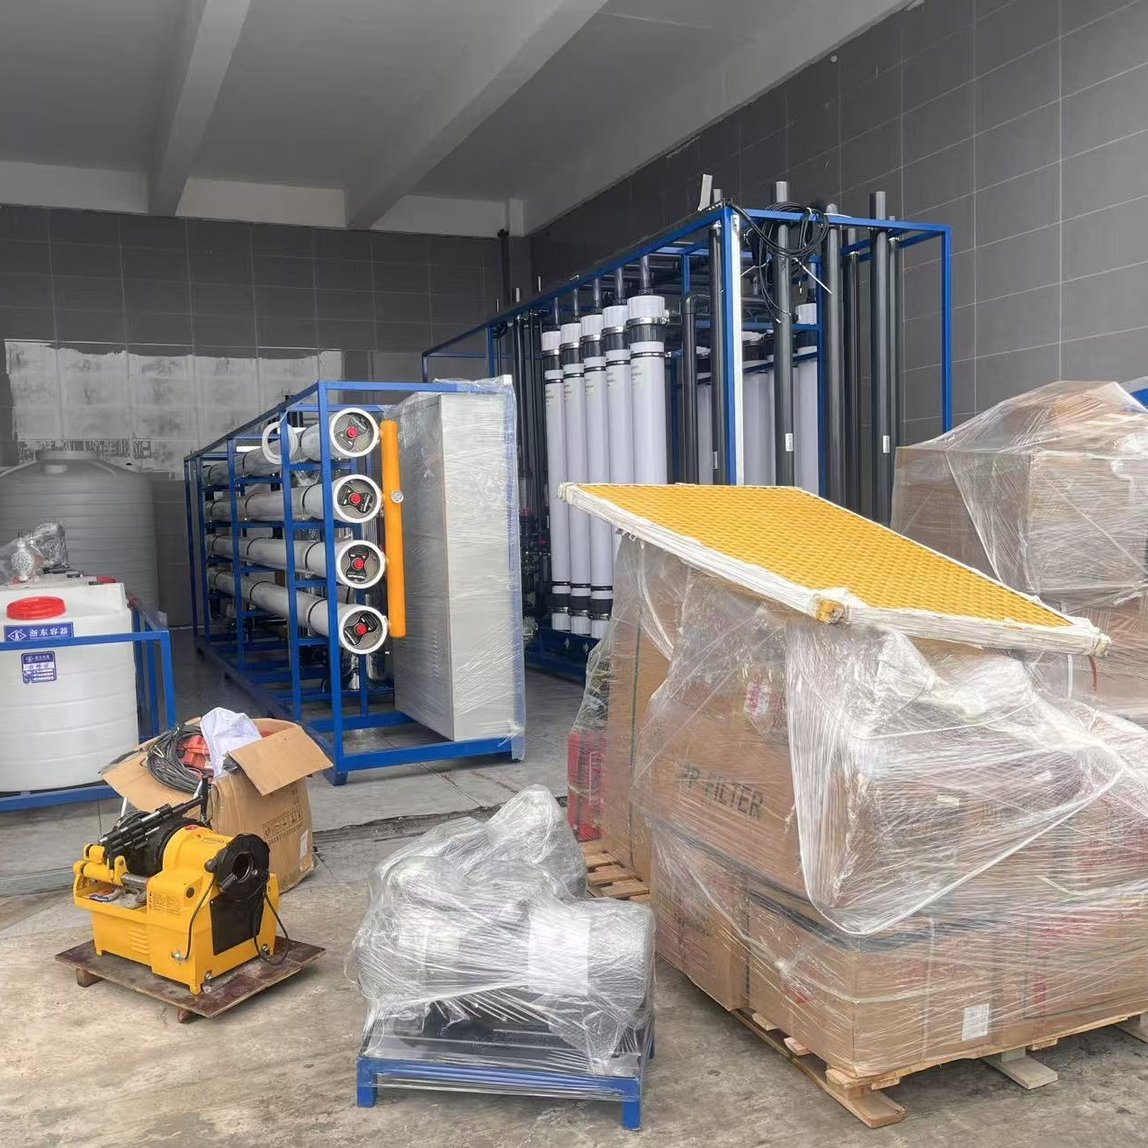
This project was implemented at an energy production facility in Chongqing, China. The system was designed with a treatment capacity of 50 m³/h, providing continuous reclamation of industrial wastewater generated from production processes, equipment cleaning, and cooling water blowdown.
Engineered for high-volume, continuous industrial operations, the system employs a proven dual-membrane treatment process to ensure stable reclaimed water quality while reducing freshwater consumption.
Wastewater Collection → Equalization Tank → Coagulation & Filtration → Precision Pretreatment → Ultrafiltration (UF) → Reverse Osmosis (RO) → Disinfection & Pressure Stabilization → Water Reuse
The treatment system effectively removes:
This enables treated water to meet industrial reuse requirements for various non-potable applications.
The integrated PLC automation system provides:
Designed for stable operation under varying hydraulic loads, the system offers low operating costs, controlled energy consumption, and simplified maintenance.
 |
 |
 |
This industrial reclaimed water system is suitable for:
The system is ideal for facilities seeking to reduce freshwater consumption, lower wastewater discharge volumes, and comply with increasingly stringent environmental regulations.
 |
 |
 |
During daily operation, the Chongqing energy facility generates substantial volumes of industrial wastewater from cooling systems, equipment maintenance, and plant cleaning operations.
Although this wastewater undergoes preliminary treatment, it still contains suspended solids, residual organic matter, and dissolved mineral salts that prevent direct reuse in industrial processes.
Conventional discharge not only wastes valuable water resources but also increases freshwater procurement costs and wastewater disposal expenses while making it more difficult to achieve corporate sustainability and environmental compliance objectives.
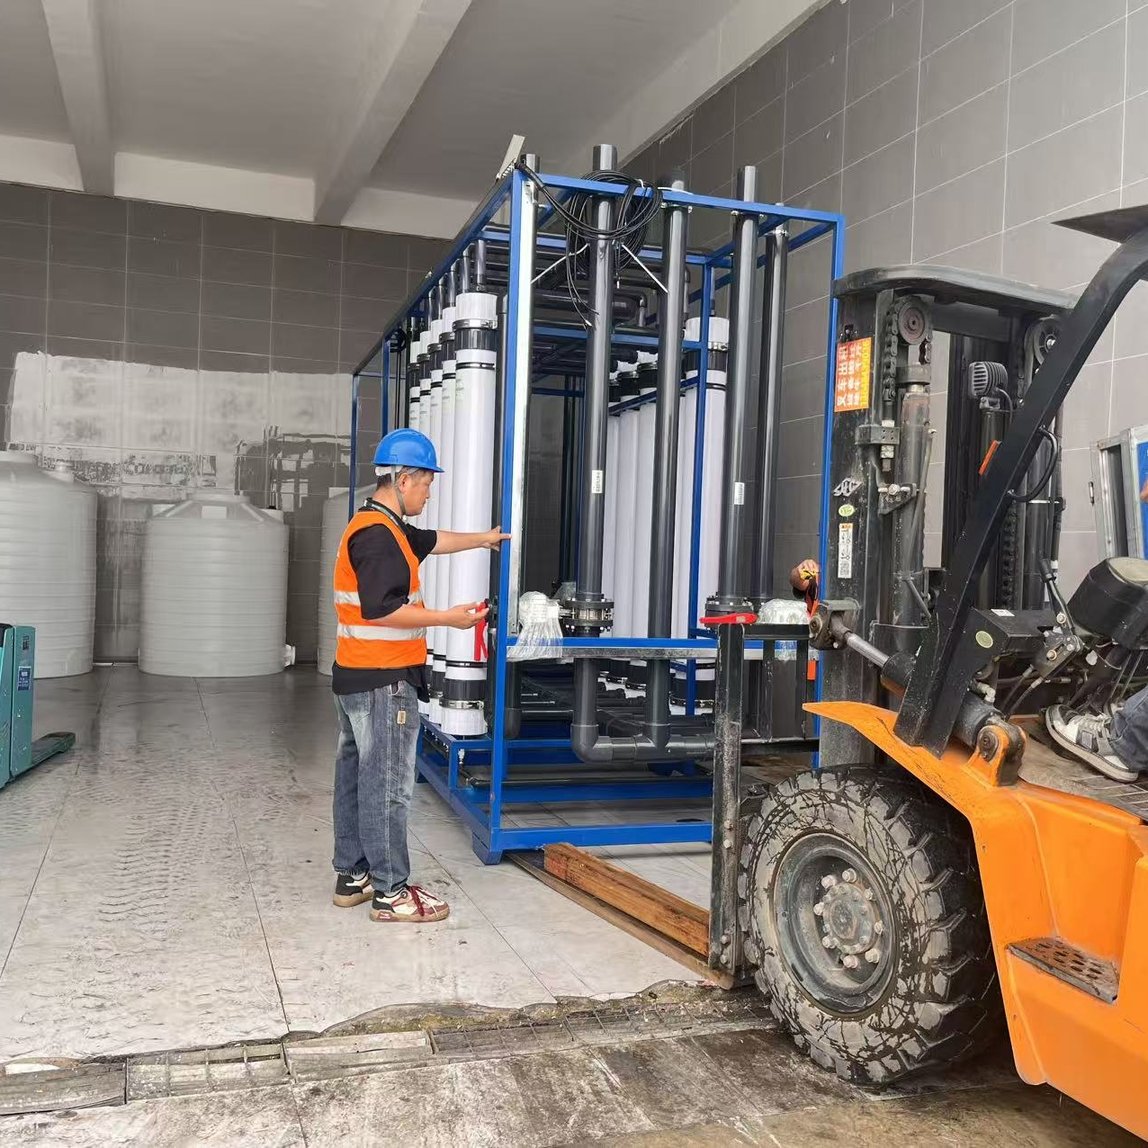
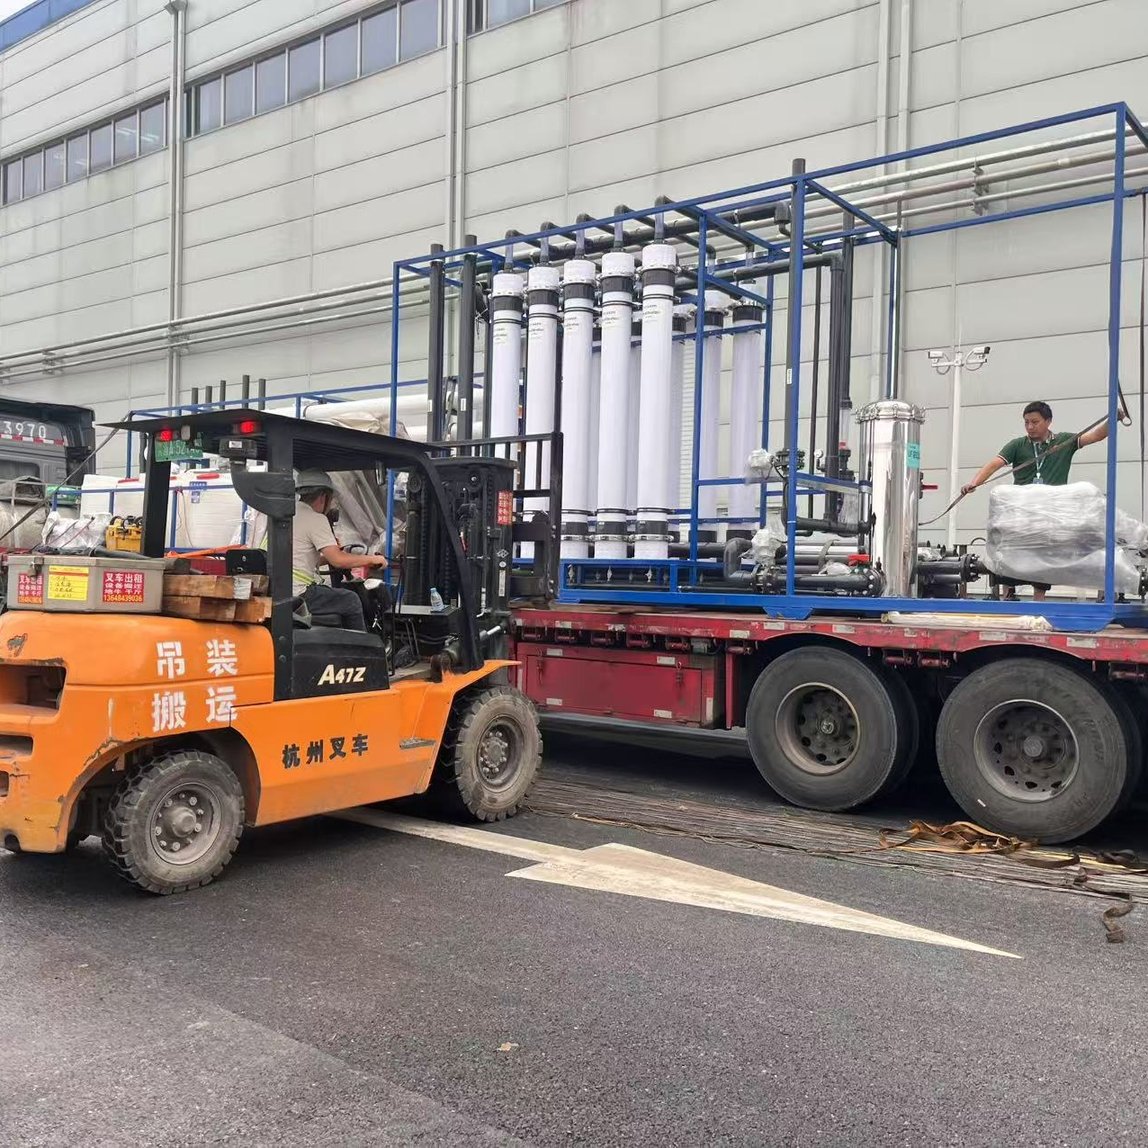
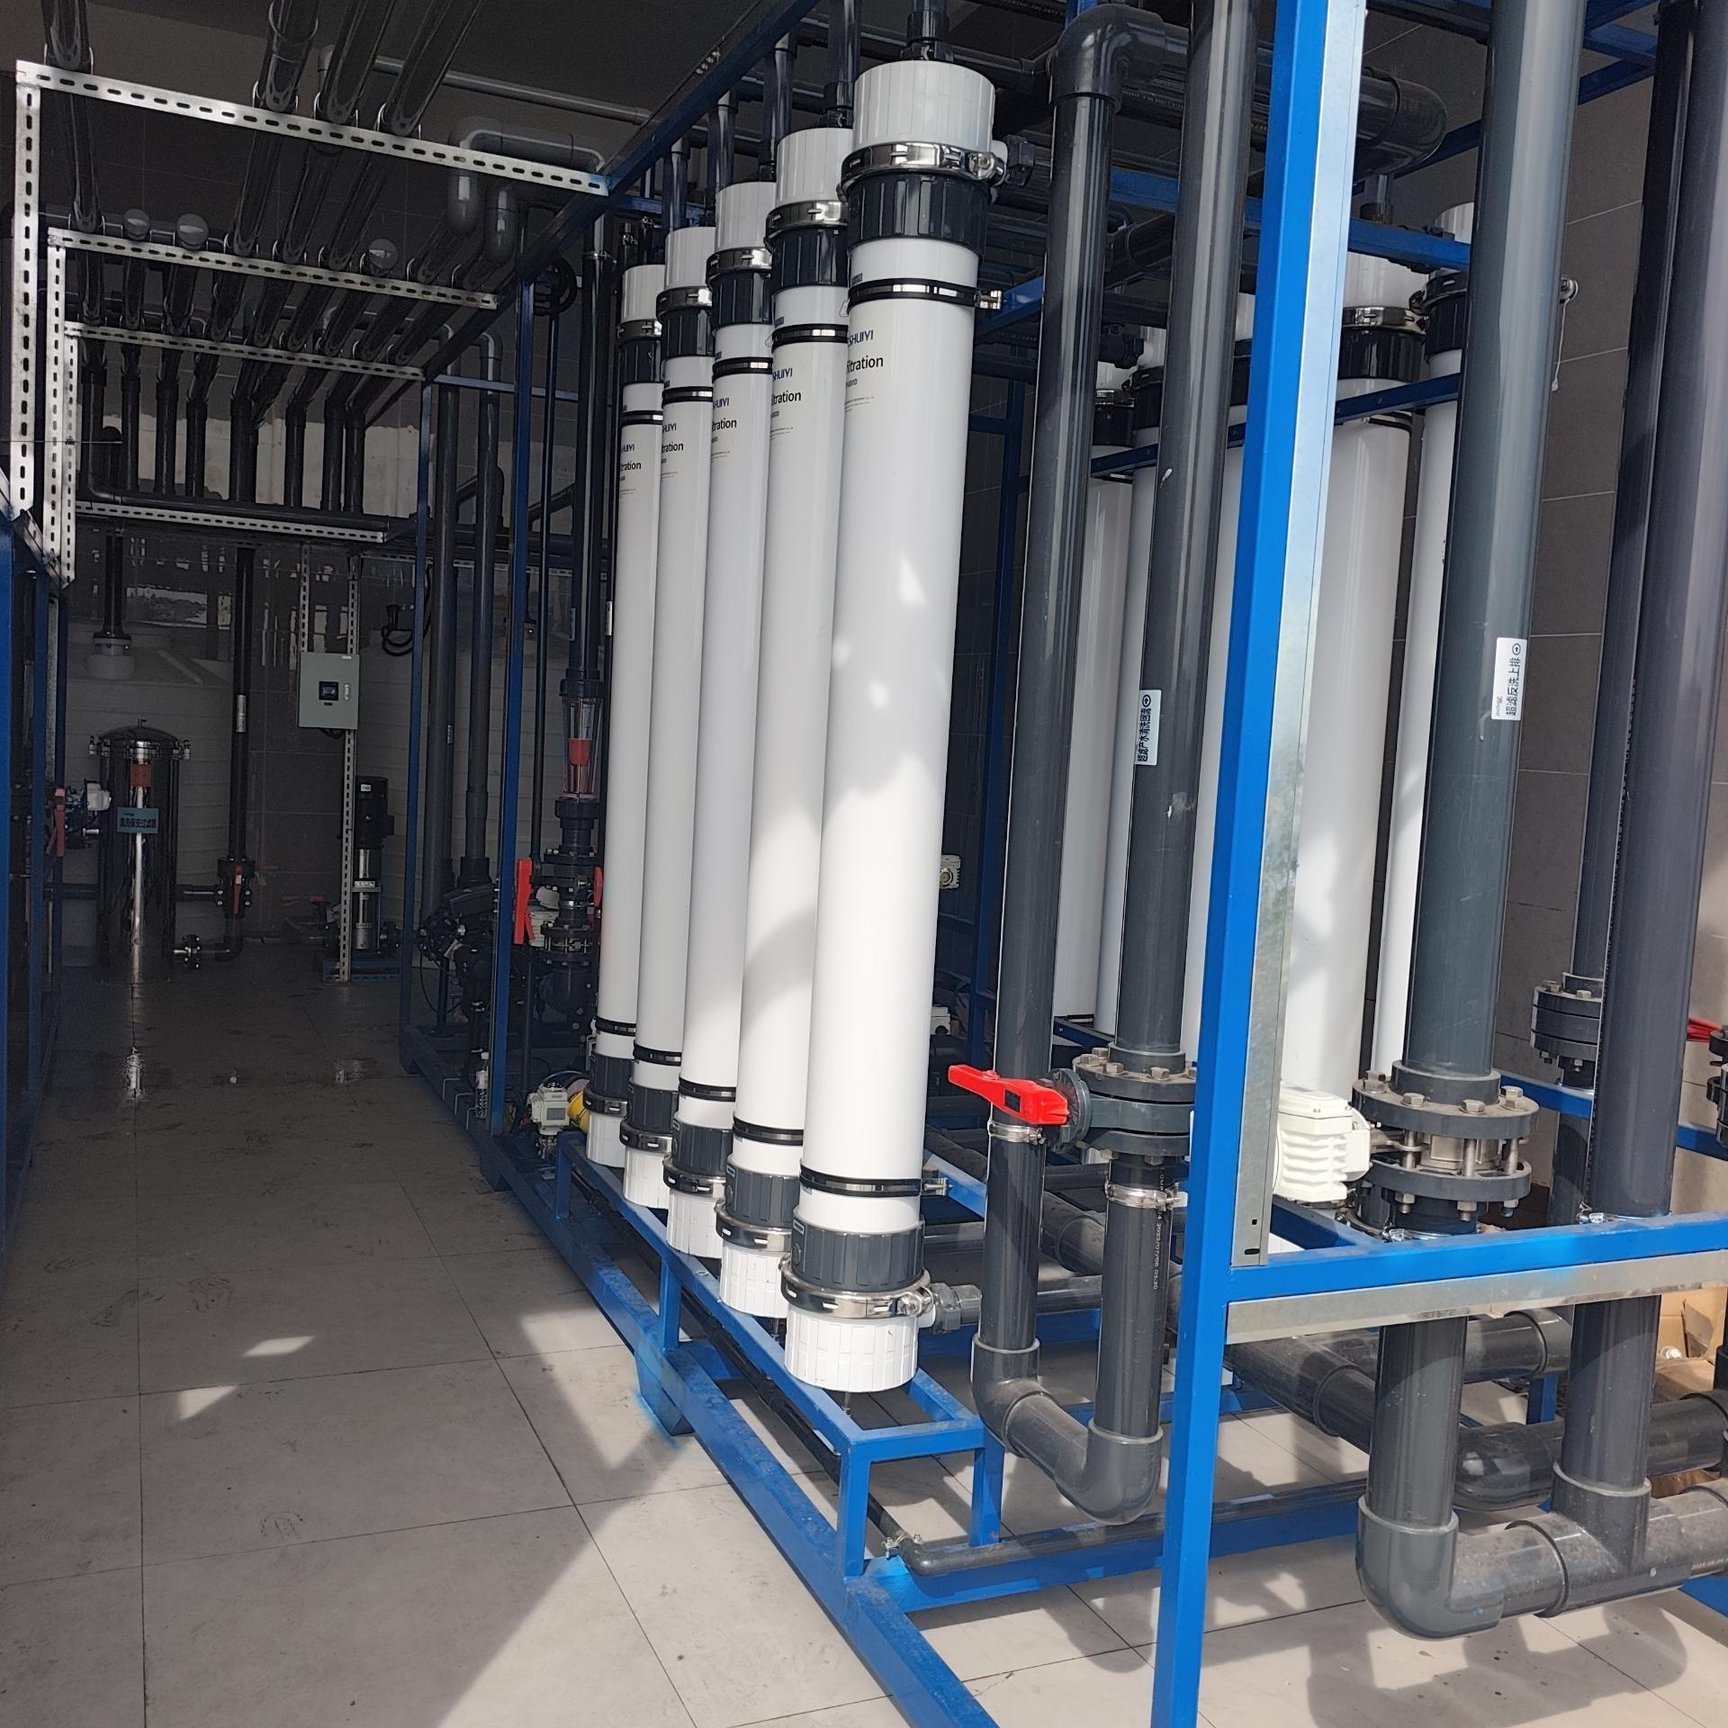
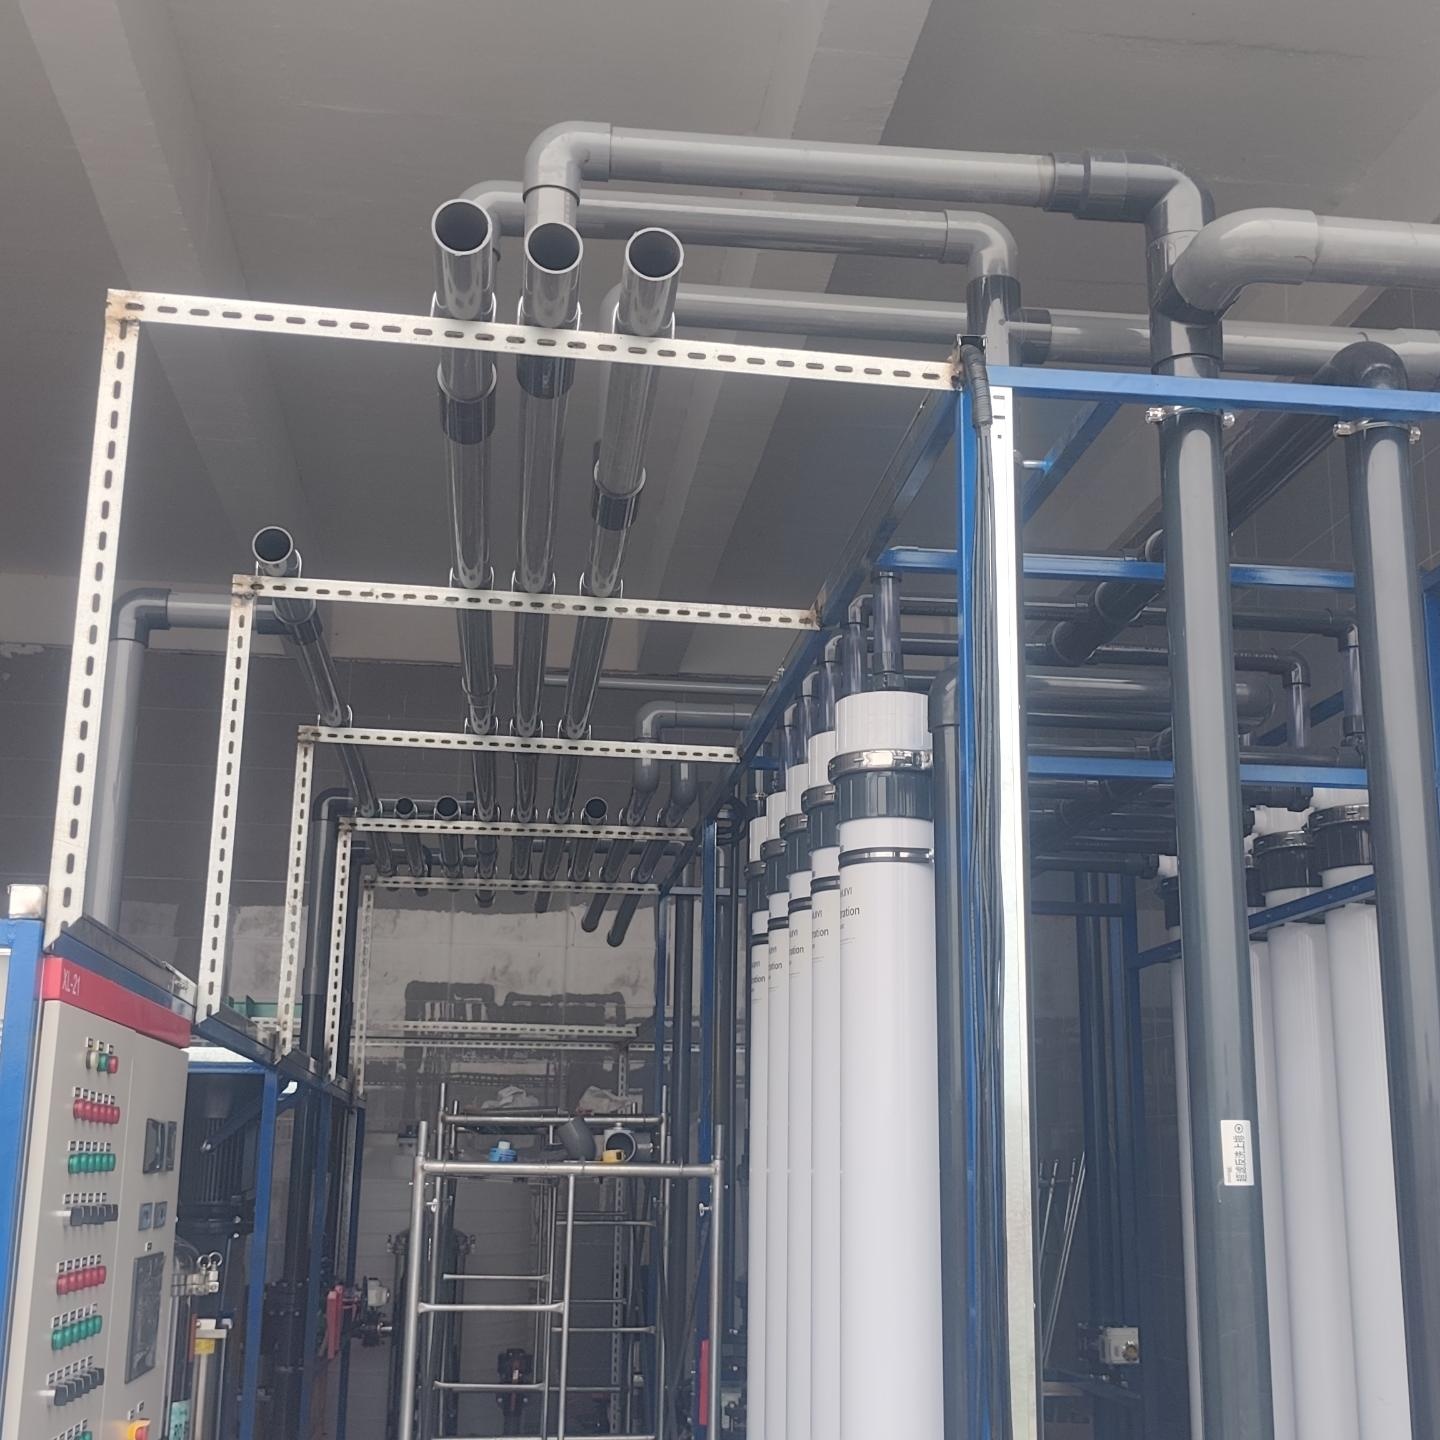
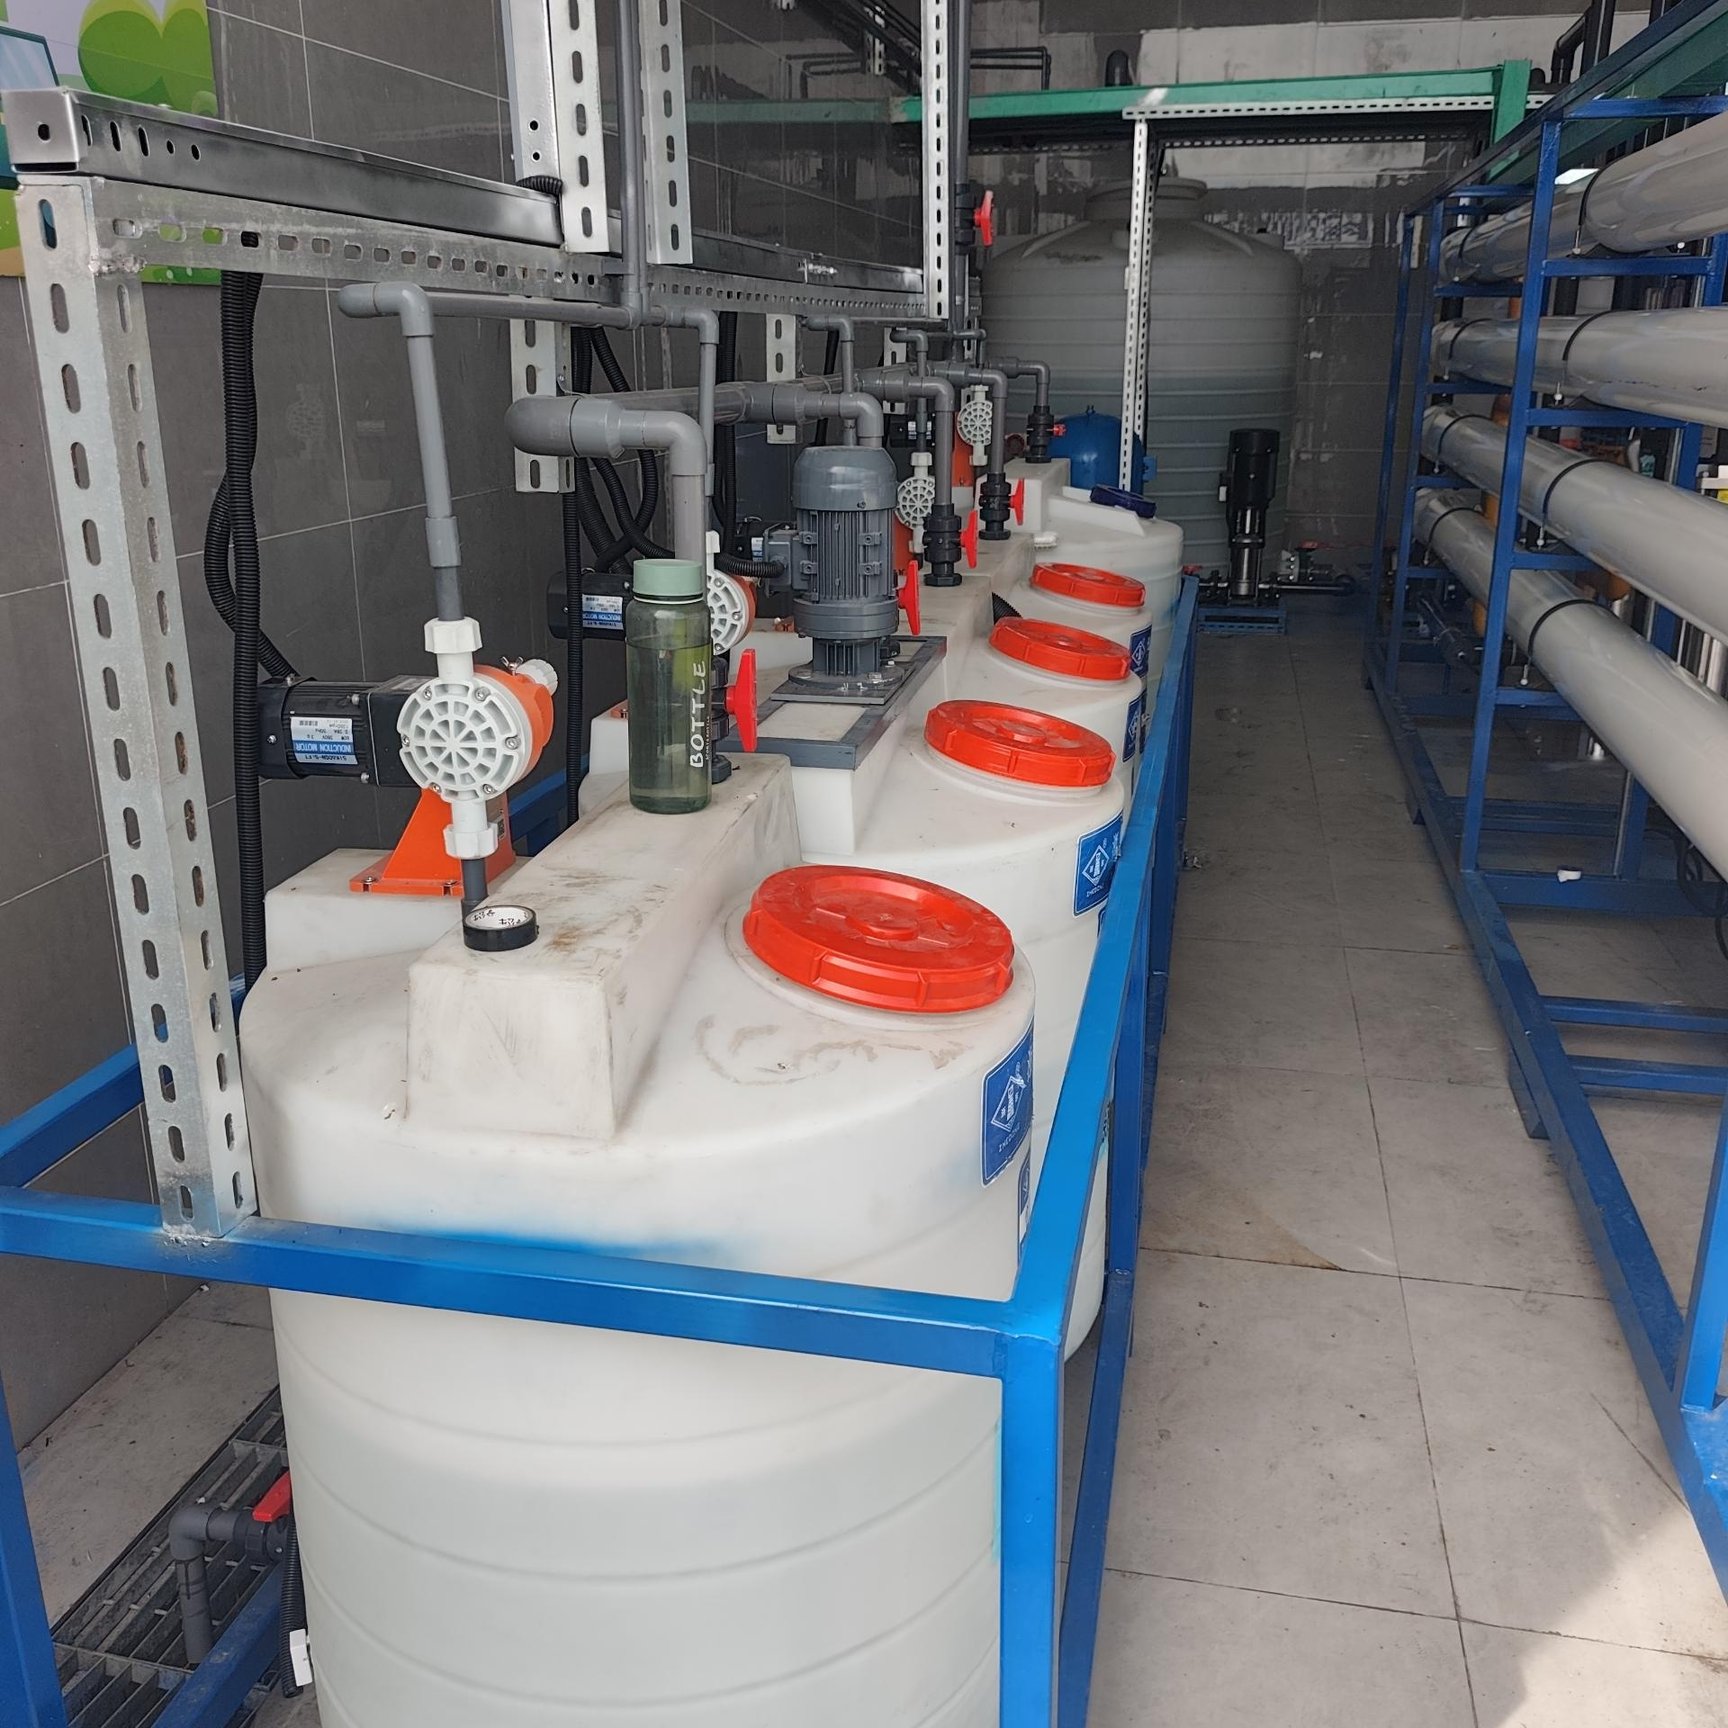
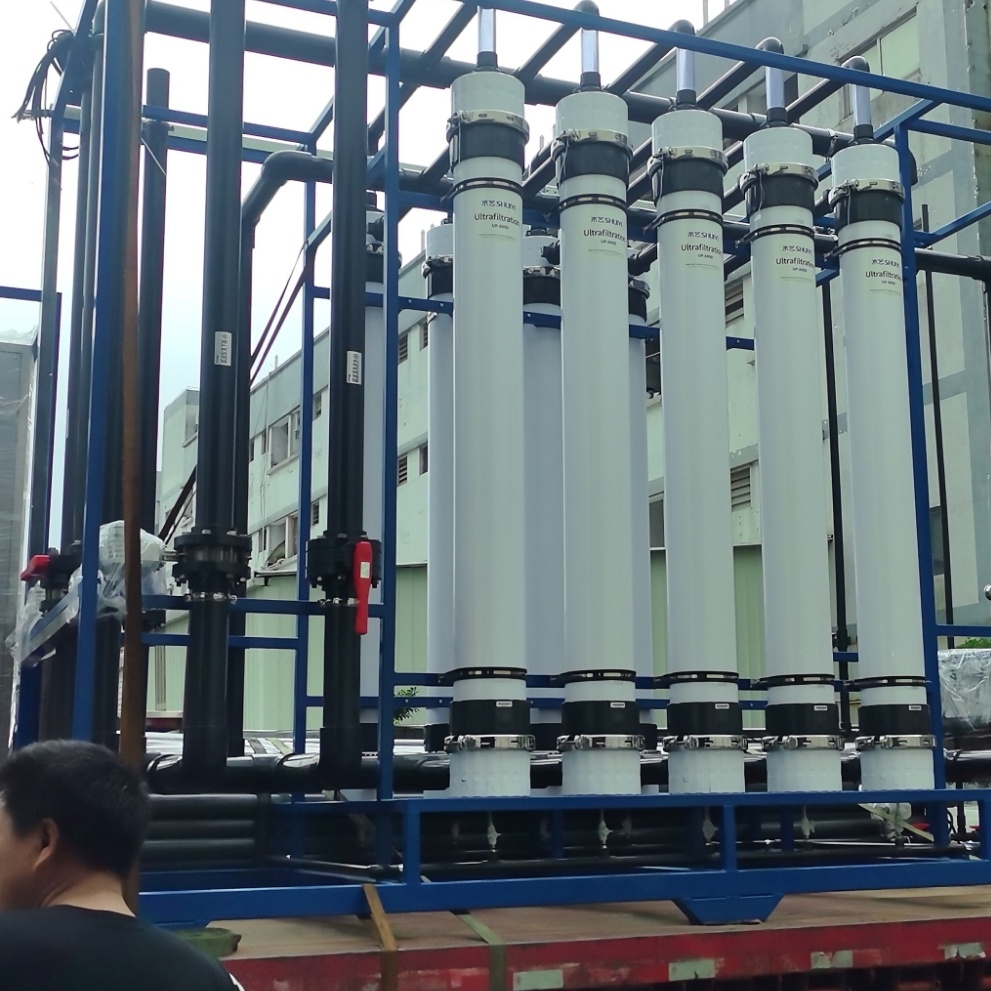
To address these challenges, Benenv designed a 50 m³/h advanced industrial water reclamation system based on proven UF + RO double-membrane technology, providing reliable, high-quality reclaimed water for continuous industrial reuse.
Wastewater is first collected in an equalization tank where flow rate and water quality fluctuations are balanced, ensuring consistent operating conditions for downstream treatment units.
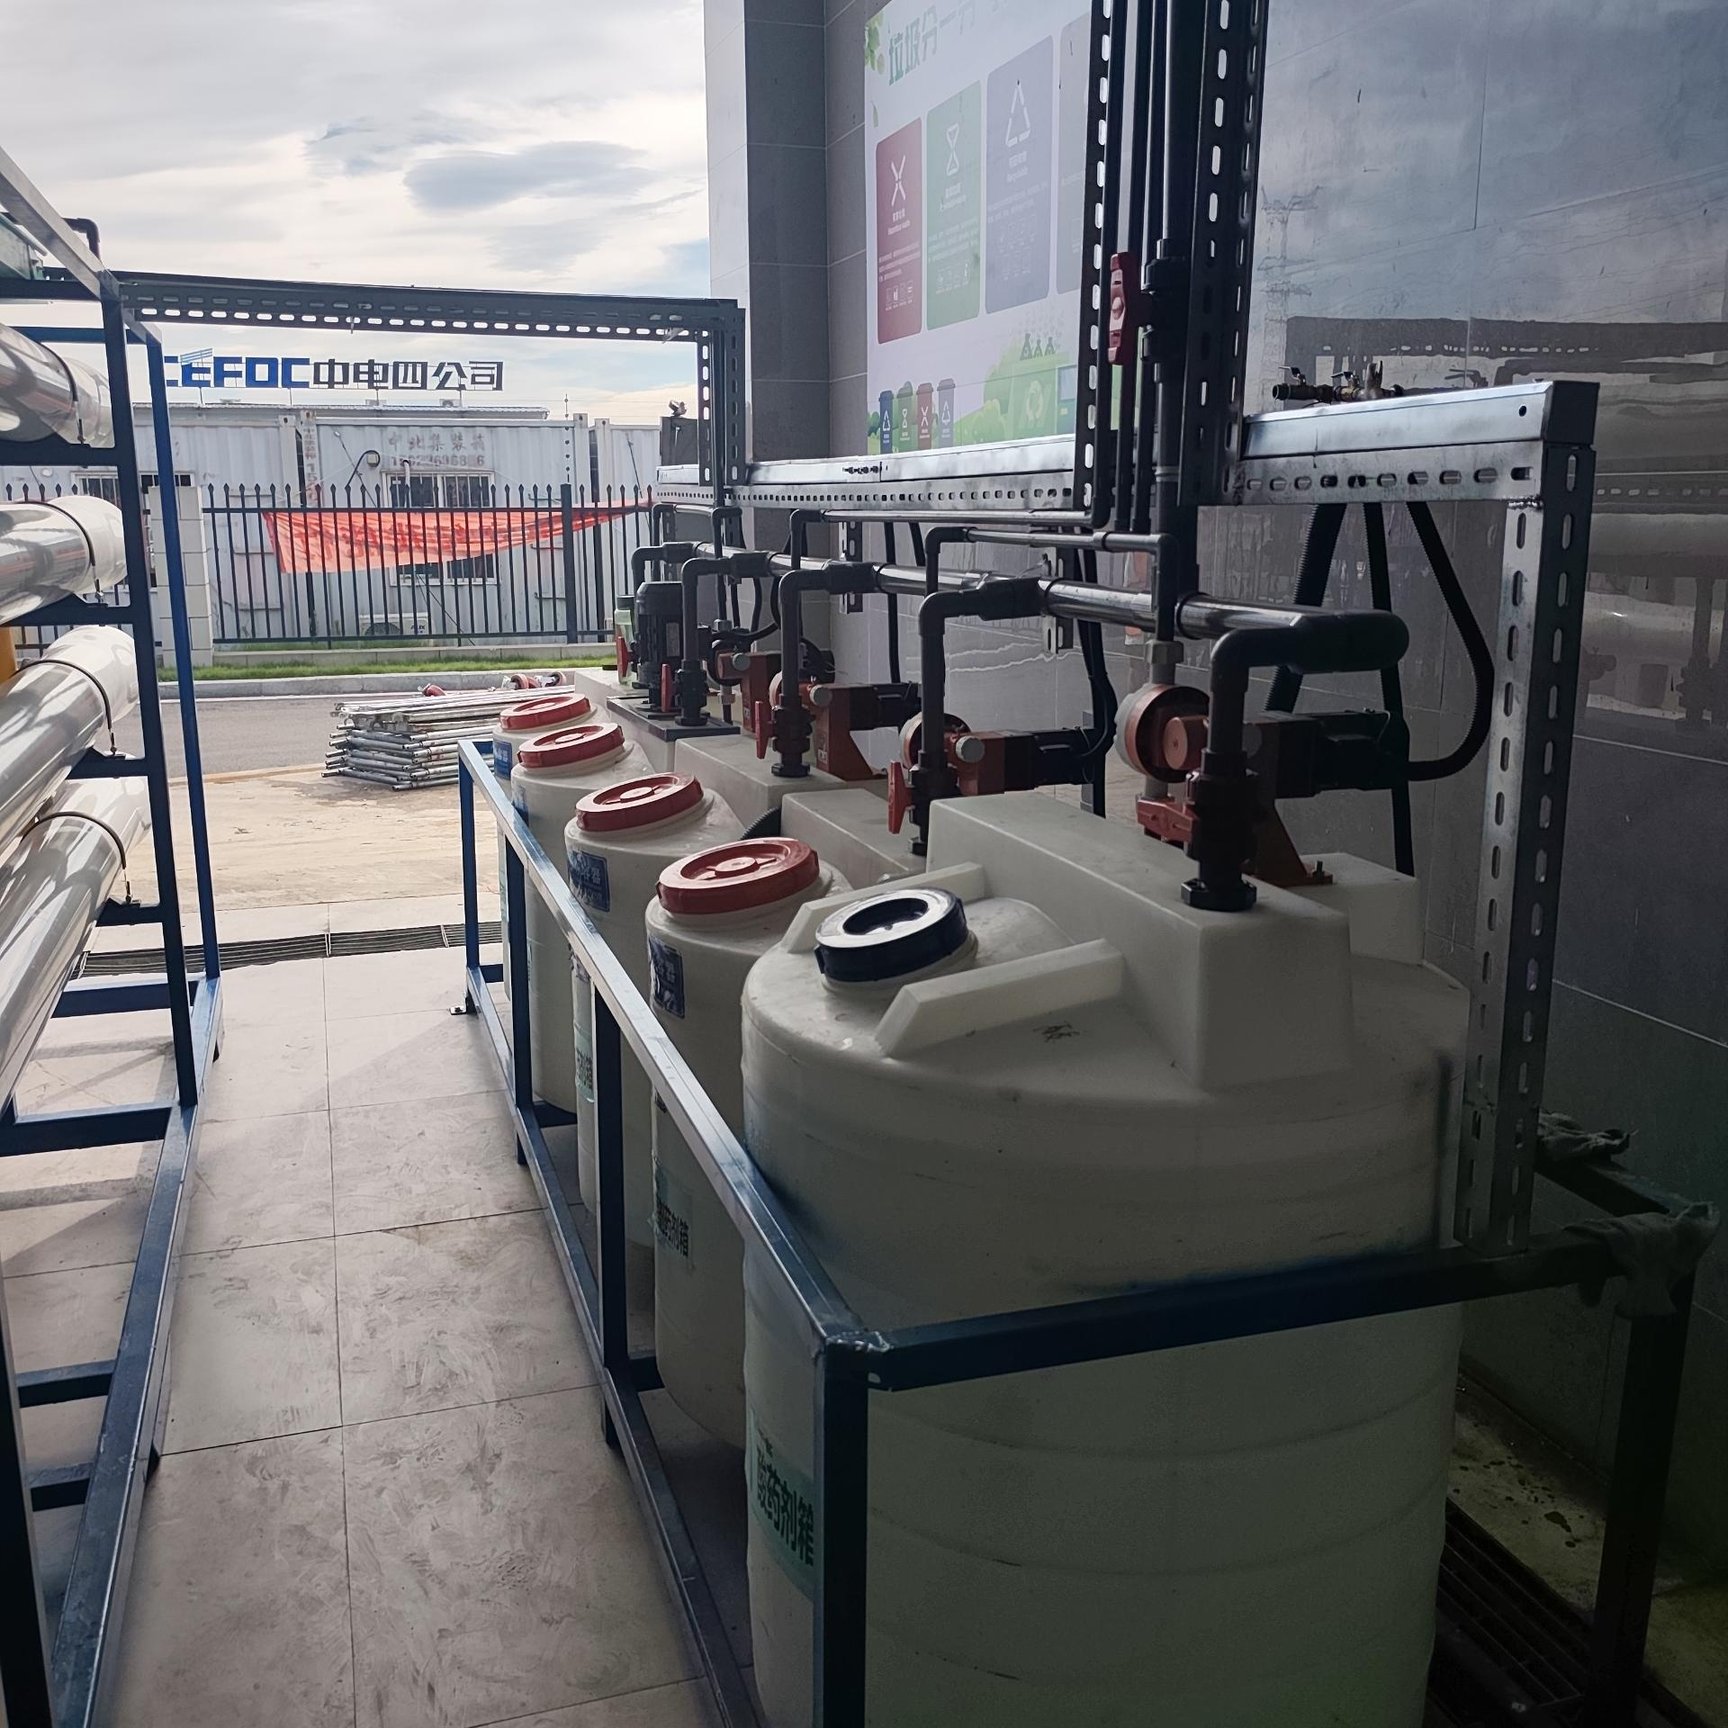
The water then undergoes coagulation and filtration pretreatment, removing suspended solids, colloidal particles, and portions of the organic contaminants. This significantly reduces the loading on the membrane systems while protecting UF and RO membranes from fouling and extending their service life.
Following pretreatment, the wastewater enters the ultrafiltration (UF) unit, where fine suspended particles and high-molecular-weight contaminants are removed to produce clarified feed water.
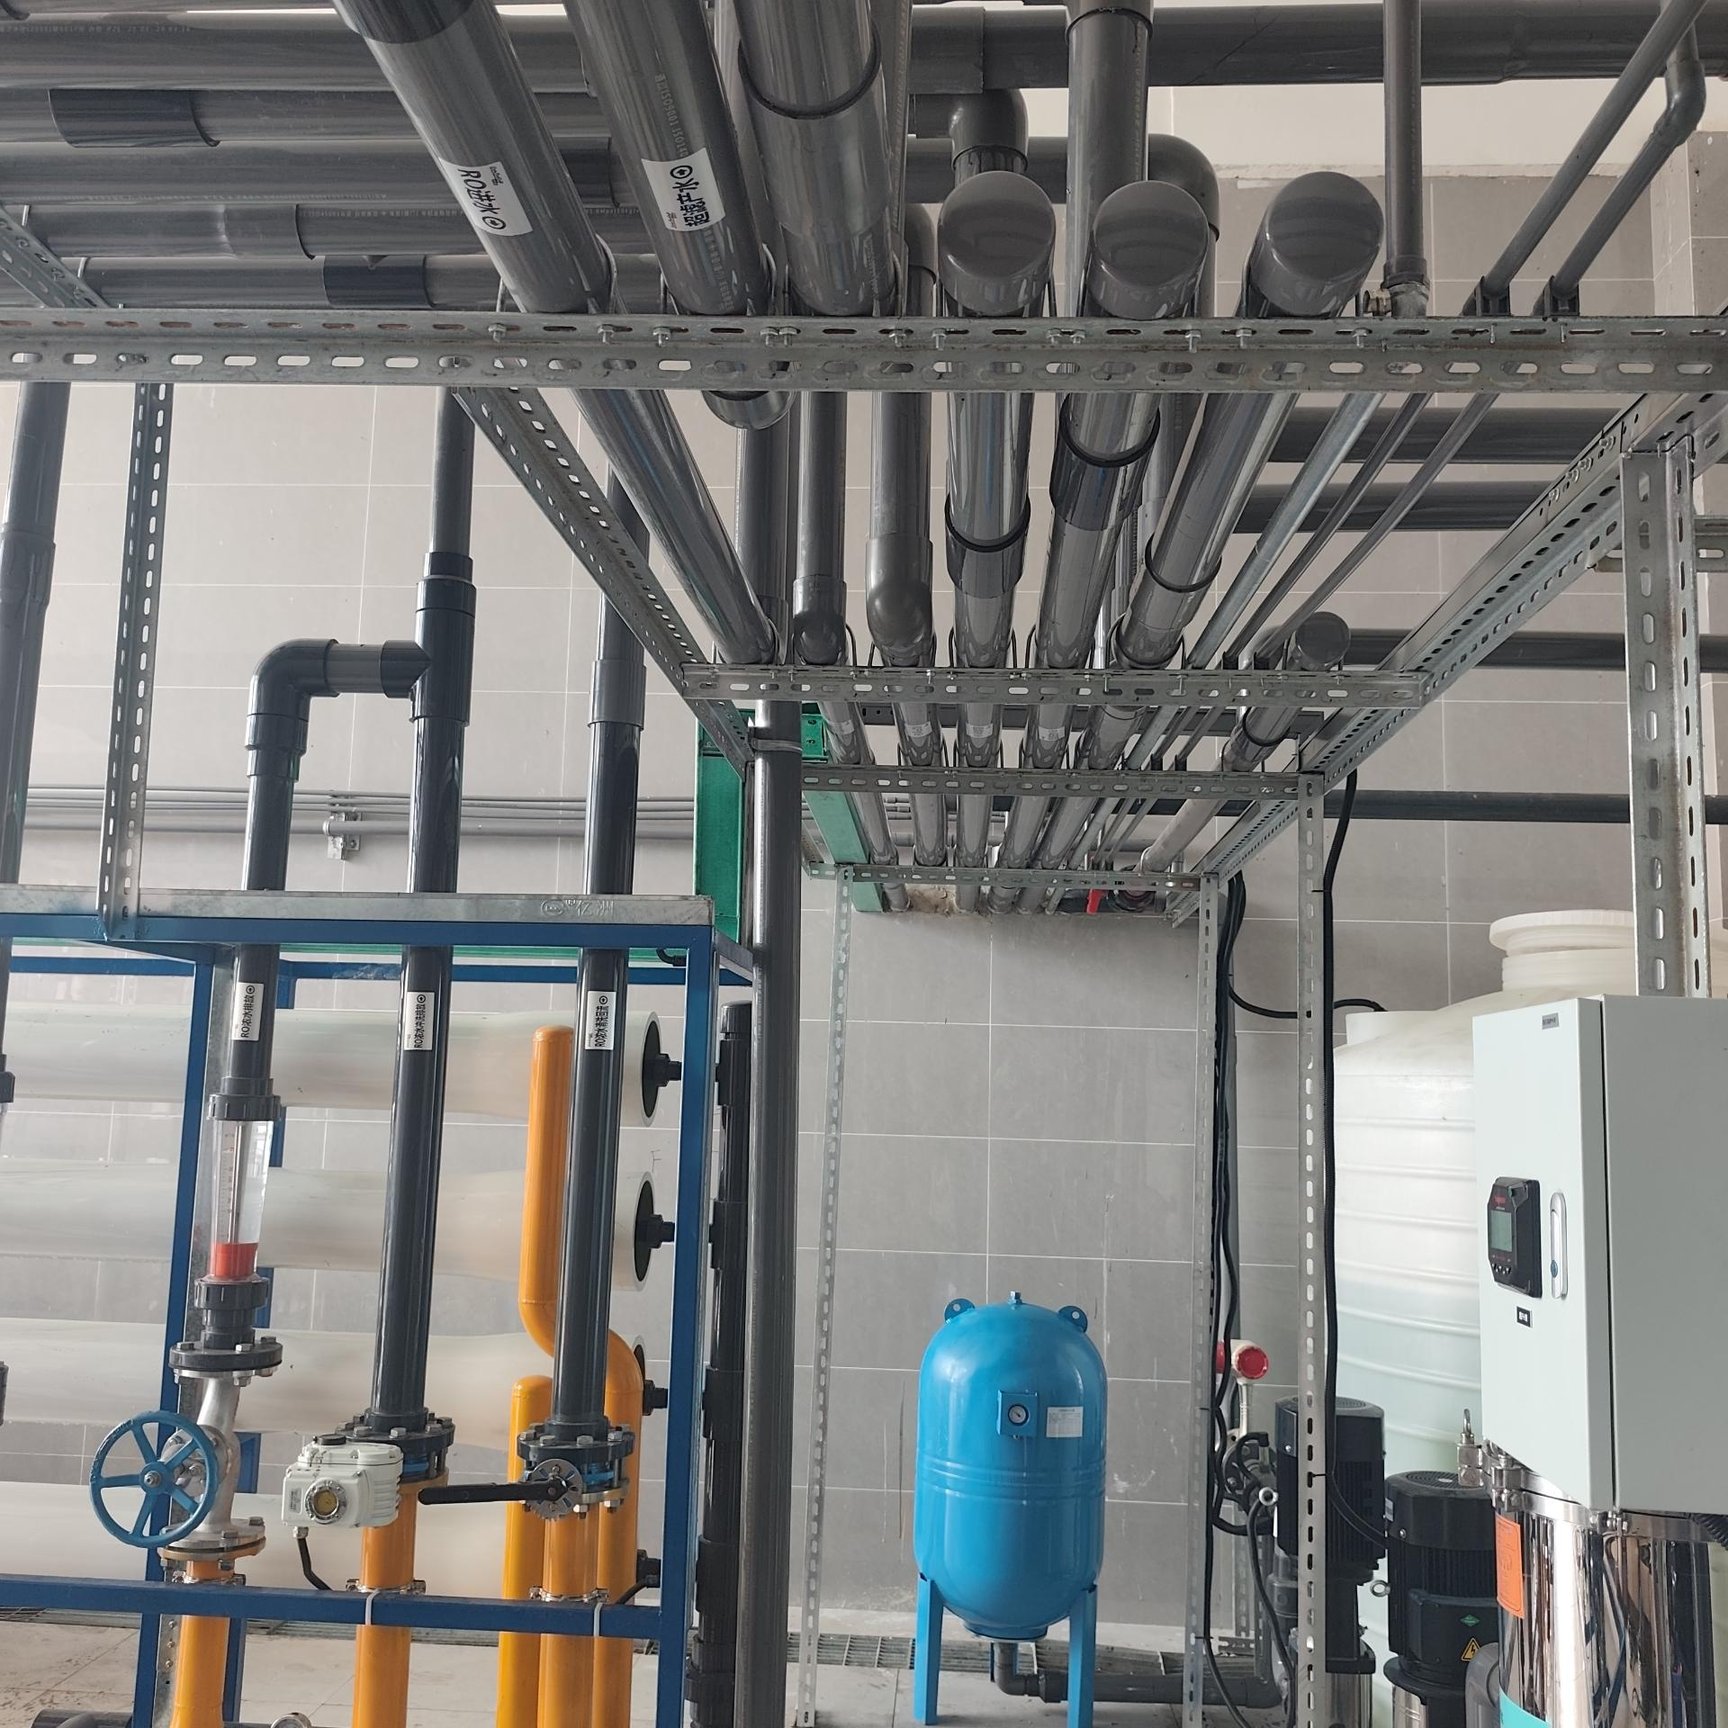
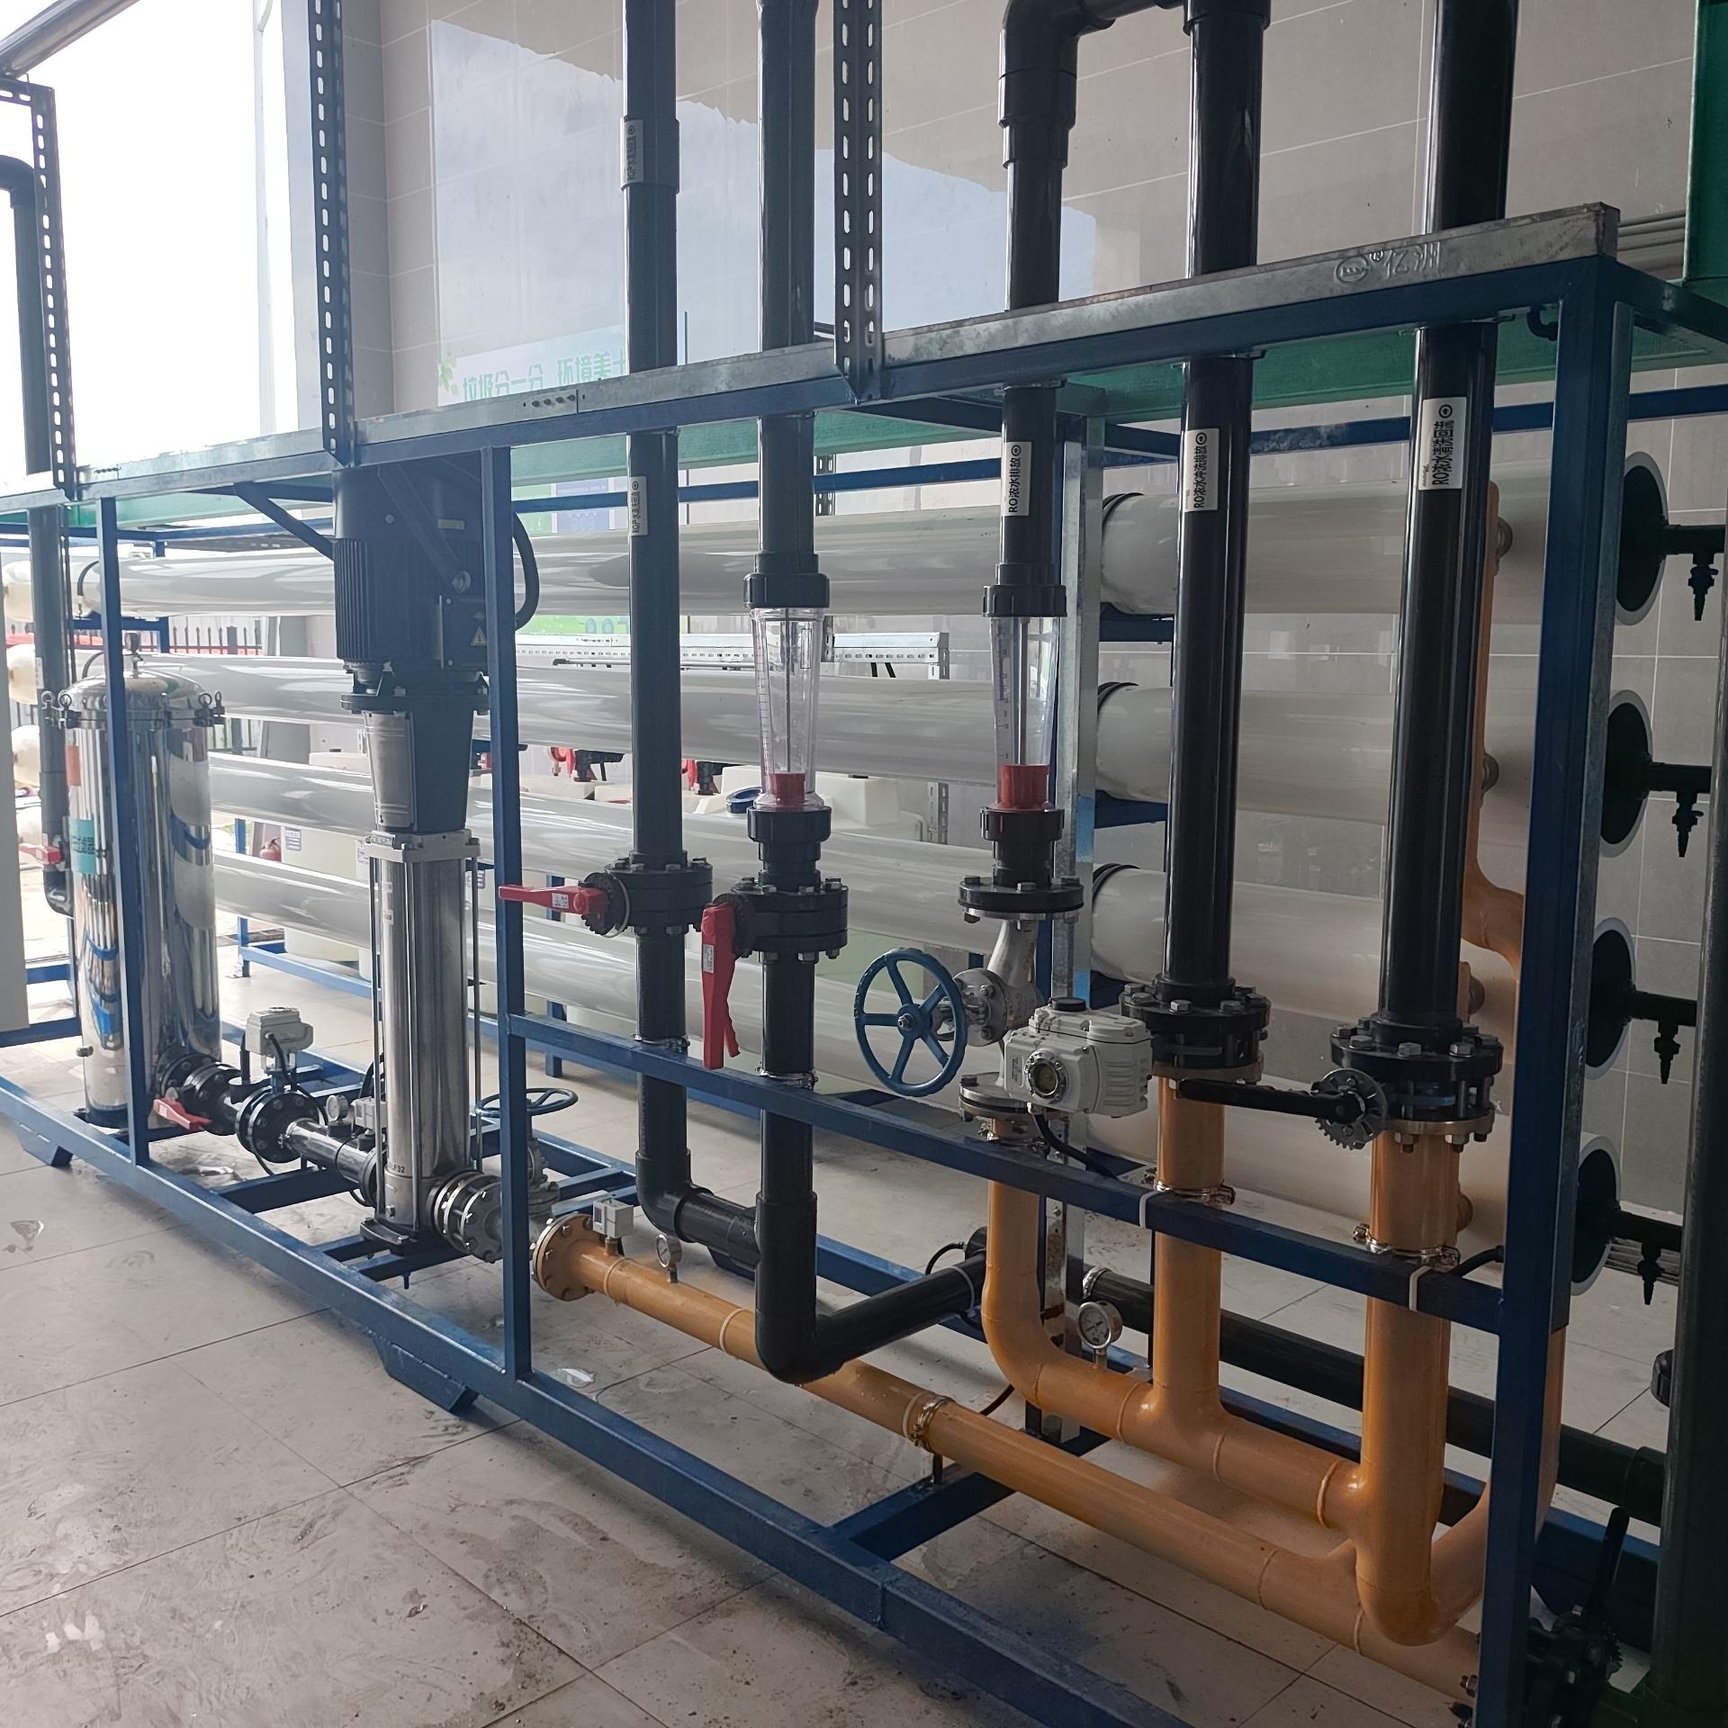
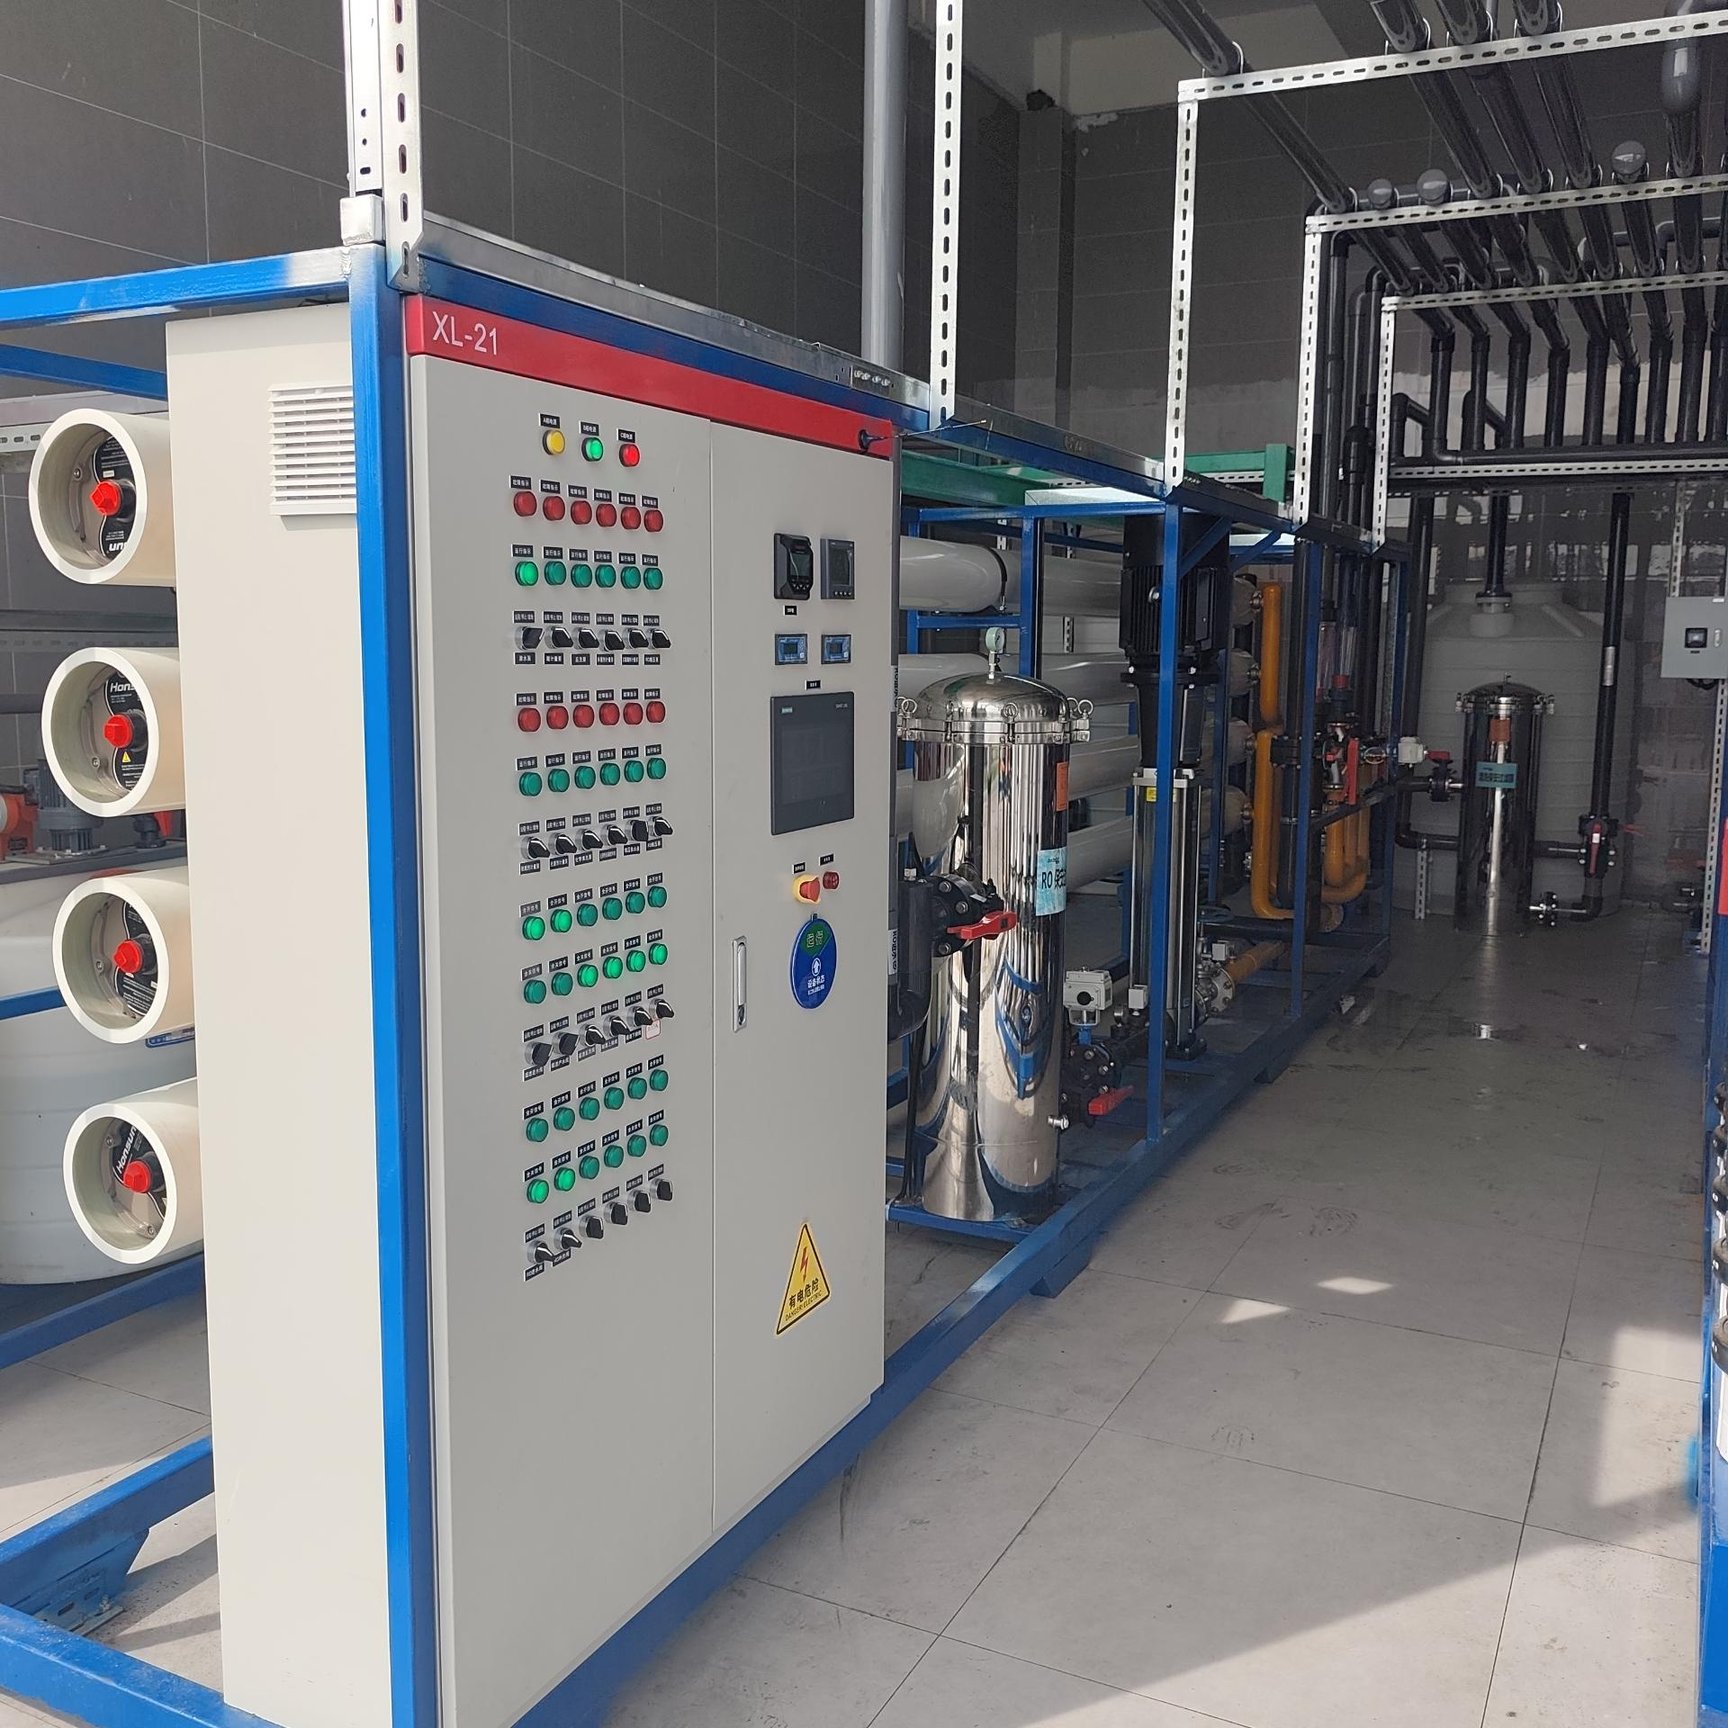
The UF permeate is subsequently treated by the reverse osmosis (RO) system, which efficiently removes dissolved salts, ions, and remaining impurities. This substantially reduces conductivity and improves overall water quality.
Finally, the reclaimed water passes through a disinfection and pressure stabilization unit before being delivered to the plant's reclaimed water distribution network.
The fully automated system operates continuously with minimal operator intervention. Intelligent PLC controls automatically regulate membrane cleaning cycles, monitor water quality, and optimize system performance, ensuring stable operation under continuous industrial production conditions.
Since commissioning, the project has successfully enabled large-scale wastewater recycling within the facility, significantly reducing freshwater consumption, lowering operating costs, and minimizing wastewater discharge volumes.
By improving water-use efficiency and supporting sustainable industrial operations, the system has helped the customer achieve environmental compliance while reducing overall production costs. Today, the project serves as a benchmark industrial water reuse application for energy facilities across Southwest China.
 |
 |
 |
 |
 |
 |

 EN