
14-t/h-two-pass-ro--edi-industrial-pure-water-system-for-energy-storage-battery-production, 14-t/h-two-pass-ro--edi-industrial-pure-water-system-for-energy-storage-battery-production, /case-studies
EN
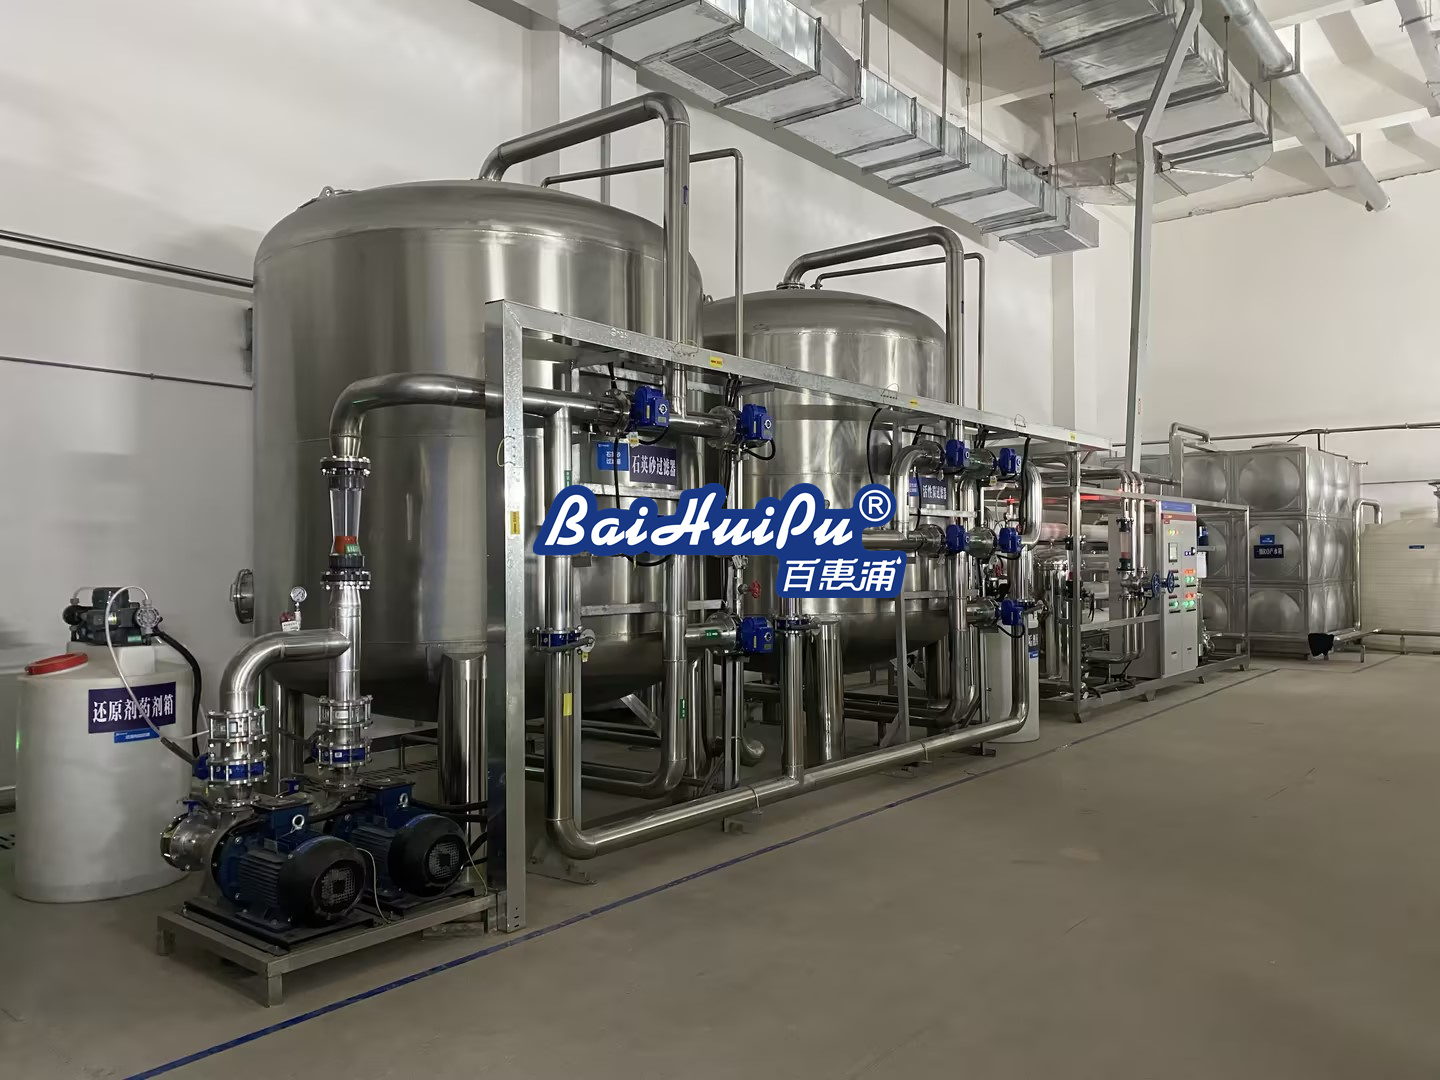
Featuring multi-stage pretreatment, two-pass reverse osmosis (RO), EDI, and precision post-treatment, this 14 T/H industrial pure water system delivers stable, high-purity process water for energy storage battery manufacturing, equipment cooling, and other critical production applications with fully automated operation.
This project provides a customized industrial pure water production system for an energy storage battery manufacturing facility. The system is designed with a production capacity of 14 m³/h (14 T/H) and supplies approximately 30 tons of industrial pure water per day, supporting both intermittent and continuous water demand throughout the production process.
The treated water consistently meets the industrial pure water requirements for the new energy and energy storage battery industry.
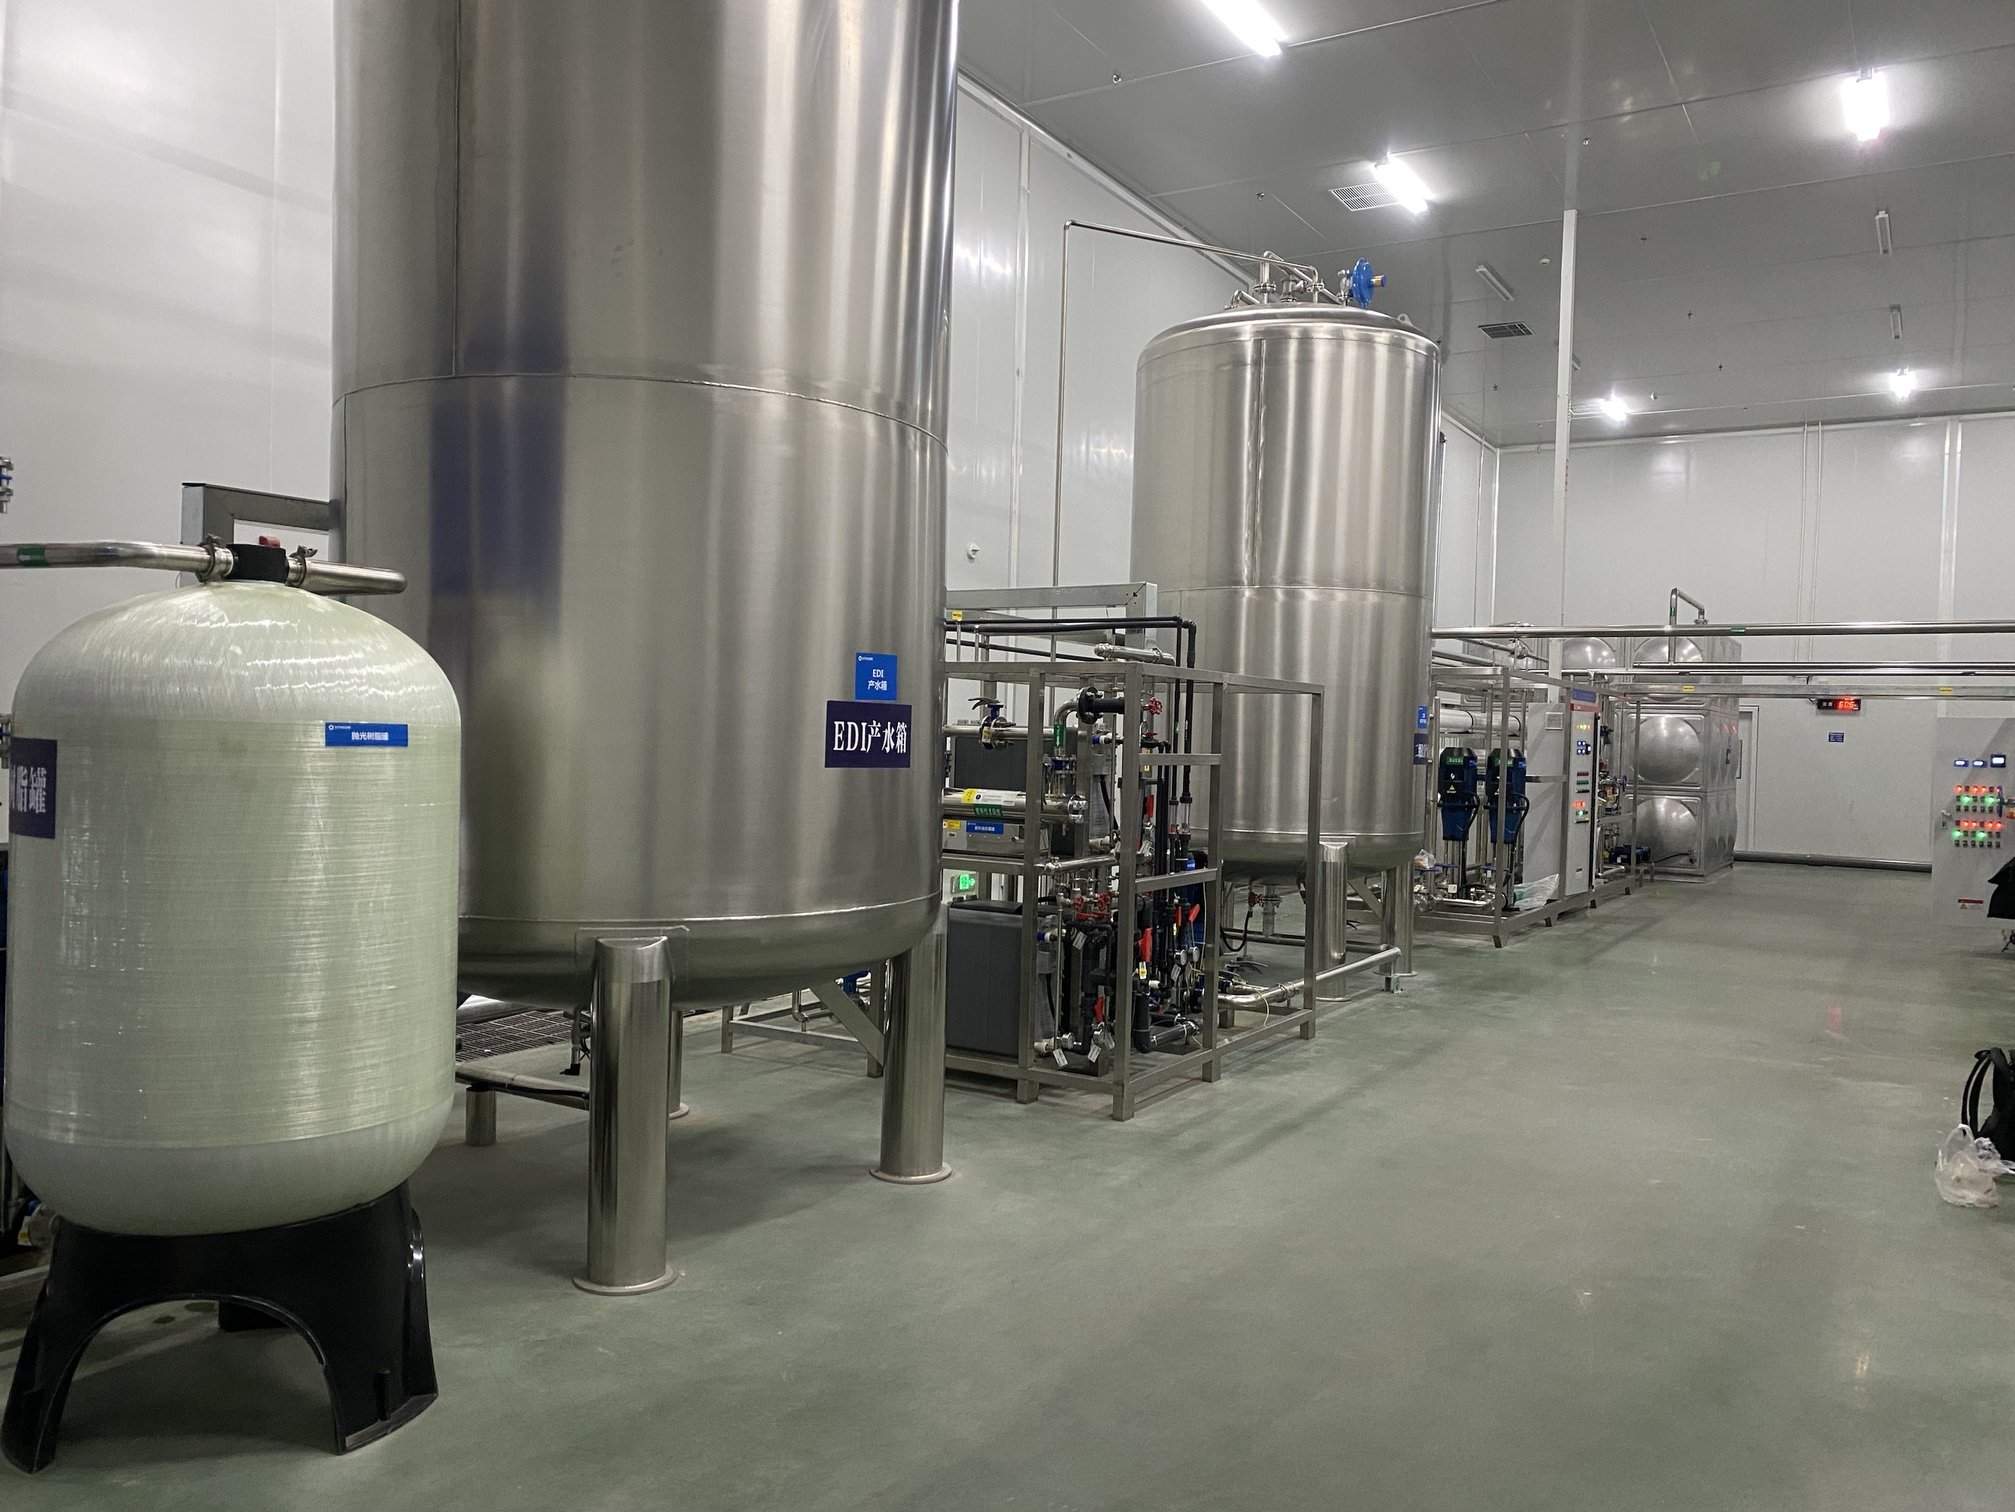
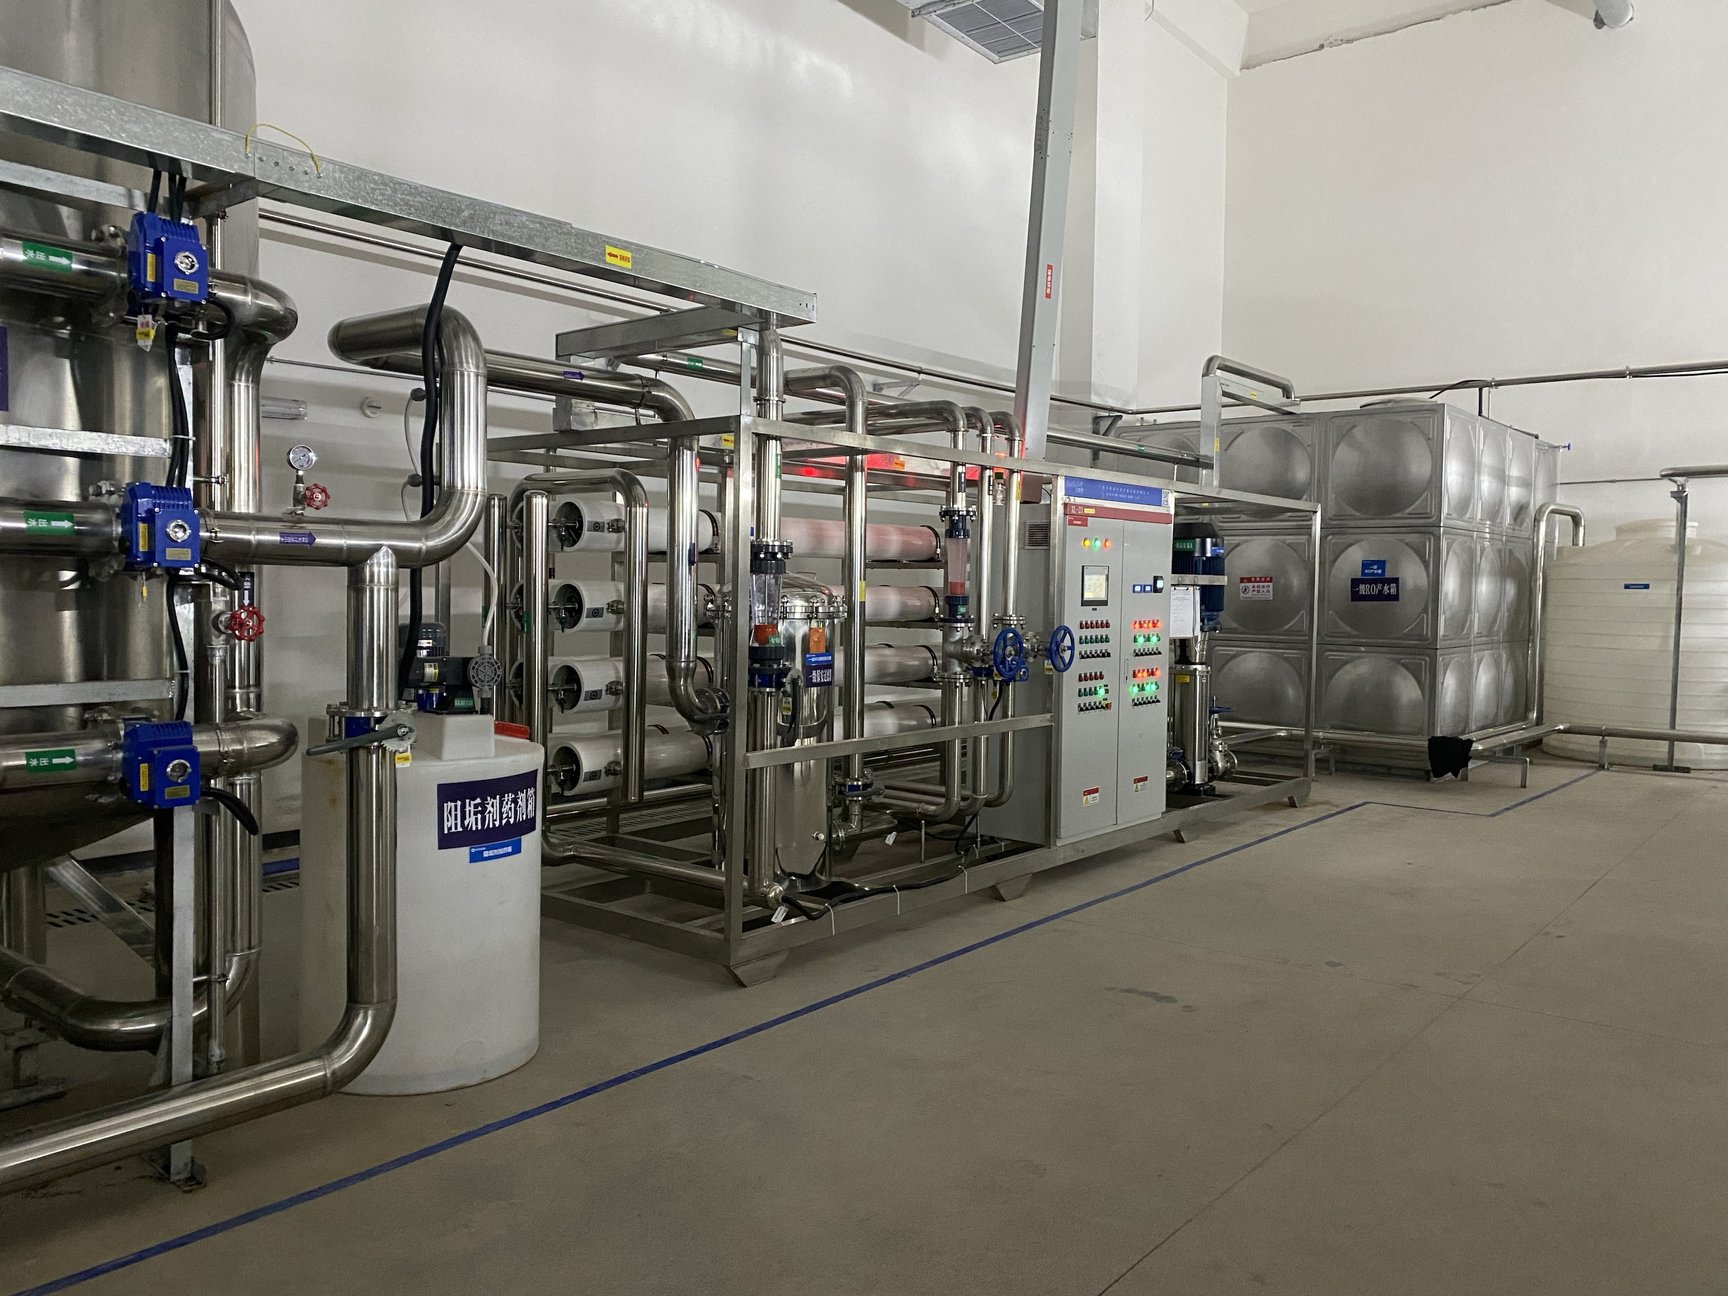
Raw Water Booster Pump → Multimedia Filtration → Activated Carbon Filtration → Precision Security Filtration → Two-Pass Reverse Osmosis (RO) → EDI (Electrodeionization) → Precision Post-Polishing → Constant-Pressure Pure Water Storage → Point-of-Use Water Supply
As the global energy storage industry continues to expand rapidly, manufacturers require increasingly higher standards of process water purity, stability, and production reliability. Untreated municipal water contains hardness minerals, dissolved salts, residual chlorine, and trace contaminants that can negatively affect critical manufacturing processes such as electrode cleaning, slurry preparation, and battery assembly. The use of inadequate process water may result in incomplete cleaning, coating defects, unstable battery performance, reduced cycle life, and lower production yield.
To support high-quality battery manufacturing, Baihuipu designed and supplied a dedicated industrial pure water production system tailored to the customer's manufacturing requirements.
The project features a 14 T/H industrial pure water system capable of supplying approximately 30 tons of high-purity water per day, fully supporting production operations, equipment cooling, laboratory testing, and other plant utility requirements.
The treatment process adopts a multi-stage purification design to ensure consistent water quality throughout the production cycle.
Raw water first enters the booster pumping system before passing through multimedia filtration and activated carbon filtration, where suspended solids, organic contaminants, residual chlorine, and other impurities are effectively removed. This pretreatment stage protects downstream membrane equipment from fouling and scaling while improving overall system efficiency.
The pretreated water then flows through a precision security filter, removing fine suspended particles before entering the core two-pass reverse osmosis (RO) system. High-performance RO membranes efficiently remove dissolved salts, hardness minerals, heavy metal ions, colloidal particles, and other dissolved impurities.
Following RO treatment, the water enters the EDI (Electrodeionization) unit, which continuously removes remaining ionic contaminants through electrically driven ion exchange technology. A precision polishing stage further stabilizes water quality, ensuring that the final product water consistently meets the stringent purity requirements of energy storage battery manufacturing.
The complete system is controlled by a PLC-based intelligent automation platform, enabling fully automatic 24-hour operation. Functions include automatic membrane flushing, pressure regulation, constant-pressure water supply, intelligent load adjustment based on plant demand, low-water protection, and overload shutdown. These features effectively reduce membrane fouling, extend equipment service life, and minimize operating costs without requiring continuous operator supervision.
Since commissioning, the system has consistently delivered stable flow rates and high-quality industrial pure water, fully supporting every stage of energy storage battery production. The reliable water supply has eliminated production risks associated with poor raw water quality, improved battery consistency and product yield, and provided a solid foundation for standardized, large-scale, high-quality manufacturing.
This project represents another successful reference for Baihuipu in supplying advanced industrial pure water systems to the global new energy and energy storage battery industry, demonstrating the company's expertise in delivering reliable, energy-efficient, and fully automated water treatment solutions.

 EN