
11-t/h-industrial-pure-water-system--guangzhou-battery-plant-project, 11-t/h-industrial-pure-water-system--guangzhou-battery-plant-project, /case-studies
EN
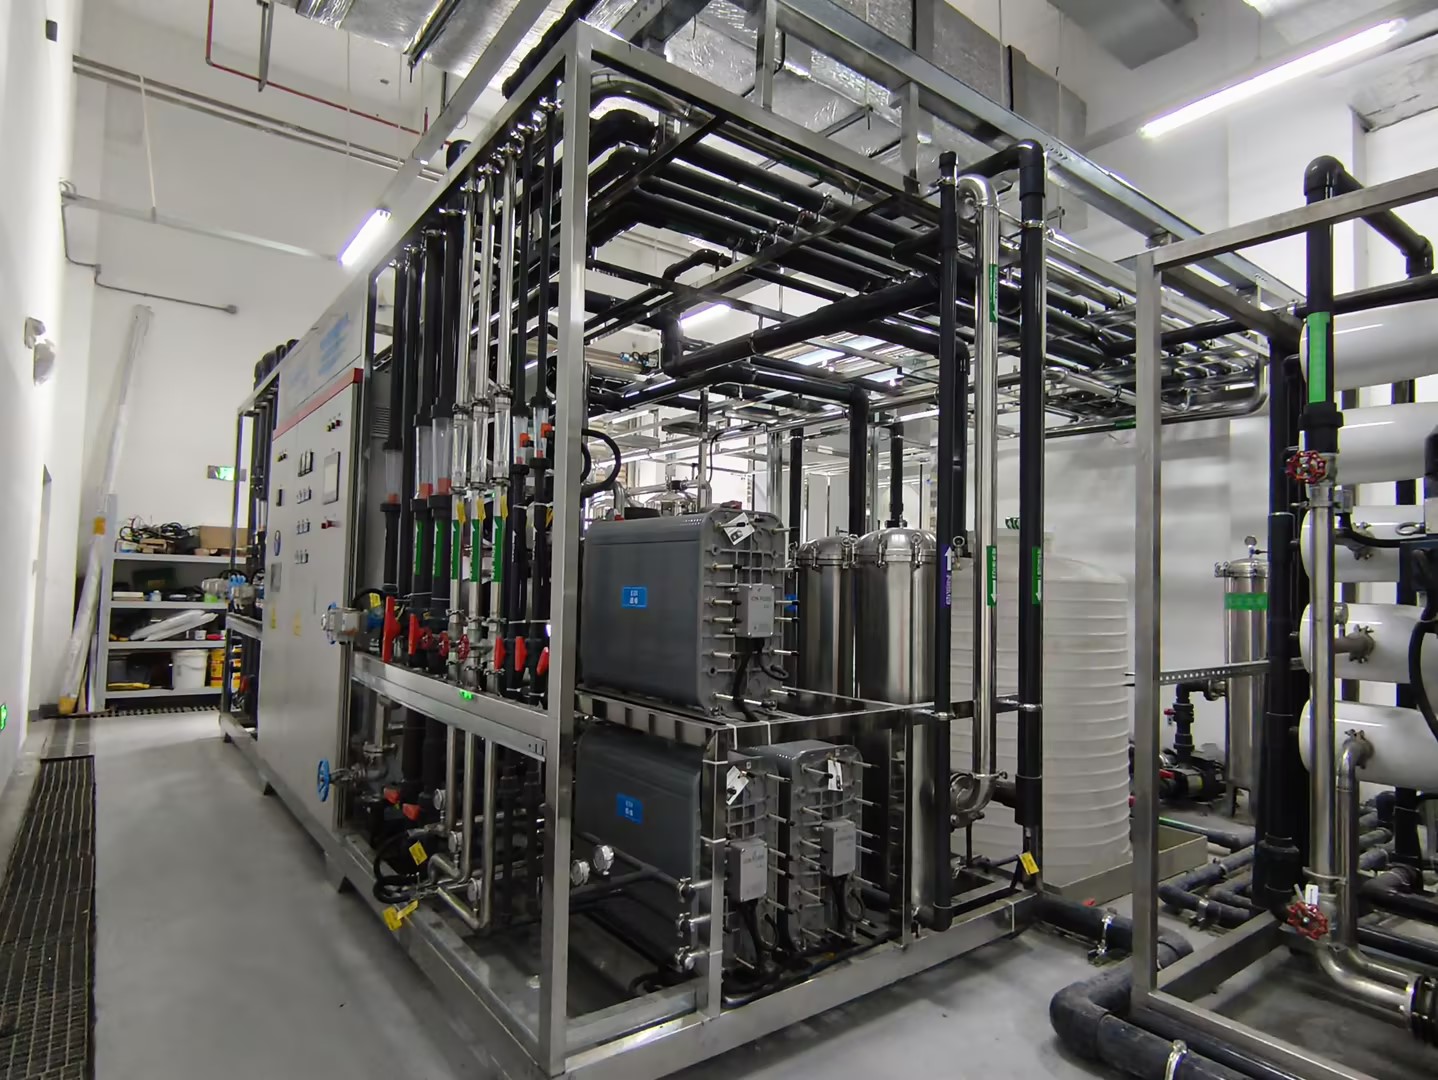
An industrial pure water system featuring multimedia pretreatment, activated carbon filtration, double-pass reverse osmosis (RO), and precision filtration, delivering stable, automated, and continuous pure water supply for lithium battery manufacturing.
This project was implemented for Guangzhou Ronbay Energy Technology Co., Ltd., providing a customized industrial pure water production system for its lithium battery manufacturing facility.
The system is designed to produce 11 m³/h of industrial pure water and supports 24-hour continuous operation, meeting the large-volume water demand of modern battery production lines. The product water complies with industrial pure water standards for the lithium battery industry.
Raw Water Booster Pump → Multimedia Filter → Activated Carbon Filter → Precision Cartridge Filter → Double-Pass Reverse Osmosis (RO) → Pure Water Storage & Constant-Pressure Distribution
The system continuously supplies high-quality process water for battery slurry preparation, electrode cleaning, equipment cooling, and other critical manufacturing processes.
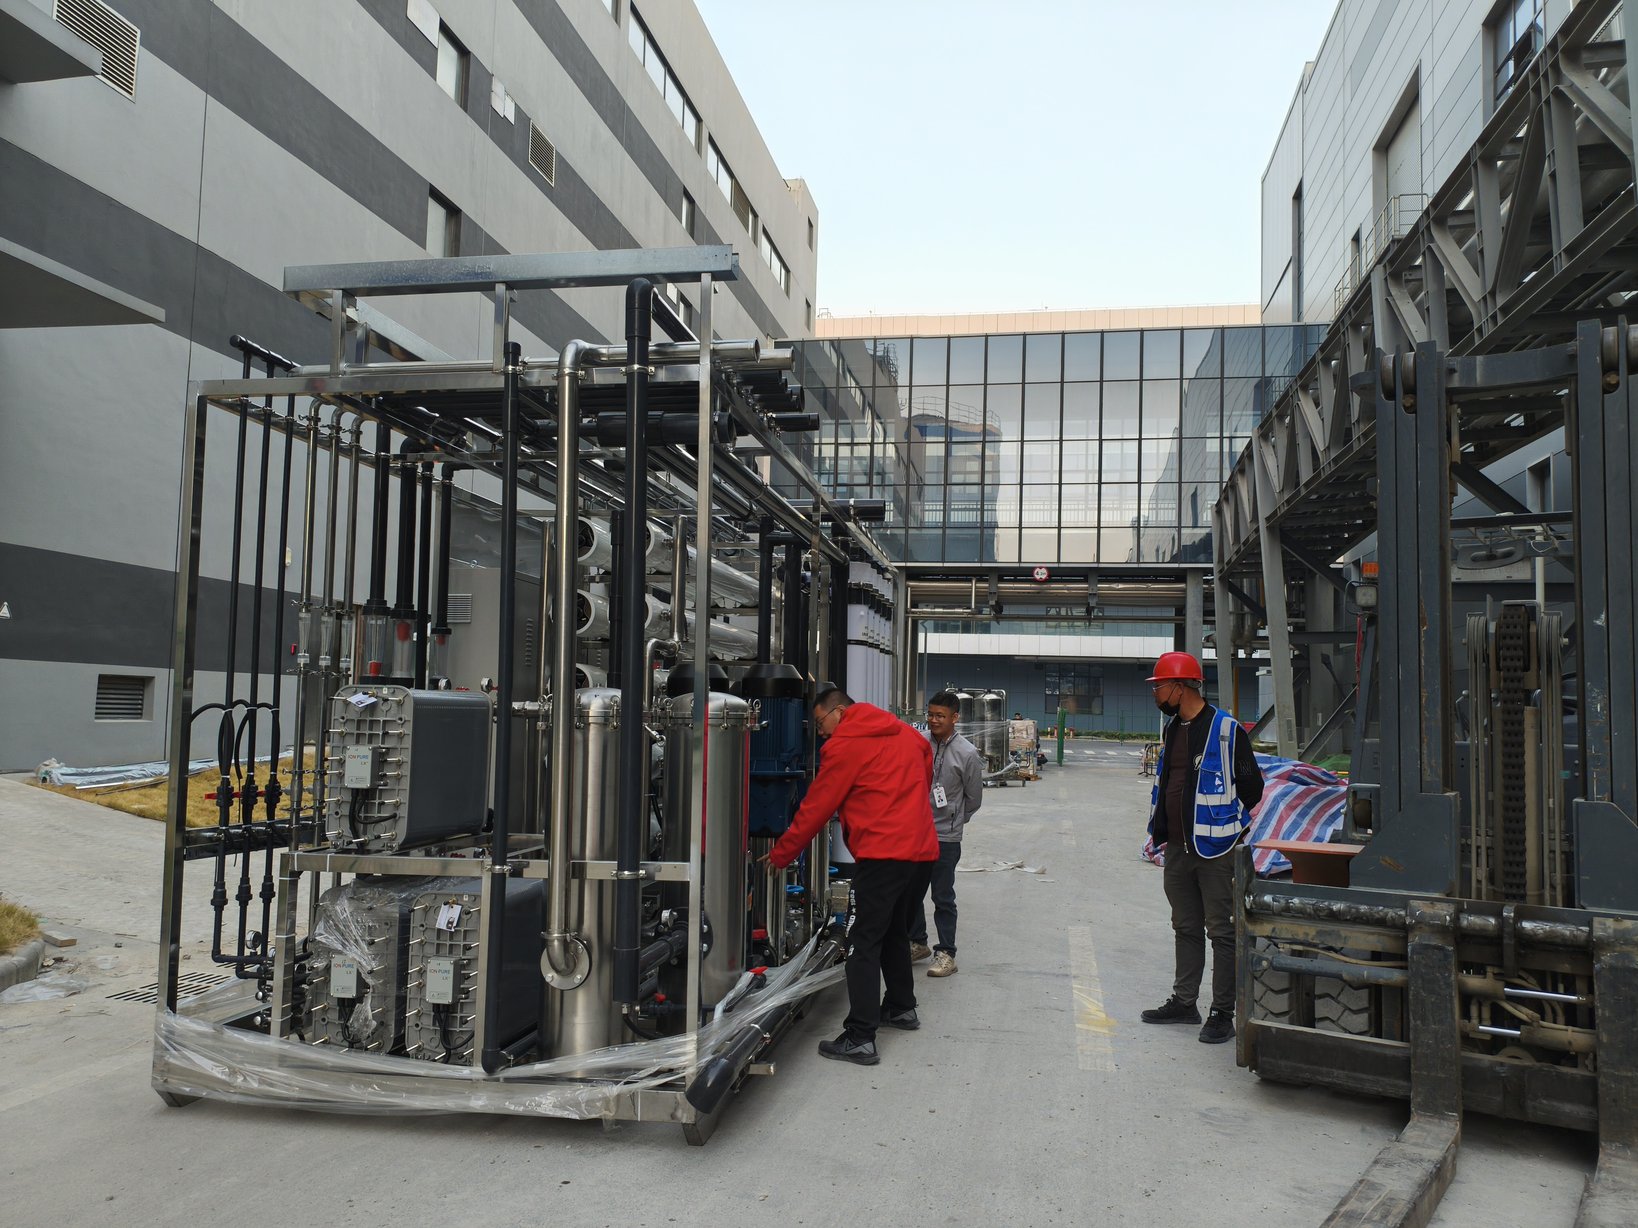
This industrial pure water system is suitable for manufacturers of:
Typical applications include:
Battery manufacturing requires extremely low concentrations of dissolved salts and impurities. Conventional municipal water may contain excessive minerals and suspended contaminants, which can negatively affect electrode cleanliness, coating quality, battery consistency, and production yield.
The system is ideal for:
It provides a standardized and reliable pure water solution for modern lithium battery manufacturing.
Guangzhou Ronbay Energy specializes in the research, development, and manufacturing of advanced lithium batteries. Throughout the battery production process, high-quality process water is essential to maintain product consistency and manufacturing reliability.
The local municipal water supply contains hardness minerals, dissolved salts, residual chlorine, and trace impurities. If used directly for electrode cleaning or slurry preparation, these contaminants may lead to surface contamination, uneven coating quality, reduced electrical conductivity, lower battery consistency, and decreased production yield.
To support standardized, large-scale manufacturing, Baihuipu designed a high-capacity industrial pure water production system capable of delivering stable, high-quality process water around the clock.
Based on the customer's requirement for 11 m³/h continuous production, uninterrupted process water supply, and the characteristics of Guangzhou's local water source, Baihuipu developed a multi-stage purification system centered on advanced pretreatment and double-pass reverse osmosis technology.
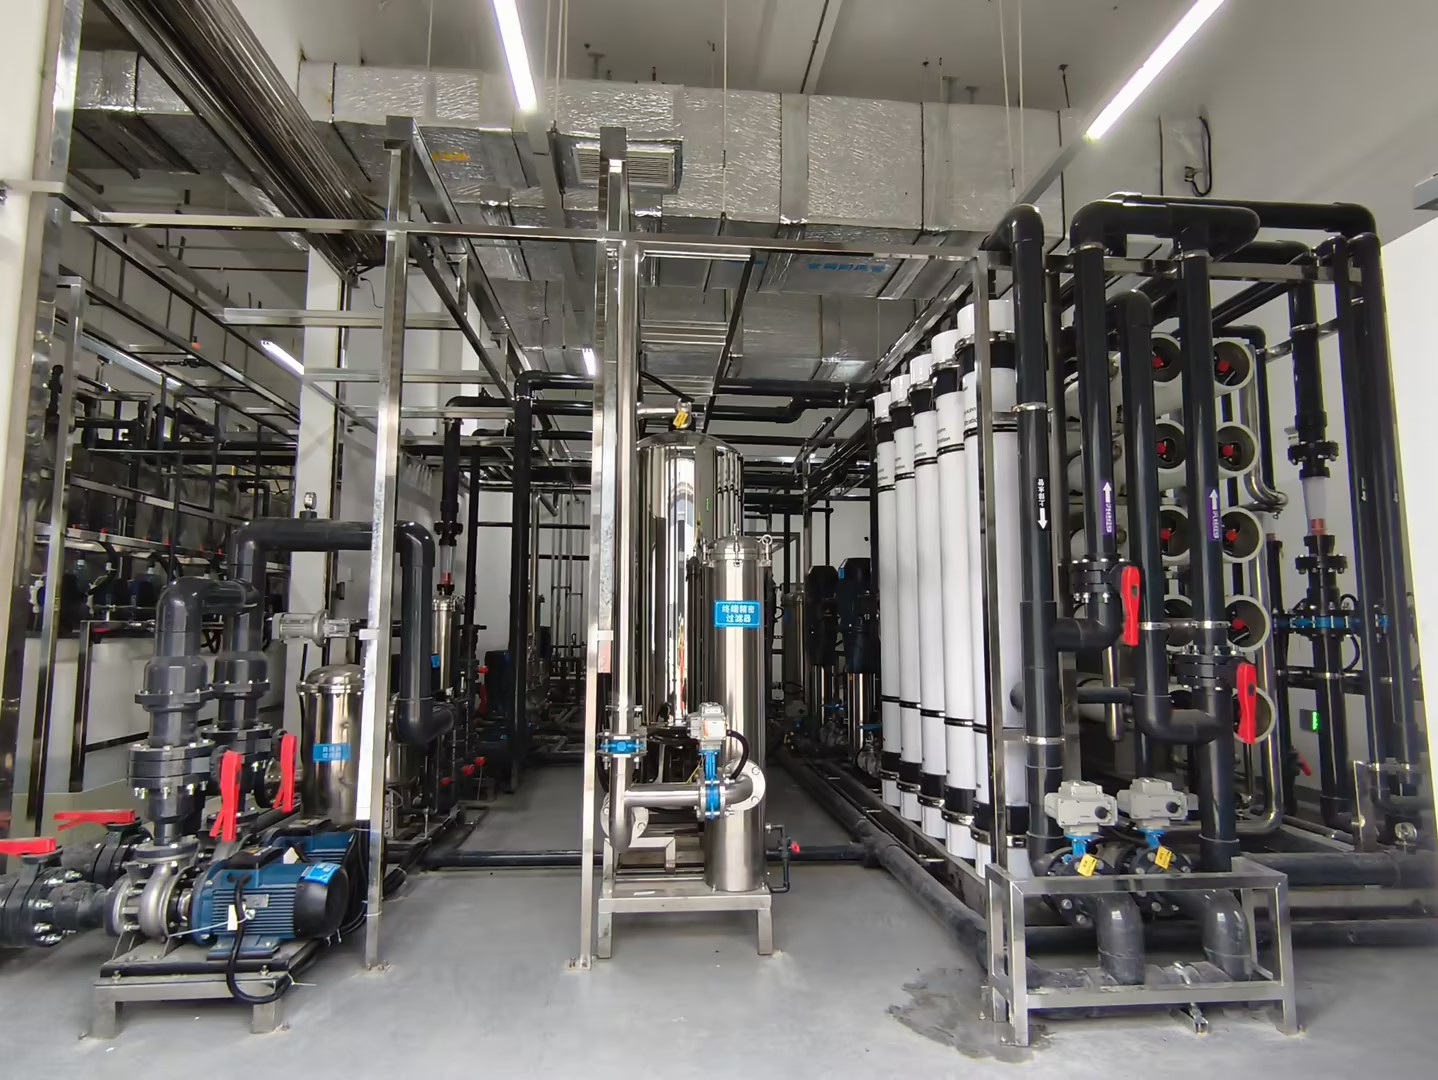
Raw water is first pressurized before entering the pretreatment section. A multimedia filter removes suspended solids, sediment, and larger particulate matter. The water then passes through an activated carbon filter, which effectively removes residual chlorine, odors, color, and dissolved organic compounds while protecting downstream membrane components.
Following pretreatment, the water enters a precision cartridge filter, which captures fine particles and prevents membrane fouling.
The pretreated water is then processed through the double-pass reverse osmosis system, the core purification stage of the project. The RO membranes efficiently remove dissolved salts, metal ions, organic contaminants, colloids, and other microscopic impurities, producing industrial pure water that fully satisfies the stringent water quality requirements of lithium battery manufacturing.
The entire system operates under a fully automated PLC control platform capable of automatic start-stop operation, scheduled membrane flushing, constant-pressure water delivery, and intelligent operational management. These features effectively minimize membrane scaling, extend equipment service life, and significantly reduce maintenance requirements.
Since commissioning, the system has consistently delivered sufficient water production capacity, stable water quality, and highly reliable automated operation without requiring continuous operator supervision.
The project now provides a continuous supply of high-quality industrial pure water for every stage of battery manufacturing, including electrode cleaning, slurry preparation, equipment cooling, and other critical production processes. By eliminating water-quality-related production risks, the system has improved battery product quality, increased manufacturing yield, reduced equipment maintenance costs, and provided Guangzhou Ronbay Energy with a dependable and efficient water supply solution.
This successful installation serves as an excellent reference project for industrial pure water systems supporting large-scale lithium battery manufacturing and demonstrates Baihuipu's expertise in delivering reliable, energy-efficient, and fully automated water treatment solutions for the global new energy industry.

 EN